E-mail us: [email protected]
Tel: +86-15239857375
 English
 中文简体


 Home / Author / Gao Manli — Overseas Sales Manager / Self-Lubricating Tin Bronze Flanged Bushings for Reliable Pump and Industrial Motion Systems
Self-Lubricating Tin Bronze Flanged Bushings for Reliable Pump and Industrial Motion Systems
 2026.10.30
 Gao Manli — Overseas Sales Manager
Content
- 1 What Is a Self-Lubricating Tin Bronze Flanged Bushing?
- 2 Why Tin Bronze Is Suitable for Self-Lubricating Bushings
- 3 Operating Principle of the Oil-Impregnated Structure
- 4 Key Advantages Over Conventional Bushings
- 5 Technical Characteristics and Reference Values
- 6 Powder Metallurgy Manufacturing Process
- 7 Quality Control and Manufacturing Strengths
- 8 Applications in Pump Systems
- 9 Applications Beyond Pumps
- 10 Comparison with Other Bearing Solutions
- 11 Design Considerations for Engineers
- 12 Installation Recommendations
- 13 Maintenance and Service-Life Management
- 14 Customization Options
- 15 Production, Packaging, and Delivery
- 16 Why Choose an Experienced Powder Metallurgy Manufacturer?
- 17 How the Product Supports Pump Reliability
- 18 Frequently Asked Questions
- 18.1 What is the main benefit of a self-lubricating flanged bronze bushing?
- 18.2 Can this bushing be used in water pumps?
- 18.3 What materials are available?
- 18.4 What dimensions can be customized?
- 18.5 Does the bushing require additional grease?
- 18.6 How does the flange improve installation?
- 18.7 What is the expected service life?
- 18.8 Can the product be used for oscillating motion?
- 18.9 What surface treatments are available?
- 18.10 How is oil retained inside the bushing?
- 18.11 Can the company produce small trial batches?
- 18.12 What information should be provided for a quotation?
- 18.13 What quality documents can be provided?
- 18.14 How should a worn bushing be investigated?
- 19 Conclusion
- 20 References
- 21 Product: Powder Metallurgy Self-lubricating Tin Bronze Flanged Bushing
Self-lubricating tin bronze flanged bushings are engineered bearing components designed to support rotating or oscillating shafts while reducing friction, wear, maintenance requirements, and the risk of unexpected equipment downtime. Manufactured through powder metallurgy, these bushings contain a controlled network of internal pores that are filled with lubricating oil. During operation, the stored oil gradually migrates to the bearing surface, creating a protective film between the shaft and the bushing.
The integrated flange provides an additional functional advantage. It supports axial positioning, helps prevent the bushing from moving through its housing, and simplifies assembly. When a pump, motor, actuator, or transmission requires a compact bearing solution that can operate with limited external lubrication, a self-lubricating flanged bronze bushing can provide a dependable alternative to conventional solid bronze bushings, greased bearings, and other externally lubricated components.
Jiande Welfine Technology Co., Ltd. specializes in powder metallurgy sintering and related precision machining. With more than 20 years of industry experience, a 13,039-square-meter production base, advanced forming and sintering equipment, and ISO 9001:2015 and IATF 16949:2016 quality management certifications, the company develops customized self-lubricating bushings and precision sintered components for customers in multiple industrial sectors.
This article explains the construction, operating principle, manufacturing process, technical characteristics, application advantages, customization options, and quality controls associated with powder metallurgy self-lubricating tin bronze flanged bushings.
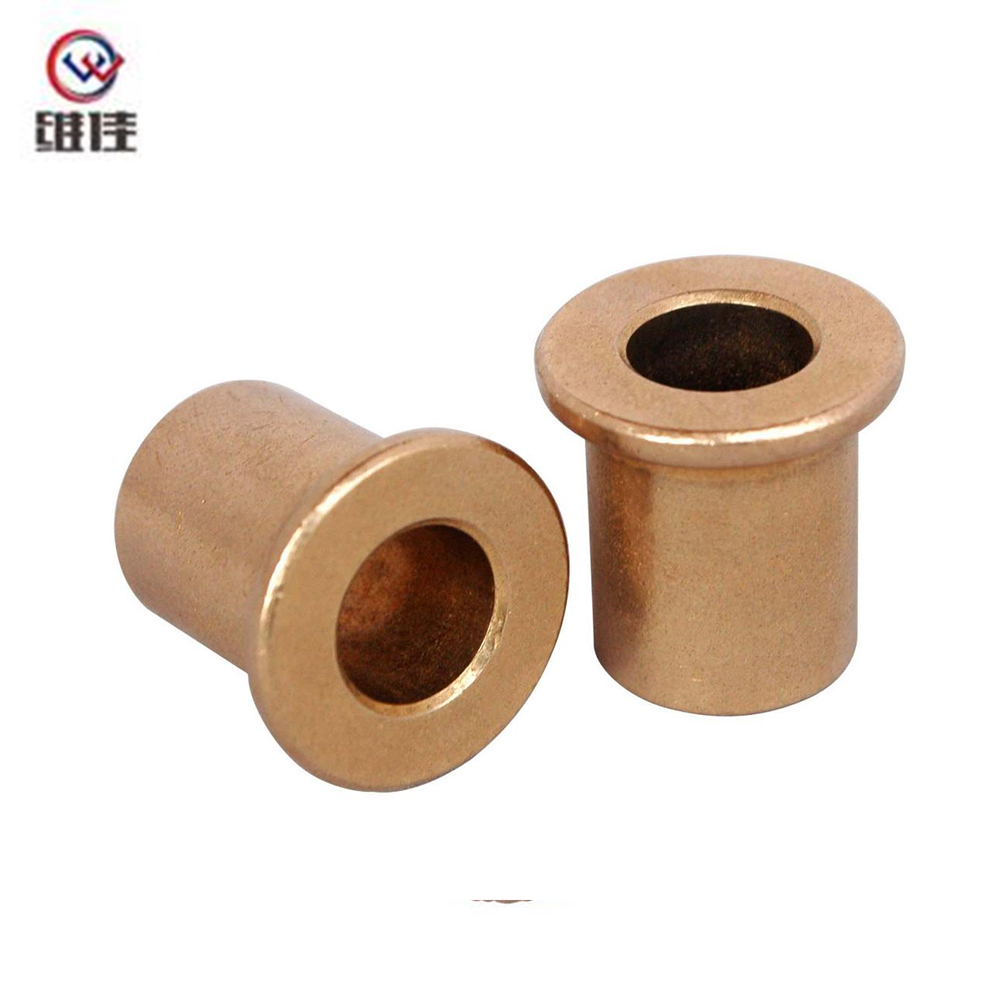
Powder Metallurgy Self-lubricating Tin Bronze Flanged Bushing
What Is a Self-Lubricating Tin Bronze Flanged Bushing?
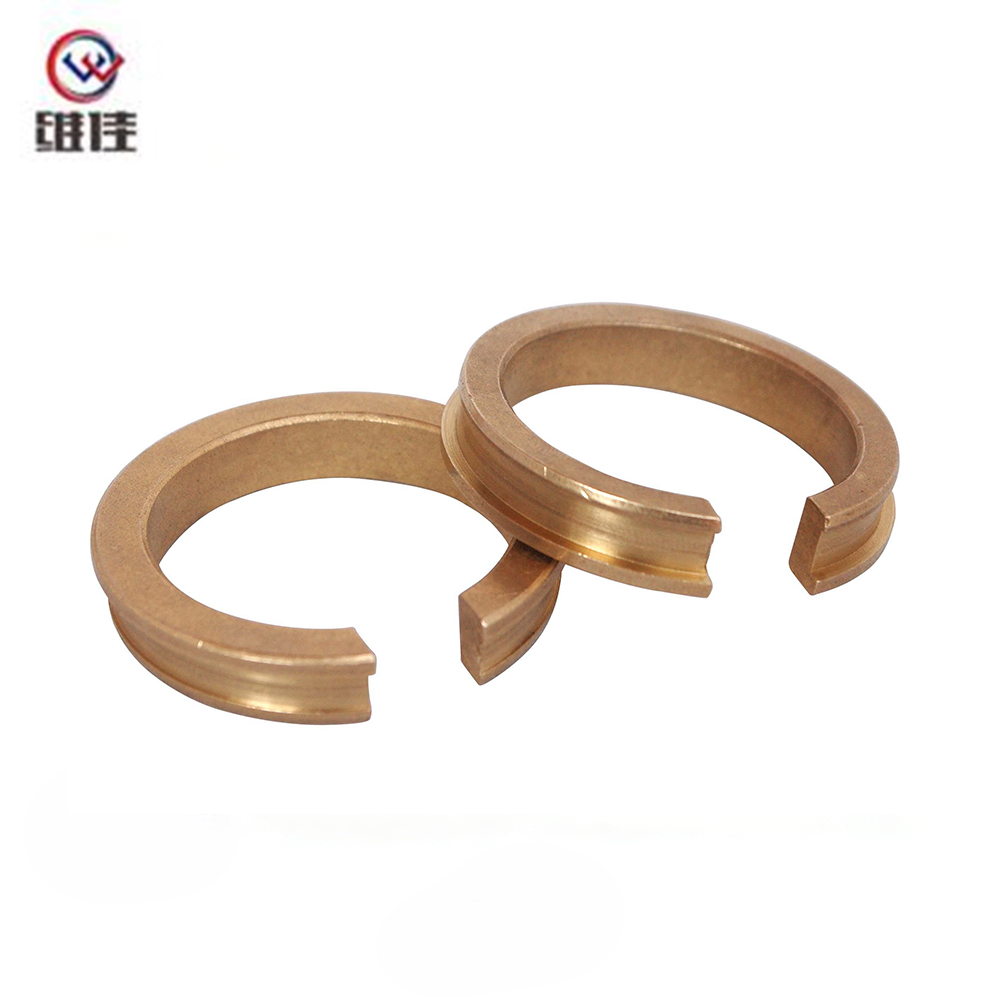
A self-lubricating tin bronze flanged bushing is a sleeve-shaped bearing made from porous tin bronze powder metallurgy material. The bushing normally includes a cylindrical bearing section and an integrated radial flange. The cylindrical section supports the shaft, while the flange provides axial location and may also carry limited axial loads depending on the design and operating conditions.
During manufacture, tin bronze powder is compacted into a predefined shape and then sintered at high temperature. Sintering bonds the powder particles together while preserving a controlled level of interconnected porosity. After sizing and dimensional calibration, the component is impregnated with lubricating oil. The oil fills the internal pores and remains available for release during operation.
The resulting product combines the mechanical strength and wear resistance of tin bronze with the maintenance benefits of an oil-impregnated bearing. Unlike a conventional solid bronze bushing, it does not depend entirely on an external grease fitting or regular manual oil application. Instead, the bearing material itself functions as a lubricant reservoir.
The flanged configuration is particularly useful where axial movement must be controlled. During installation, the flange can seat against a housing shoulder or mounting surface, allowing the bushing to locate itself accurately. This can reduce assembly time and help maintain the alignment of the shaft, housing, and bearing surface.
Why Tin Bronze Is Suitable for Self-Lubricating Bushings
Tin bronze is widely used in bearing applications because it offers a balanced combination of strength, toughness, wear resistance, and compatibility with steel shafts. Copper provides a conductive and relatively soft base, while tin increases hardness, load-carrying ability, and resistance to deformation.
In powder metallurgy form, tin bronze can be manufactured with a carefully controlled pore structure. This structure is essential because it must retain sufficient oil while also providing enough solid material to support the applied load. The balance between density, porosity, hardness, and oil content strongly influences service performance.
Tin bronze also provides good resistance to seizure when the bushing is correctly matched with the shaft material, surface finish, clearance, load, speed, and operating environment. This is particularly important in pumps and industrial equipment, where a sudden seizure can damage the shaft, stop production, and require extensive maintenance.
Common material options include CuSn6 and CuSn8. The most appropriate grade depends on the required mechanical properties, operating speed, load, temperature, dimensional requirements, and environmental conditions. Material selection can be adjusted during product development to suit a particular pump or mechanical assembly.
Operating Principle of the Oil-Impregnated Structure
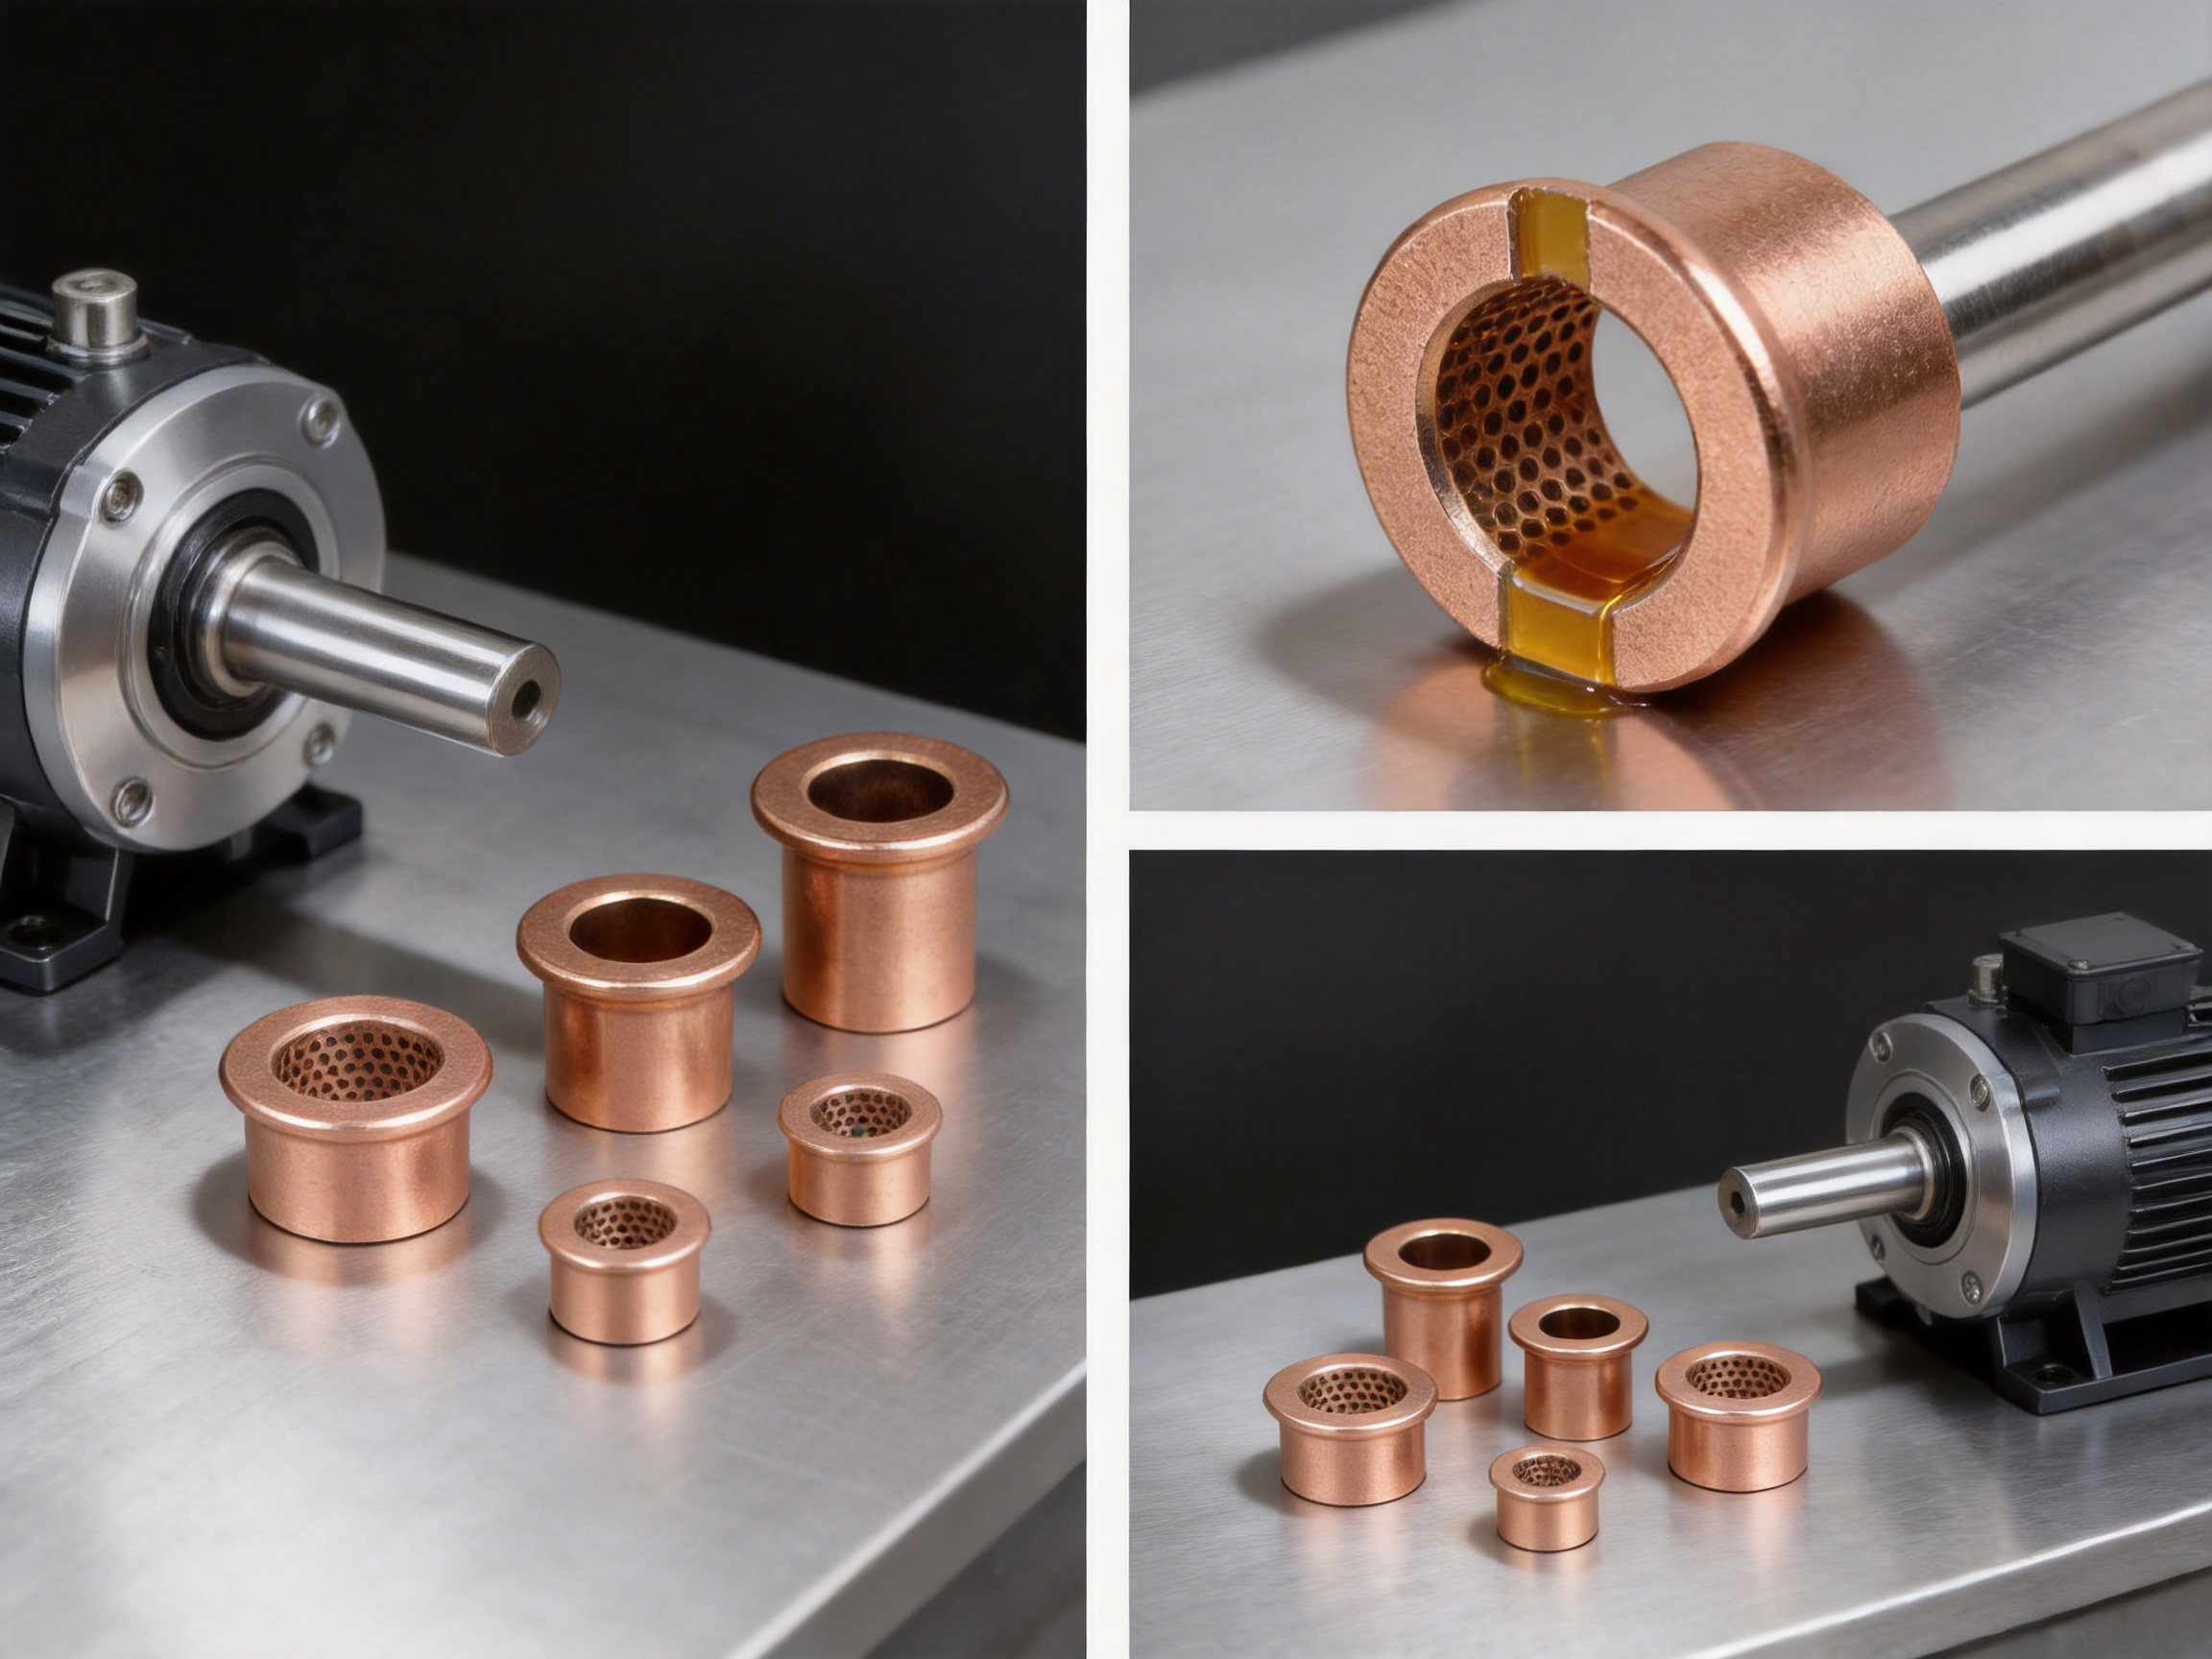
The self-lubricating function is based on the movement of oil between the internal pores and the bearing surface. The pores act as microscopic storage chambers distributed throughout the sintered bronze structure. Under normal operating conditions, the oil remains inside the bushing until frictional heat, pressure, and capillary action encourage a controlled amount to reach the sliding interface.
When the shaft begins to rotate or oscillate, friction is generated at the contact area. As the temperature of the bearing surface rises, the lubricating oil expands and migrates toward the surface. A thin oil film then forms between the shaft and the bushing. This film reduces direct metal-to-metal contact and lowers the energy required for movement.
When the equipment slows down or stops, the temperature decreases. A portion of the oil returns to the pores through capillary action and contraction. This reversible release-and-absorption cycle allows the bushing to replenish its lubricating film repeatedly during normal operation.
The system does not mean that the bushing can operate without any design limitations. The bearing still requires appropriate clearance, alignment, load, speed, temperature, and shaft finish. However, under suitable conditions, the oil-impregnated structure can significantly reduce the need for external lubrication and help maintain consistent performance over a long operating period.
Typical Self-Lubrication Cycle
1. The shaft starts rotating or oscillating inside the bushing.
2. Friction produces heat at the sliding interface.
3. Stored oil moves through the interconnected pores toward the bearing surface.
4. A thin lubricating film separates the shaft from the bronze surface.
5. Friction, wear, and operating temperature are reduced.
6. When the machine stops or cools, excess oil is drawn back into the porous structure.
7. The process repeats during subsequent operating cycles.
Key Advantages Over Conventional Bushings
Reduced Dependence on External Lubrication
Traditional bronze bushings often depend on grease, oil grooves, automatic lubrication systems, or scheduled manual lubrication. If lubrication is delayed, incorrectly applied, contaminated, or forgotten, friction and wear can increase rapidly. A self-lubricating bushing stores its lubricant internally, reducing dependence on maintenance personnel and external lubrication equipment.
This is especially useful in enclosed pump housings, remote installations, compact mechanisms, and equipment that operates continuously. Reducing the number of lubrication points can simplify equipment design and lower the total maintenance burden.
Lower Risk of Lubrication-Related Failure
External lubricants can leak, dry out, become contaminated, or be applied in an incorrect quantity. Too little lubricant may result in accelerated wear, while excessive grease can create drag, heat, seal problems, and contamination. Internal oil impregnation provides a more controlled source of lubrication within the bearing material.
Because the lubricant is stored in the bushing, the system is less vulnerable to certain external supply failures. This can improve reliability in pumps and machines where access is difficult or where scheduled service intervals are long.
Improved Resistance to Wear and Seizure
The combination of tin bronze and a continuous oil film helps reduce adhesive wear and surface damage. Tin bronze offers a durable bearing surface, while the lubricant reduces direct contact between the shaft and bushing. This combination can help prevent scoring, galling, and seizure when the product is correctly selected and installed.
The dense sintered skeleton provides structural support, while the pores retain the lubricant. The resulting material is not simply a soft porous metal; it is an engineered composite structure in which the metallic framework and oil content work together.
Integrated Axial Positioning
A plain cylindrical bushing may require a separate shoulder, retaining ring, washer, or press-fit arrangement to prevent axial movement. The integrated flange of a flanged bushing provides a built-in locating feature. It can simplify housing design and reduce the number of additional components.
Accurate axial positioning also helps maintain the intended bearing width and can reduce the possibility of the bushing moving away from the load zone. This is valuable in pump components, pedal mechanisms, actuators, and other assemblies where axial alignment affects operating stability.
Compact and Cost-Effective Construction
Powder metallurgy permits near-net-shape production. Compared with manufacturing a bushing entirely from machined bar stock, powder compaction can reduce material waste, machining time, and processing steps. The flange and cylindrical bearing surface can often be formed as one piece.
For medium- and high-volume production, this manufacturing approach can significantly reduce unit cost. It can also provide repeatable dimensions and consistent material characteristics once the tooling and process parameters have been validated.
Stable Operation in Continuous-Duty Equipment
Industrial pumps, motors, conveyors, and other machines may operate for thousands of hours each year. A bearing solution that requires frequent lubrication can increase service interruptions and labor costs. An oil-impregnated bushing can provide continuous lubrication during normal duty cycles, reducing the frequency of routine intervention.
The actual service life depends on load, speed, temperature, shaft condition, contamination, and operating environment. Nevertheless, the self-lubricating design is well suited to applications where consistent low-maintenance operation is a priority.
Technical Characteristics and Reference Values
The following values represent typical reference ranges for powder metallurgy self-lubricating tin bronze flanged bushings. Final values should be confirmed according to the selected material grade, component dimensions, operating conditions, and customer drawing.
| Parameter | Typical Reference Value |
| Material | Tin bronze, including CuSn6 or CuSn8 options |
| Oil content | 18% or higher, depending on product design |
| Density | Approximately 6.2–6.8 g/cm³ |
| Inner diameter range | Approximately 3–100 mm |
| Outer diameter range | Approximately 6–120 mm |
| Length range | Approximately 5–100 mm |
| Flange diameter | Typically 2–10 mm larger than the outer diameter |
| Operating temperature | Approximately -40°C to +220°C, subject to lubricant and application conditions |
| Dimensional accuracy | Up to approximately IT7–IT8 after sizing, depending on geometry |
| Reference ultimate PV value | Approximately 2.5 MPa·m/s without additional oil lubrication |
| Surface treatment | Natural finish, phosphating, tin plating, or other agreed treatment |
The PV value represents the relationship between bearing pressure and sliding velocity. It is an important reference when evaluating a plain bearing because a bushing may perform satisfactorily at a high load and low speed or at a low load and high speed, while the same combination may not be suitable at a high load and high speed.
Designers should also consider start-stop cycles, oscillating motion, shock loads, misalignment, vibration, fluid exposure, dust, installation interference, shaft hardness, shaft surface roughness, and heat dissipation. Technical data should be treated as a basis for selection rather than as a substitute for application testing.
Powder Metallurgy Manufacturing Process
Powder Selection and Material Preparation
The manufacturing process begins with the selection and preparation of bronze powder. Particle composition, particle size distribution, flow characteristics, compressibility, and cleanliness influence the final density and pore structure. Tin bronze powder must be controlled carefully to ensure that the finished material provides the required combination of strength, oil retention, and dimensional stability.
Material preparation may include blending alloy powders and approved processing additives. The mixture must remain uniform throughout production so that the finished bushings have consistent chemical composition and mechanical performance from batch to batch.
Precision Powder Compaction
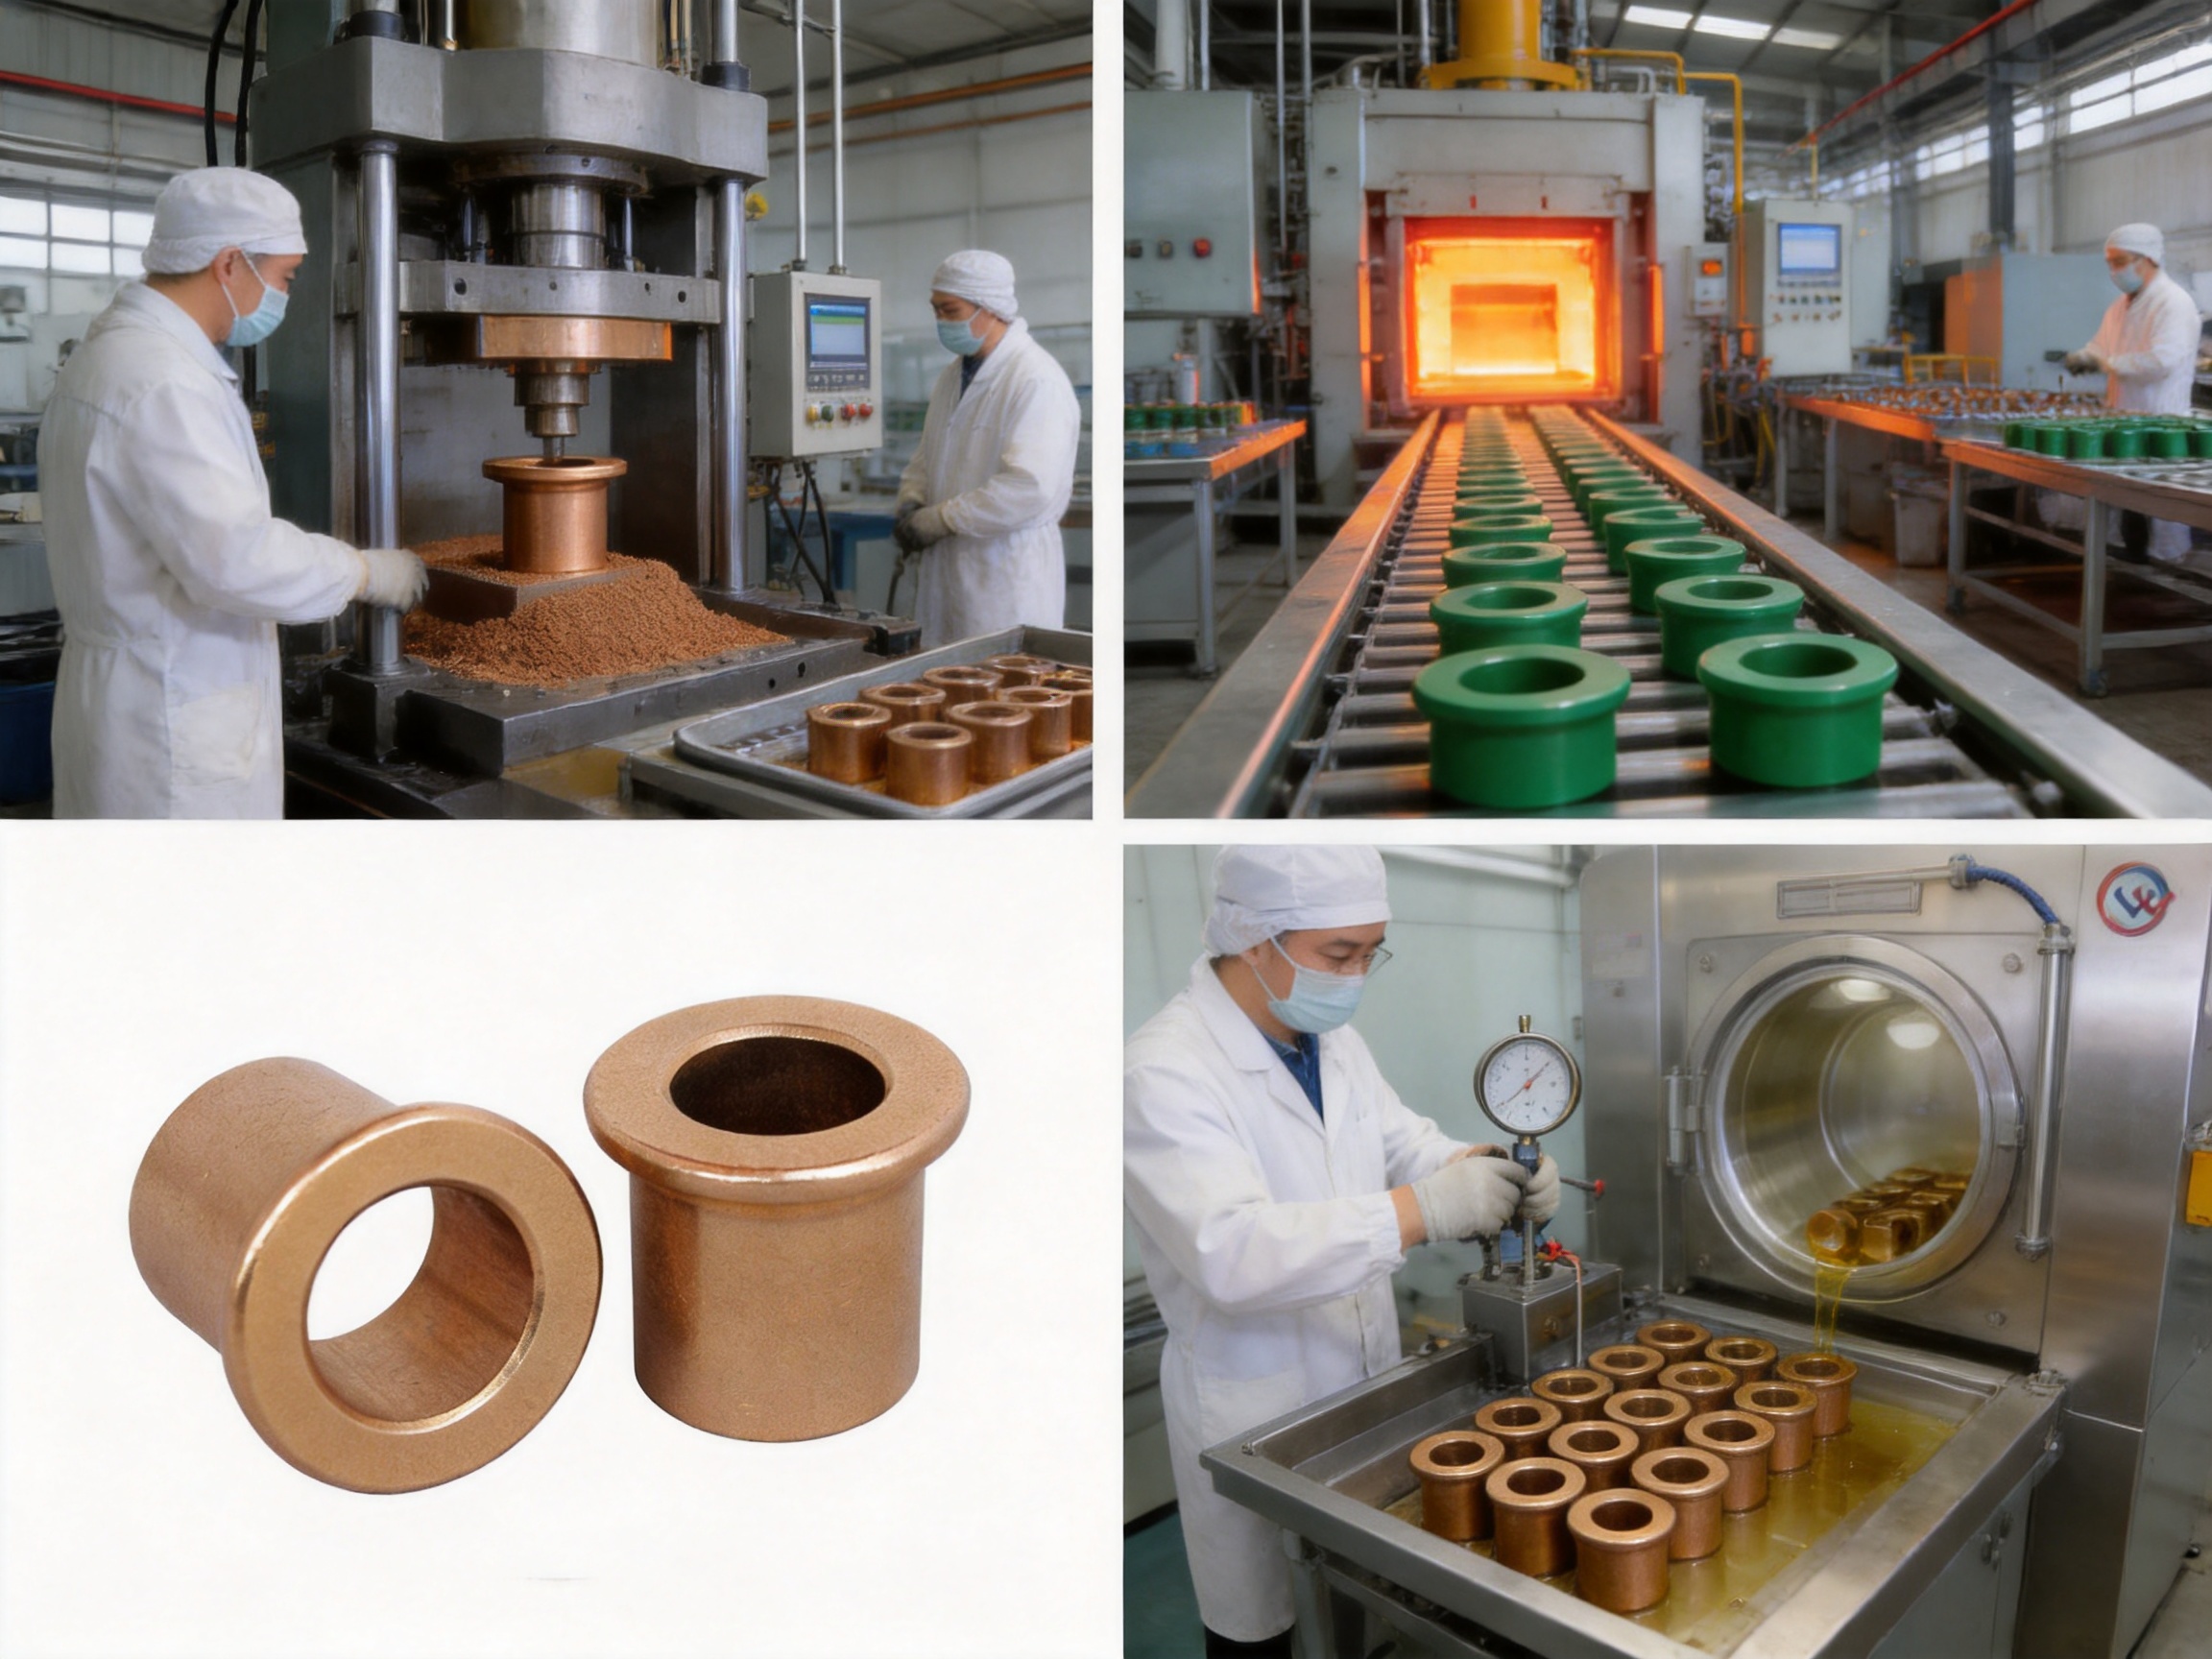
Prepared powder is placed into a forming die and compacted under controlled pressure. The die is designed to produce the inner diameter, outer diameter, bearing length, flange geometry, and other required features. Correct compaction is essential because it determines the initial shape and density distribution of the part.
Advanced presses and precision forming tools help produce consistent green components before sintering. Tooling must be designed to account for material flow, ejection, dimensional shrinkage, flange thickness, and the possibility of density differences between the bearing section and flange.
For customized products, the engineering team can develop tooling according to customer drawings or physical samples. This allows the bushing to be adapted to a specific housing, shaft, axial load requirement, or assembly method.
High-Temperature Sintering
The compacted component is heated in a controlled-atmosphere sintering furnace. During sintering, powder particles bond at their contact points and the component develops its final metallic framework. Temperature profile, furnace atmosphere, heating rate, holding time, and cooling conditions must be controlled to achieve the required strength and dimensional consistency.
The sintering process must preserve a suitable level of porosity. Excessive densification could reduce oil storage capacity, while insufficient bonding could reduce mechanical strength and wear resistance. Process engineers therefore balance density and porosity according to the intended application.
Sizing and Dimensional Calibration
After sintering, the components may be sized through a controlled calibration operation. Sizing improves dimensional accuracy, roundness, straightness, flange geometry, and surface consistency. It also helps ensure that the inner diameter and outer diameter meet the requirements of the shaft and housing fit.
Accurate sizing is particularly important for pump bushings. Excessive clearance can increase vibration, leakage, and wear, while insufficient clearance may cause high friction, overheating, or seizure. The correct fit must be determined based on the material, temperature, speed, load, shaft size, and operating environment.
Oil Impregnation
After dimensional calibration, the porous bronze bushing is impregnated with lubricating oil. The process is designed to fill the internal pore network with a controlled quantity of lubricant. Vacuum assistance or other controlled methods may be used to remove trapped air and improve oil penetration.
Oil content is an important quality characteristic. It must be high enough to support the intended self-lubricating function while maintaining the mechanical integrity of the bearing. The selected lubricant should also be compatible with the operating temperature, speed, surrounding materials, seals, and application environment.
Surface Treatment and Optional Machining
Depending on the application, the bushing may be supplied with a natural sintered surface or may receive an additional treatment such as phosphating or tin plating. These treatments can improve corrosion resistance, surface behavior, appearance, or compatibility with specific operating environments.
Related precision machining can be performed where the design requires features that cannot be produced entirely through compaction and sizing. Machining may include end-face finishing, special grooves, non-standard flange profiles, oil holes, steps, chamfers, or other customer-specific geometries.
Inspection and Release
Finished bushings are inspected according to the applicable control plan. Typical inspections may include dimensional measurement, visual inspection, density testing, oil content verification, surface condition checks, material verification, and sampling-based functional evaluation.
Inspection reports can be supplied for qualified orders. Traceability of raw materials, production batches, tooling, process parameters, and inspection results helps support stable quality and efficient problem resolution.
Quality Control and Manufacturing Strengths
Jiande Welfine Technology Co., Ltd. integrates research and development, production, precision machining, testing, and sales. This integrated structure allows the company to manage the complete product cycle from initial design review through mass production and delivery.
The company operates a modern production base covering approximately 13,039 square meters. The facility includes high-efficiency powder presses, high-temperature sintering furnaces, precision forming machines, and inspection equipment. These resources support the manufacture of bushings, self-lubricating bearing components, and other precision sintered parts.
More than 150 skilled employees contribute to production, engineering, quality management, tooling, inspection, and customer service. The company’s more than 20 years of experience in powder metallurgy provides a practical foundation for handling different material grades, shapes, tolerances, production quantities, and application requirements.
Quality management is supported by ISO 9001:2015 and IATF 16949:2016 certifications. These systems encourage controlled documentation, process monitoring, corrective action, supplier management, inspection planning, and continual improvement. For customers in automotive, industrial, pump, and machinery markets, a structured quality system provides greater confidence in batch-to-batch consistency.
Engineering Support for OEM and ODM Projects
Self-lubricating bushings are not always interchangeable. A part that appears similar in size may perform differently because of variations in clearance, flange thickness, oil content, density, shaft material, or operating speed. For this reason, engineering cooperation is important during product development.
Customers can provide drawings, samples, technical specifications, or application information. The engineering team can review the requirements and recommend suitable dimensions, material grades, tolerance ranges, surface treatments, and production methods. Support is available for both original equipment manufacturing and original design manufacturing projects.
Small-batch trial production can be used to verify assembly fit and operating behavior before larger quantities are released. This approach helps identify design improvements at an early stage and reduces the risk of costly modifications after mass production has started.
Near-Net-Shape Production and Cost Control
Powder metallurgy is efficient because it converts a measured quantity of powder into a shape close to the final component geometry. Compared with producing the same part from a solid copper alloy bar, this can reduce cutting waste and machining time. The integrated flange can also be formed as part of the component rather than being assembled separately.
For suitable production volumes, near-net-shape manufacturing may reduce costs by more than 30 percent compared with traditional machined copper bushings. The actual savings depend on geometry, tolerance, material, tooling, quantity, secondary operations, and quality requirements.
Applications in Pump Systems
Centrifugal Pumps
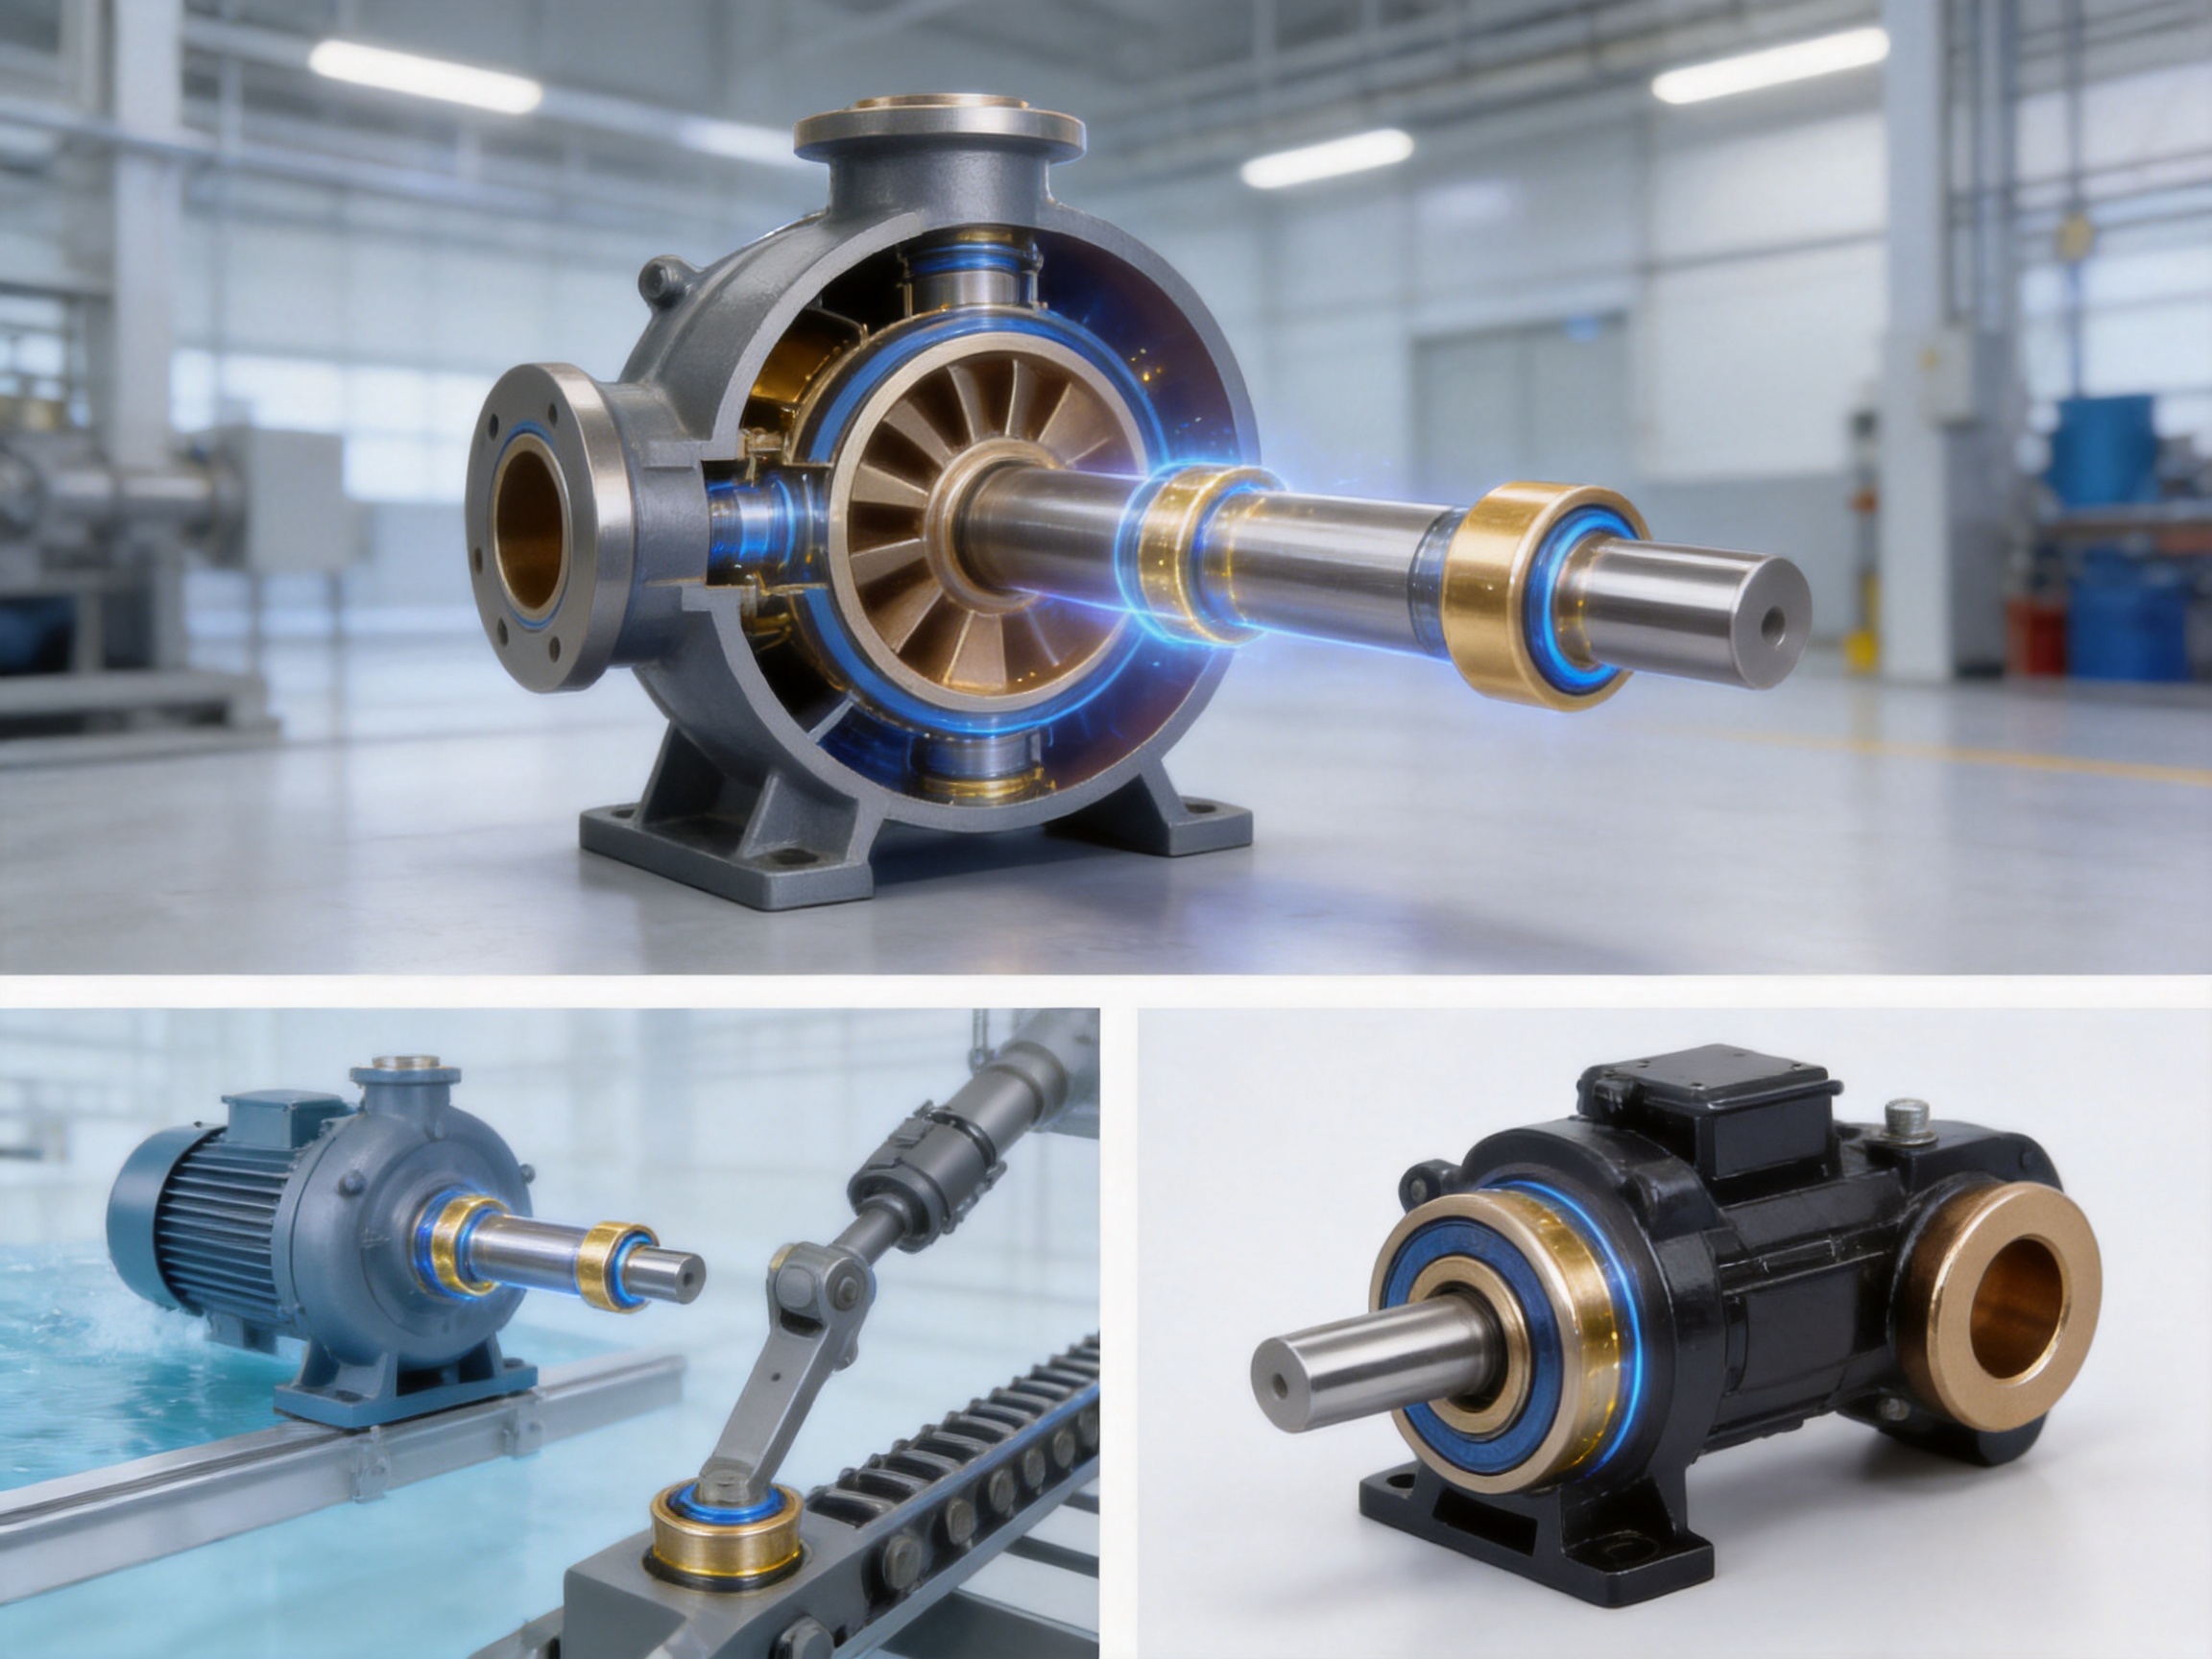
Centrifugal pumps often contain rotating shafts, impellers, sleeves, and support components that require controlled radial clearance. A self-lubricating flanged bushing can be used in selected support or positioning locations where the load, speed, temperature, and fluid exposure are suitable.
The flanged design can assist with axial location and simplify assembly within a pump housing. The oil-impregnated structure can also reduce the need for a separate grease supply in locations where external lubrication is undesirable.
Water Circulation Pumps
Water circulation equipment may operate continuously in heating, cooling, building services, industrial process, and water treatment installations. Maintenance access can be limited, particularly when pumps are installed inside equipment rooms, below platforms, or within integrated systems.
Self-lubricating bushings can help reduce routine servicing requirements. When used in an appropriate location and protected from unsuitable fluid exposure, they can support stable shaft movement and reduce friction-related energy loss.
Chemical Transfer Pumps
Chemical processing equipment requires careful material and lubricant compatibility assessment. The bushing material, impregnating oil, surface treatment, seals, and process fluid must be reviewed together. Tin bronze may be suitable for selected chemical transfer applications, but the exact chemical concentration, temperature, pressure, and exposure time must be evaluated before approval.
Where the operating environment is appropriate, the internally lubricated design can reduce the risk of external grease contamination entering the process area. Application testing and compatibility confirmation are recommended for aggressive chemicals or unusual temperatures.
Agricultural Irrigation Pumps
Agricultural pumps often operate in dusty, humid, or difficult-to-access environments. External grease systems may attract abrasive dust or require frequent servicing during demanding seasonal operation. A self-lubricating flanged bushing can reduce the number of maintenance tasks and help protect the sliding interface from certain external contaminants.
Industrial Cooling Pumps
Cooling pumps may run for extended periods and are often linked to production equipment that must remain available. A bearing component that reduces the risk of lubrication-related failure can contribute to lower downtime and more predictable maintenance planning.
Marine and Hydraulic Equipment
Marine pump systems, hydraulic assemblies, and related equipment may contain compact mechanisms exposed to vibration, moisture, or restricted service access. The bushing design can be adapted with suitable materials, dimensional tolerances, surface treatments, and protective measures. The specific environment must be reviewed to determine whether the standard oil-impregnated design is appropriate.
Applications Beyond Pumps
The product is also used in automotive mechanisms such as steering systems, brake pedal assemblies, seat adjustment mechanisms, hinges, linkages, and actuators. In these applications, compact size, low maintenance, smooth movement, and reliable positioning are important.
Construction machinery can use flanged bushings in selected pin connections, hydraulic pump components, valve groups, and control mechanisms. The integrated flange can simplify retention, while the tin bronze material can support repeated movement under appropriate load and speed conditions.
Textile machinery, printing equipment, office equipment, reducers, motors, conveyors, and general transmission components can also benefit from self-lubricating bearing solutions. The product can be designed for rotating, oscillating, or intermittent movement depending on the application.
When used in office equipment or precision mechanisms, dimensional accuracy and low operating noise may be especially important. When used in construction machinery or industrial equipment, load capacity, impact resistance, and wear life may receive greater emphasis. The same basic bushing concept can therefore be adjusted to meet different performance priorities.
Comparison with Other Bearing Solutions
| Characteristic | Self-Lubricating Tin Bronze Flanged Bushing | Conventional Solid Bronze Bushing | Grease-Dependent Plain Bushing |
| Lubrication method | Oil stored in internal pores | External oil or grease, depending on design | Regular external grease application |
| Maintenance requirement | Low under suitable conditions | Moderate to high | Regular lubrication required |
| Axial positioning | Provided by integrated flange | May require additional design features | May require additional design features |
| Risk of missed lubrication | Reduced | Higher if external lubricant is required | High when service intervals are missed |
| Material utilization | Efficient near-net-shape production | More machining may be required | Depends on manufacturing method |
| Suitable operating mode | Rotating, oscillating, and intermittent motion | Rotating or oscillating motion with suitable lubrication | Motion requiring routine lubrication |
| Customization potential | High for dimensions, flange, material, and treatment | High but potentially more machining-intensive | Dependent on construction and supplier capability |
| Contamination exposure | Reduced exposure of lubricant to external contaminants | Dependent on lubrication arrangement | External grease may attract contaminants |
This comparison is intended as a general guide. A self-lubricating bushing is not automatically the best solution for every application. Rolling bearings, polymer bushings, bronze-plated components, or fully lubricated solid bushings may be more appropriate in certain conditions. Proper technical selection remains essential.
Design Considerations for Engineers
Load and Speed
Calculate the projected bearing area using the bearing length and shaft diameter. The resulting pressure should be evaluated together with the sliding speed to determine the operating PV value. Starting friction, peak load, shock load, and intermittent operation should also be considered rather than evaluating only the average running condition.
Clearance and Fit
Clearance must allow the shaft to rotate freely without excessive movement. The appropriate value depends on shaft diameter, speed, operating temperature, material expansion, lubrication, load, and housing conditions. A clearance that is suitable at room temperature may be insufficient at elevated operating temperature.
The housing fit must hold the bushing securely without distorting the inner diameter. Excessive interference can close the running clearance, while insufficient interference can allow the bushing to move in the housing. Installation tolerances should therefore be specified together with the shaft and housing materials.
Shaft Condition
The mating shaft should have suitable hardness, roundness, straightness, and surface roughness. A damaged, rough, or contaminated shaft can rapidly wear the bushing and disrupt the oil film. Replacing a worn bushing without inspecting the shaft may lead to premature failure of the new component.
Alignment
Misalignment can concentrate the load on one edge of the bushing, causing uneven wear and elevated temperature. The housing, shaft, and adjacent components should be aligned as accurately as practical. If unavoidable misalignment is expected, the bearing design should be reviewed before production.
Temperature
Operating temperature affects oil viscosity, dimensional clearance, material strength, and lubricant evaporation. The stated reference range of approximately -40°C to +220°C must be evaluated together with the selected lubricant and actual duty cycle. Continuous operation at the upper temperature limit may require special material or lubricant selection.
Environment and Contamination
Dust, abrasive particles, water, cleaning chemicals, process fluids, and salt spray can influence service life. Seals, shields, protective coatings, or alternative material treatments may be considered where the environment is severe. The bushing should not be exposed to a fluid that dissolves, washes out, or chemically degrades the impregnating oil unless the design has been specifically developed for that condition.
Installation Recommendations
Before installation, confirm the bushing dimensions, shaft condition, housing dimensions, orientation, and flange seating surface. The housing should be clean and free from burrs, chips, rust, and foreign material. The shaft should be checked for scoring, excessive roughness, bending, and incorrect diameter.
Use a suitable press tool that applies force evenly around the bushing or through an approved installation surface. Do not apply installation force directly to a thin flange if doing so could distort or crack the component. The flange should seat evenly against the intended shoulder or mounting surface.
Do not hammer the bushing into position unless a specifically approved installation procedure permits it. Impact can damage the flange, deform the bearing bore, or create hidden cracks. A controlled press-fit operation generally provides better results.
After installation, verify that the shaft rotates freely and that there is no abnormal binding. For a new assembly, check end play, radial movement, noise, temperature, and vibration during initial operation. Early monitoring can identify an incorrect fit, misalignment, or unexpected load before serious damage occurs.
Maintenance and Service-Life Management
The principal maintenance benefit of an oil-impregnated bushing is the reduction of routine lubrication work. However, the surrounding equipment should still be inspected regularly. Maintenance personnel should check for unusual noise, temperature rise, vibration, shaft movement, leakage, contamination, and changes in operating performance.
Do not automatically add grease or oil to a self-lubricating bushing unless the application documentation specifically recommends it. An incompatible or excessive lubricant may alter friction behavior, attract contamination, damage seals, or interfere with the intended oil-release mechanism.
If a bushing shows accelerated wear, investigate the underlying cause. Possible causes include excessive load, excessive speed, misalignment, insufficient clearance, poor shaft finish, contamination, high temperature, fluid incompatibility, incorrect installation, or an unsuitable lubricant. Replacing the component without correcting the cause may result in repeated failure.
For critical pump systems, operators may establish condition-based maintenance using temperature, vibration, noise, energy consumption, and shaft movement as indicators. This approach can help identify gradual wear while the equipment is still operating and allow replacement to be planned during a scheduled shutdown.
Customization Options
Jiande Welfine Technology Co., Ltd. supports customization of the inner diameter, outer diameter, overall length, flange diameter, flange thickness, chamfer, step, groove, and other geometric features. These options allow the bushing to match existing pump housings and mechanical assemblies.
Material customization may include different tin bronze grades, density targets, oil contents, and lubricant choices. The appropriate specification depends on the load, speed, temperature, atmosphere, surrounding fluid, and required service life.
Surface treatment options include natural finish, phosphating, tin plating, and other agreed treatments. A surface treatment may be selected to improve corrosion resistance, assembly behavior, appearance, or compatibility with a particular environment.
Customers may request development based on a drawing, sample, three-dimensional model, or technical description. The engineering process can include drawing review, feasibility analysis, tooling design, prototype production, dimensional inspection, assembly verification, and mass-production approval.
Production, Packaging, and Delivery
Standard products may be available from stock, while customized products can be scheduled according to tooling, quantity, inspection, and processing requirements. Typical delivery for customized parts is approximately 7–15 days after production conditions are confirmed, although actual timing depends on design complexity, order quantity, tooling status, and customer approval requirements.
Each bushing should be protected against moisture, contamination, impact, and oxidation during transportation. Independent moisture-resistant packaging helps maintain product condition and reduces the risk of damage during storage and delivery.
Packaging specifications can be adjusted for export shipments, automated production lines, bulk handling, or individual component protection. Customers with special labeling, batch identification, palletization, or documentation requirements can confirm these details during order review.
Why Choose an Experienced Powder Metallurgy Manufacturer?
The performance of a self-lubricating bushing depends on more than its external dimensions. Porosity, density distribution, oil content, sintering quality, sizing accuracy, flange integrity, surface condition, and material consistency all influence service life. An experienced powder metallurgy manufacturer can manage these variables through established equipment, tooling knowledge, process controls, and inspection procedures.
Jiande Welfine Technology Co., Ltd. combines powder metallurgy production with related precision machining. This allows the company to provide both standard components and customized parts that require additional operations. Customers can work with one supplier for material selection, tooling, forming, sintering, sizing, machining, surface treatment, inspection, and delivery.
The company’s focus on OEM and ODM cooperation supports the needs of equipment manufacturers, pump producers, automotive suppliers, industrial distributors, and engineering contractors. Its technical team can assist with early design decisions that influence cost, manufacturability, performance, and delivery time.
With ISO 9001:2015 and IATF 16949:2016 certifications, modern equipment, trained personnel, and a dedicated production base, the company is positioned to support both trial orders and repeat production. The objective is not simply to produce a bushing, but to provide a stable bearing solution that performs consistently within the customer’s complete assembly.
How the Product Supports Pump Reliability
Pump reliability is influenced by many parts, including seals, shafts, impellers, couplings, valves, motors, and bearings. The bushing is a relatively small component, but its failure can create vibration, shaft damage, leakage, reduced efficiency, and unplanned downtime.
A self-lubricating tin bronze flanged bushing supports reliability in several ways. Its internal oil reservoir reduces dependence on external lubrication. Its tin bronze framework provides a durable sliding surface. Its flange helps maintain axial position. Its powder metallurgy construction enables controlled porosity and repeatable dimensions. Its customizable geometry allows better integration with the pump housing.
When these characteristics are combined with correct application design and quality manufacturing, the bushing can help maintain smoother shaft rotation, lower friction, reduced wear, and more predictable maintenance. These benefits can contribute to improved pump availability and lower ownership cost over the service life of the equipment.
Frequently Asked Questions
What is the main benefit of a self-lubricating flanged bronze bushing?
The main benefit is the ability to provide continuous internal lubrication while also offering integrated axial positioning. The porous bronze structure stores oil and releases it to the bearing surface during operation, reducing the need for regular external lubrication.
Can this bushing be used in water pumps?
It can be used in selected water pump applications when the load, speed, temperature, clearance, shaft condition, and fluid exposure are suitable. The compatibility of the impregnating oil and the surrounding water or process fluid should be confirmed before final approval.
What materials are available?
Tin bronze grades such as CuSn6 and CuSn8 are available. The final material selection may be adjusted according to required strength, wear resistance, oil content, density, operating temperature, and application conditions.
What dimensions can be customized?
The inner diameter, outer diameter, length, flange diameter, flange thickness, steps, chamfers, grooves, and other features can be customized according to drawings or samples. The available range is approximately 3–100 mm for the inner diameter, 6–120 mm for the outer diameter, and 5–100 mm for length, subject to design review.
Does the bushing require additional grease?
Under suitable operating conditions, the oil-impregnated bushing is designed to operate without routine external grease. Additional lubricant should not be applied unless it has been approved for the specific product and application.
How does the flange improve installation?
The flange provides an integrated locating surface. It can seat against a housing shoulder, prevent axial movement, support selected axial loads, and simplify assembly by reducing the need for separate retaining components.
What is the expected service life?
Service life depends on load, speed, PV value, shaft condition, clearance, alignment, temperature, contamination, lubricant compatibility, and operating cycles. A precise life estimate requires application data and may require prototype or endurance testing.
Can the product be used for oscillating motion?
Yes, the bushing can be considered for oscillating and intermittent movement as well as continuous rotation. Oscillating applications should be reviewed separately because short stroke length, reversal frequency, edge loading, and lubricant redistribution can affect performance.
What surface treatments are available?
Natural finish, phosphating, tin plating, and other agreed surface treatments may be available. The most suitable treatment depends on corrosion exposure, assembly requirements, wear conditions, and customer specifications.
How is oil retained inside the bushing?
Oil is retained within interconnected pores created during powder metallurgy sintering. During operation, heat and movement encourage controlled oil release to the bearing surface. When the component cools, part of the oil can return to the pore network.
Can the company produce small trial batches?
Yes. Small-batch trial production is supported for qualified customization projects. Trial parts can be used to verify dimensional fit, installation, operating conditions, and design suitability before volume production.
What information should be provided for a quotation?
Useful information includes the drawing or sample, shaft diameter, housing dimensions, bearing length, flange geometry, load, speed, motion type, operating temperature, surrounding fluid, environmental conditions, quantity, surface treatment, and required delivery schedule.
What quality documents can be provided?
Depending on the order and customer requirements, quality documents may include material information, dimensional inspection reports, batch identification, process records, and other agreed inspection documentation.
How should a worn bushing be investigated?
Inspect the shaft, housing, alignment, clearance, load, speed, contamination, temperature, and lubrication conditions. Wear may be caused by a system issue rather than by the bushing alone. Corrective action should be completed before installing a replacement part.
Conclusion
Powder metallurgy self-lubricating tin bronze flanged bushings provide a practical combination of internal oil storage, wear resistance, low maintenance, accurate positioning, and near-net-shape manufacturing efficiency. They are particularly valuable in pumps and industrial mechanisms where external lubrication is inconvenient, service access is limited, or continuous operation is required.
The integrated flange simplifies assembly and helps control axial movement. The porous tin bronze structure provides a controlled lubricant reservoir and a durable bearing framework. Through appropriate material selection, dimensional control, sizing, oil impregnation, surface treatment, and inspection, the bushing can be adapted to a wide range of rotating and oscillating applications.
Jiande Welfine Technology Co., Ltd. supports these products with powder metallurgy expertise, OEM and ODM customization, modern production equipment, precision machining capabilities, structured quality management, and technical assistance based on customer drawings or samples. For pump manufacturers and industrial equipment producers, this combination can provide a reliable path from initial component design to stable repeat production.
Correct application engineering remains essential. Load, speed, clearance, temperature, shaft condition, alignment, contamination, and chemical compatibility must all be evaluated. When these factors are properly controlled, a self-lubricating tin bronze flanged bushing can help reduce friction, extend service life, lower maintenance frequency, and improve the reliability of the complete machine.
References
1. Powder Metallurgy Materials and Processes, technical reference literature on compaction, sintering, sizing, and porous metal structures.
2. Plain Bearings and Sliding Contacts, engineering reference literature on bearing pressure, sliding velocity, PV values, clearance, and wear mechanisms.
3. Copper and Copper Alloy Data, technical reference information on tin bronze composition, mechanical properties, wear resistance, and industrial applications.
4. ISO 9001:2015, Quality Management Systems — Requirements.
5. IATF 16949:2016, Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
6. Industrial Pump Engineering, reference materials covering pump shafts, bushings, alignment, lubrication, vibration, and maintenance practices.
7. Powder Metallurgy Self-Lubricating Bearing Design Guidelines, technical literature concerning oil impregnation, porosity, operating temperature, and application selection.
Product: Powder Metallurgy Self-lubricating Tin Bronze Flanged Bushing
Related products
-
-
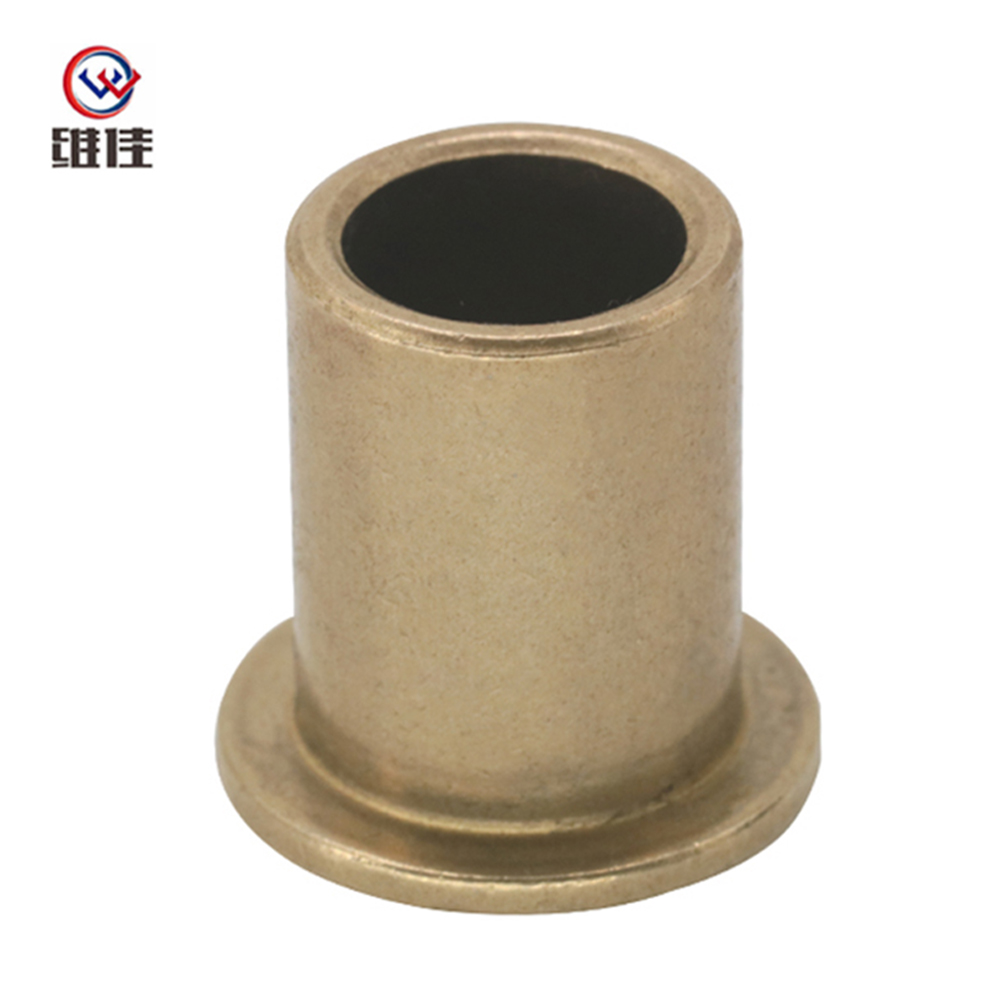
Our sintered bronze self-lubricating bearings are engineered for demanding industrial applications where traditional lubrication is impractical. Designed with advanced powder metallurgy technology, th...
See Details
Copyright © Jiande Welfine Technology Co., Ltd. All Rights Reserved. Privacy Custom Self-lubricating Sintered Bushing Manufacturers
