E-mail us: [email protected]
Tel: +86-15239857375
 English
 中文简体


 Home / Author / Tan Xinyue — After-Sales Technical Coordinator / CuSn10 Powder Metallurgy Bronze Bushing: Precision Self-Lubricating Performance for High-Load Machinery
CuSn10 Powder Metallurgy Bronze Bushing: Precision Self-Lubricating Performance for High-Load Machinery
 2026.09.12
 Tan Xinyue — After-Sales Technical Coordinator
Content
- 1 1. Product Overview
- 2 2. Why CuSn10 Is Suitable for Bushing Applications
- 3 3. Self-Lubricating Structure and Operating Principle
- 4 4. Advanced Powder Metallurgy Manufacturing Process
- 5 5. Quality Control and Manufacturing Strengths
- 6 6. Advantages Over Conventional Bushing Materials
- 7 7. Performance Benefits in Industrial Equipment
- 8 8. Application Areas
- 9 9. Design and Selection Considerations
- 10 10. Custom Manufacturing and OEM Support
- 11 11. Installation and Maintenance Recommendations
- 12 12. How Product Quality Is Evaluated
- 13 13. Why Process Integration Matters
- 14 14. Sustainability and Cost Efficiency
- 15 15. Future Development of Powder Metallurgy Bushings
- 16 16. Frequently Asked Questions
- 16.1 Can the CuSn10 powder metallurgy bronze bushing operate without regular manual lubrication?
- 16.2 Is CuSn10 suitable for high-speed rotating equipment?
- 16.3 What is the main difference between a powder metallurgy bronze bushing and a cast bronze bushing?
- 16.4 Why is vacuum used during oil impregnation?
- 16.5 What does the 5.7–5.8 g/cm³ density specification indicate?
- 16.6 What is the purpose of the 0.4 × 45° chamfer?
- 16.7 Can the bushing be customized according to a drawing?
- 16.8 What information is needed to select the correct bushing?
- 16.9 How can premature bushing wear be prevented?
- 16.10 Does oil impregnation leave the outside of the bushing oily?
- 16.11 What quality certifications support production capability?
- 16.12 Are these bushings appropriate for hydraulic systems?
- 16.13 What delivery support is available for customized products?
- 17 17. Conclusion
- 18 References
- 19 Product: Powder Metallurgy Bronze Bushing (A0667)
Modern machinery increasingly depends on compact components that can operate reliably under load, repeated motion, limited lubrication access, and demanding dimensional requirements. Among these components, bushings play a fundamental role. They support shafts, guide moving members, reduce friction, absorb wear, and help maintain alignment between mating parts. Although a bushing may appear simple, its material composition, internal structure, manufacturing accuracy, and lubrication method directly influence the reliability and service life of the complete machine.
The CuSn10 powder metallurgy bronze bushing is designed for applications that require a balanced combination of wear resistance, load-carrying capability, dimensional accuracy, corrosion resistance, and reduced maintenance. Manufactured from a copper-tin alloy containing approximately 10% tin, this bushing uses a controlled porous structure to retain lubricating oil. During operation, the stored oil can gradually migrate toward the sliding surface, helping form a stable lubricating film and reducing direct metal-to-metal contact.
Compared with many conventional brass bushings, machined bronze sleeves, and ordinary cast components, the CuSn10 powder metallurgy bushing offers important advantages in oil retention, production consistency, material utilization, and self-lubricating performance. It is suitable for precision machinery, automotive assemblies, hydraulic systems, fans, refrigerators, electric motors, automation equipment, agricultural machinery, and other industrial applications where dependable movement and reduced maintenance are important.
This article examines the product structure, material characteristics, manufacturing process, quality controls, application advantages, customization capabilities, and selection considerations associated with the CuSn10 powder metallurgy bronze bushing.
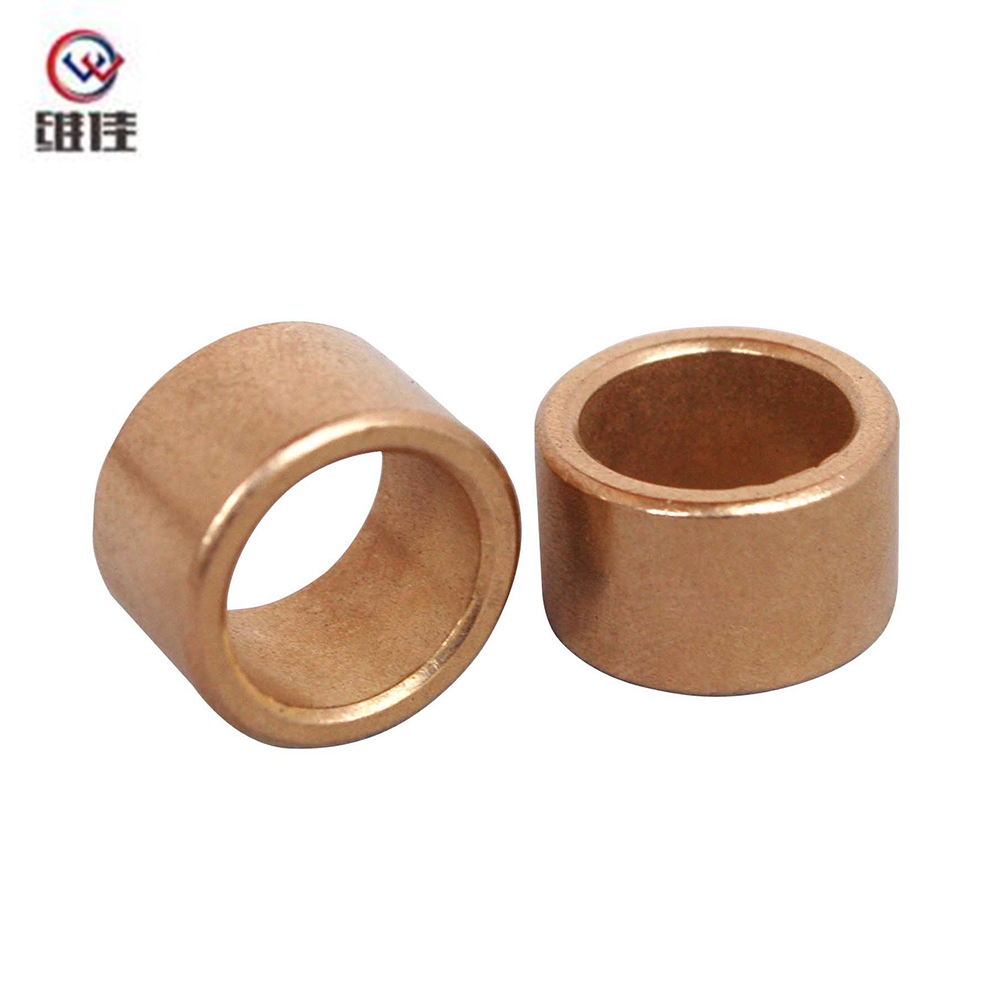
Powder Metallurgy Bronze Bushing (A0667)
1. Product Overview
The CuSn10 powder metallurgy bronze bushing is produced through an integrated sequence of powder preparation, compaction, sintering, sizing, precision processing, cleaning, oil impregnation, inspection, and packaging. Each stage contributes to the final performance of the component.
The supplied product specification is identified by code A0667. It is designed as a compact cylindrical bushing with controlled inner and outer dimensions, a defined chamfer, carefully regulated density, and a concentricity requirement suitable for precision assembly.
| Product Item | Specification |
| Product Name | Powder Metallurgy Bronze Bushing |
| Product Code | A0667 |
| Material | CuSn10 copper-tin bronze |
| Nominal Specification | 10G7 × 13s7 × 10 mm |
| Chamfer | 0.4 × 45° |
| Weight | 3.36–3.41 g |
| Density | 5.7–5.8 g/cm³ |
| Concentricity | ≤0.05 mm |
| Sintering Parameter | TCI 690 ± 30°C |
| Impregnation Oil | 46# mechanical oil |
| Impregnation Environment | Vacuum environment at approximately 80°C |
The dimensions and tolerance values demonstrate that the bushing is not simply a porous metal sleeve. It is a precision-engineered component manufactured for controlled assembly. The inner diameter must provide suitable shaft clearance, while the outer diameter must fit securely into the housing. Concentricity is also important because misalignment can produce uneven contact, localized heating, accelerated wear, and unstable operation.
The 0.4 × 45° chamfer helps guide the bushing during installation and reduces the possibility of interference at the housing entrance. It also reduces sharp edges that could damage mating components or create handling risks during assembly.
2. Why CuSn10 Is Suitable for Bushing Applications
CuSn10 is a copper-based bronze alloy containing approximately 10% tin. Copper provides good thermal conductivity and a strong metallic base, while tin contributes to hardness, wear resistance, and improved performance under sliding contact. This combination makes CuSn10 suitable for applications where a bushing must support movement while resisting friction and surface damage.
The alloy is particularly useful when equipment operates under repeated rotation, oscillation, intermittent movement, or moderate to high mechanical loading. Its copper-based structure can help conduct heat away from the sliding area, reducing the risk of excessive temperature accumulation. The tin content improves the ability of the material to withstand surface wear compared with softer copper or standard brass alternatives.
In a powder metallurgy bushing, the alloy composition is only one part of the performance equation. The manufacturing process creates a controlled network of pores throughout the material. These pores are later filled with oil, giving the bushing a self-lubricating function that is not normally available in a dense, nonporous machined sleeve.
The balance between strength and porosity is critical. Excessive porosity may reduce mechanical strength and dimensional stability. Insufficient porosity may reduce oil retention and limit the self-lubricating effect. A reliable manufacturer must therefore control the powder formulation, compaction pressure, sintering cycle, density, and sizing operation as an integrated system.
| Performance Factor | CuSn10 Powder Metallurgy Bronze | Typical Brass Bushing |
| Wear Resistance | High | Moderate |
| Oil Retention | Excellent due to controlled porosity | Limited in dense material |
| Self-Lubrication | Available after oil impregnation | Usually requires external lubrication |
| Load Capability | Suitable for many medium- and high-load applications | Depends strongly on alloy and design |
| Thermal Conductivity | Good | Good to moderate |
| Mass Production Consistency | High when process parameters are controlled | Varies with machining and casting conditions |
| Material Utilization | Efficient powder-based production | More material may be removed during machining |
3. Self-Lubricating Structure and Operating Principle
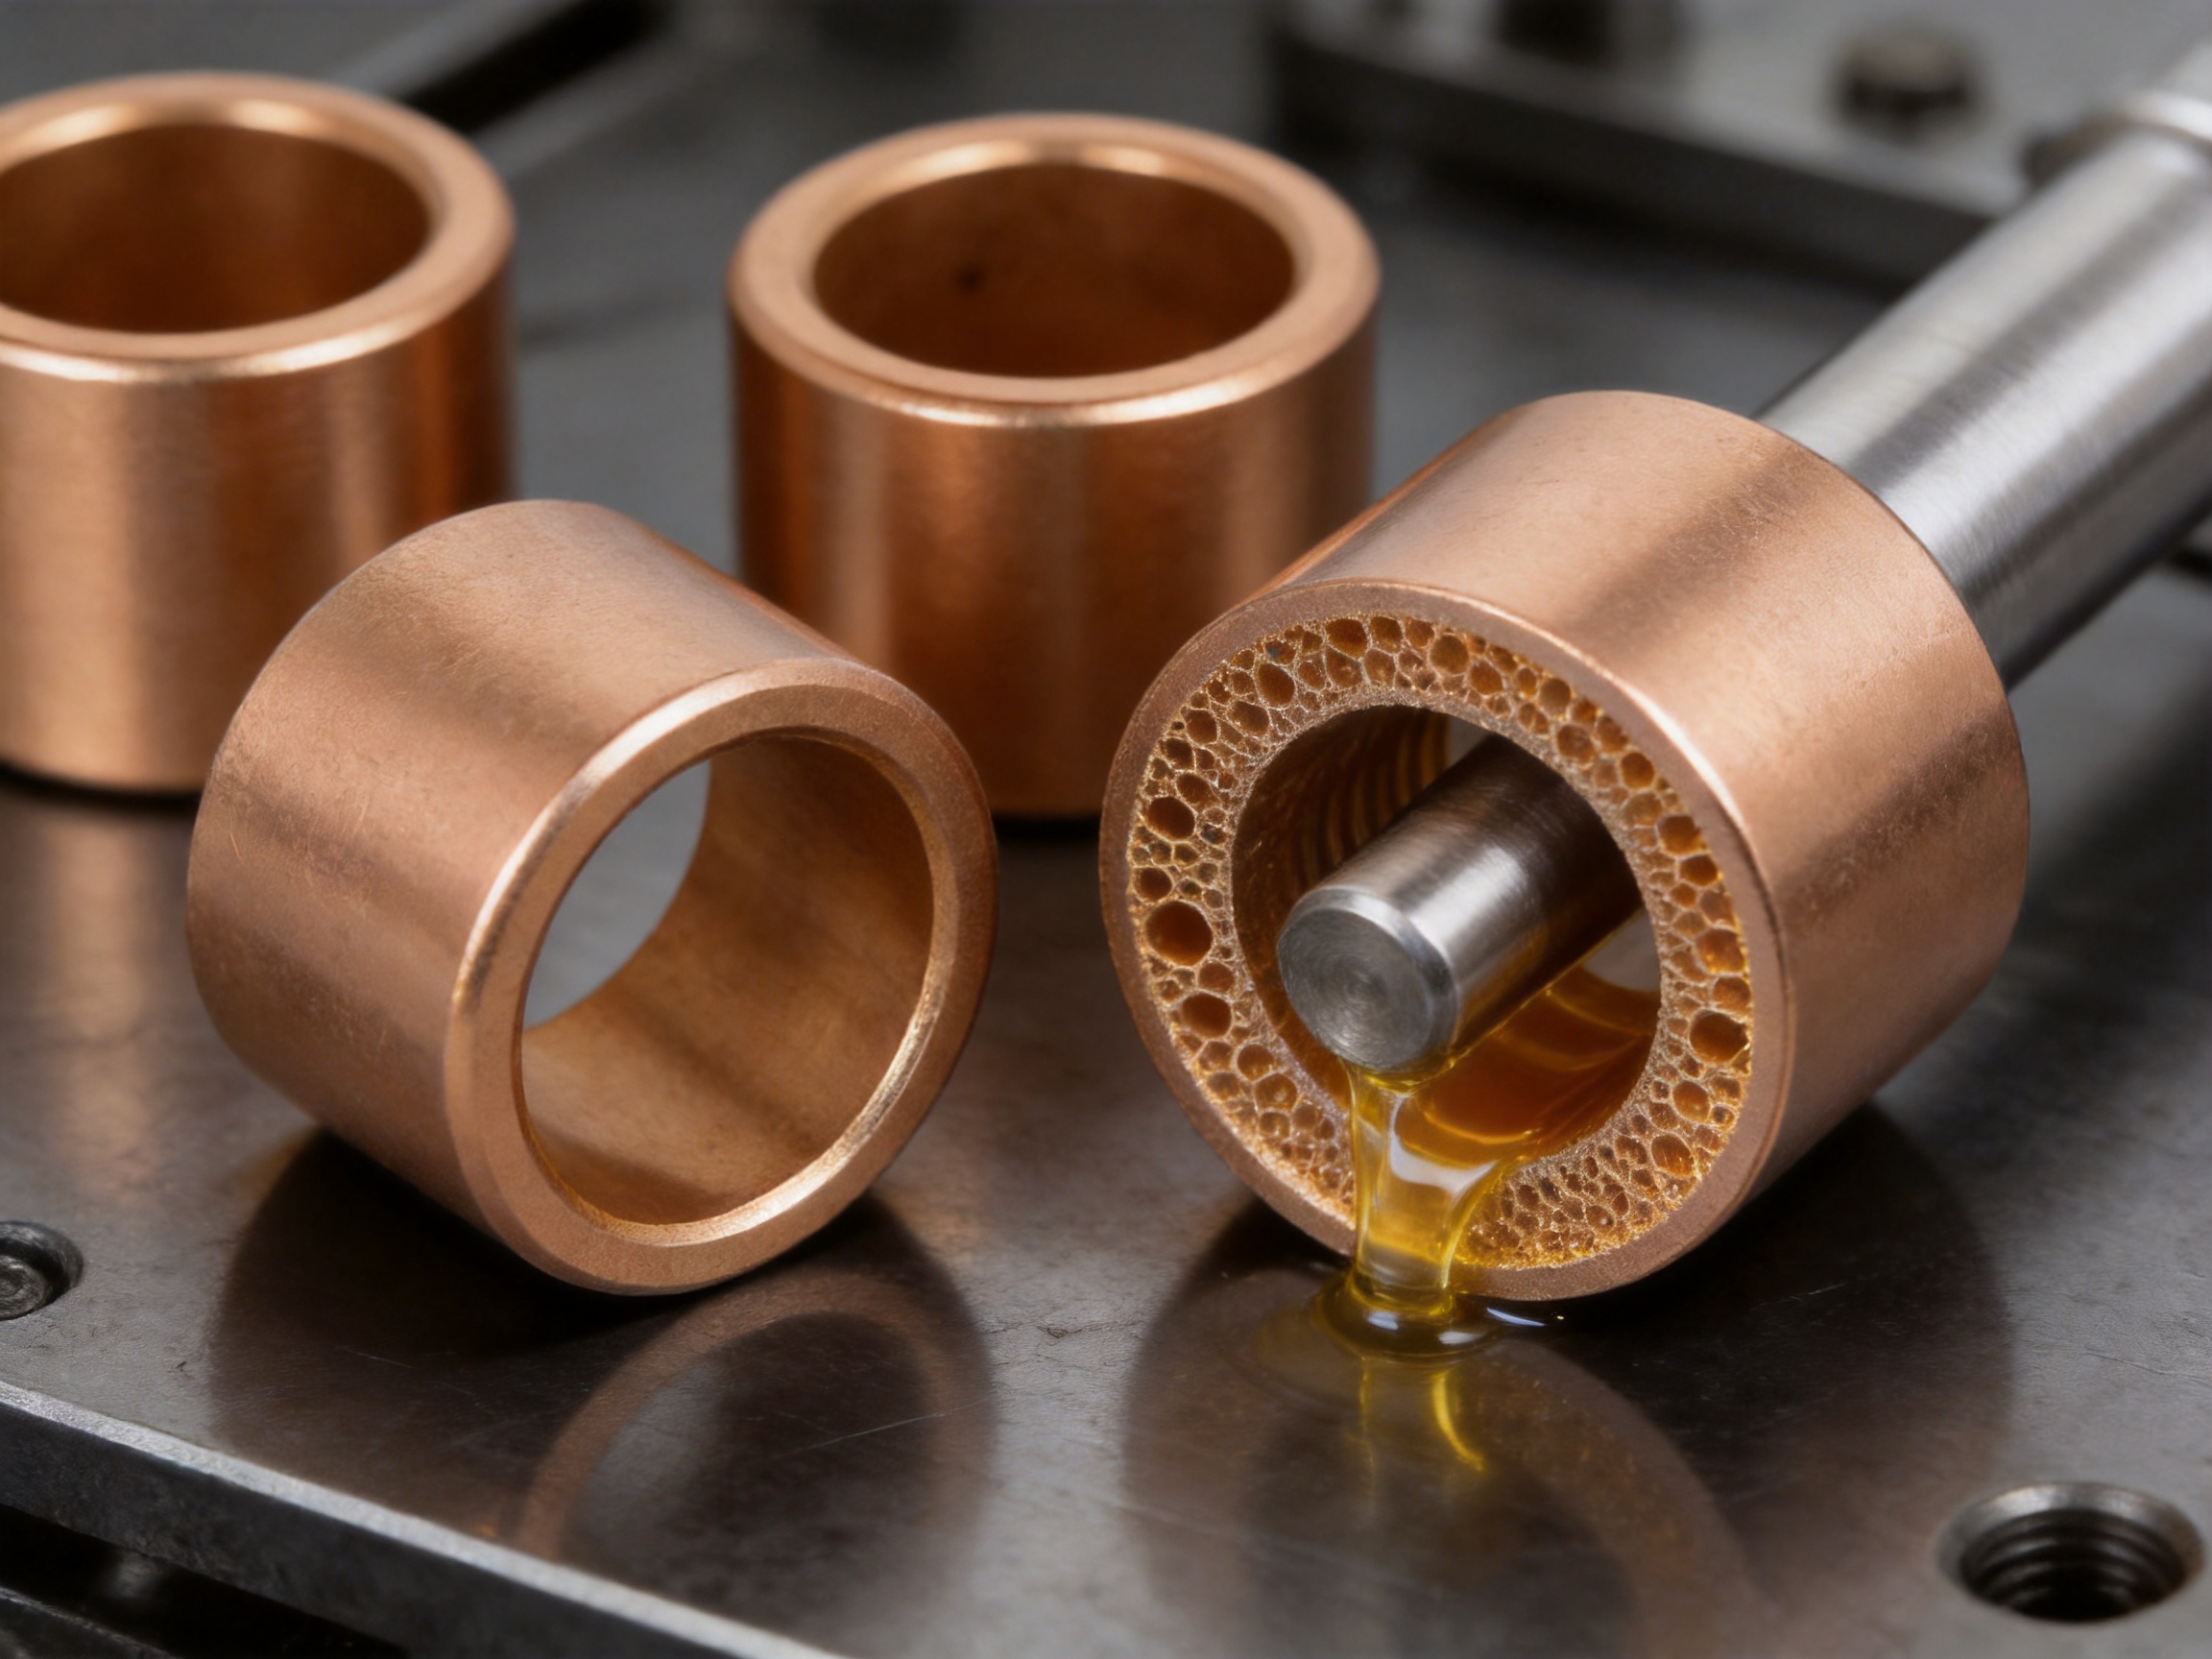
The self-lubricating function of the CuSn10 bushing is based on its interconnected porous structure. During powder metallurgy production, metal powder is compacted into the required shape and then heated below the alloy melting point. Sintering bonds the particles while preserving a controlled percentage of microscopic pores.
After sintering and sizing, the component is cleaned and placed into a vacuum oil impregnation process. The vacuum removes air from the pores. When the bushing is immersed in 46# mechanical oil under an approximately 80°C vacuum environment, the oil penetrates the available pore network. After cooling and atmospheric recovery, the oil remains stored inside the material.
During operation, frictional heat and contact pressure encourage a small quantity of oil to move toward the sliding interface. This replenishes the lubricating film and reduces the amount of external lubricant required. When the equipment stops, some oil can migrate back into the pore structure, allowing the bushing to retain a reserve of lubricant for subsequent operating cycles.
This mechanism is particularly useful in assemblies where regular lubrication is inconvenient, inaccessible, expensive, or likely to be neglected. It can also reduce the need for grease channels, external lubrication fittings, and frequent maintenance shutdowns.
Self-lubrication does not mean that the bushing is suitable for every operating condition without inspection. Load, speed, shaft surface finish, temperature, clearance, alignment, contamination, and duty cycle all influence service life. Applications involving extreme loads, very high speeds, aggressive chemicals, or elevated temperatures should be evaluated with specific operating data.
4. Advanced Powder Metallurgy Manufacturing Process
4.1 Raw Material Preparation
Production begins with the selection and inspection of copper-based alloy powder. Powder composition, particle size distribution, flowability, apparent density, and cleanliness affect the behavior of the material during compaction and sintering. For CuSn10 bushings, the copper-tin composition must be controlled consistently so that finished parts deliver stable mechanical and tribological performance.
Raw material inspection is carried out for each relevant batch. Composition and particle size testing help confirm that the powder conforms to the required internal specifications and applicable material standards. Controlling the raw powder at this stage helps prevent variation in density, porosity, weight, and dimensional shrinkage later in the process.
4.2 Precision Compaction
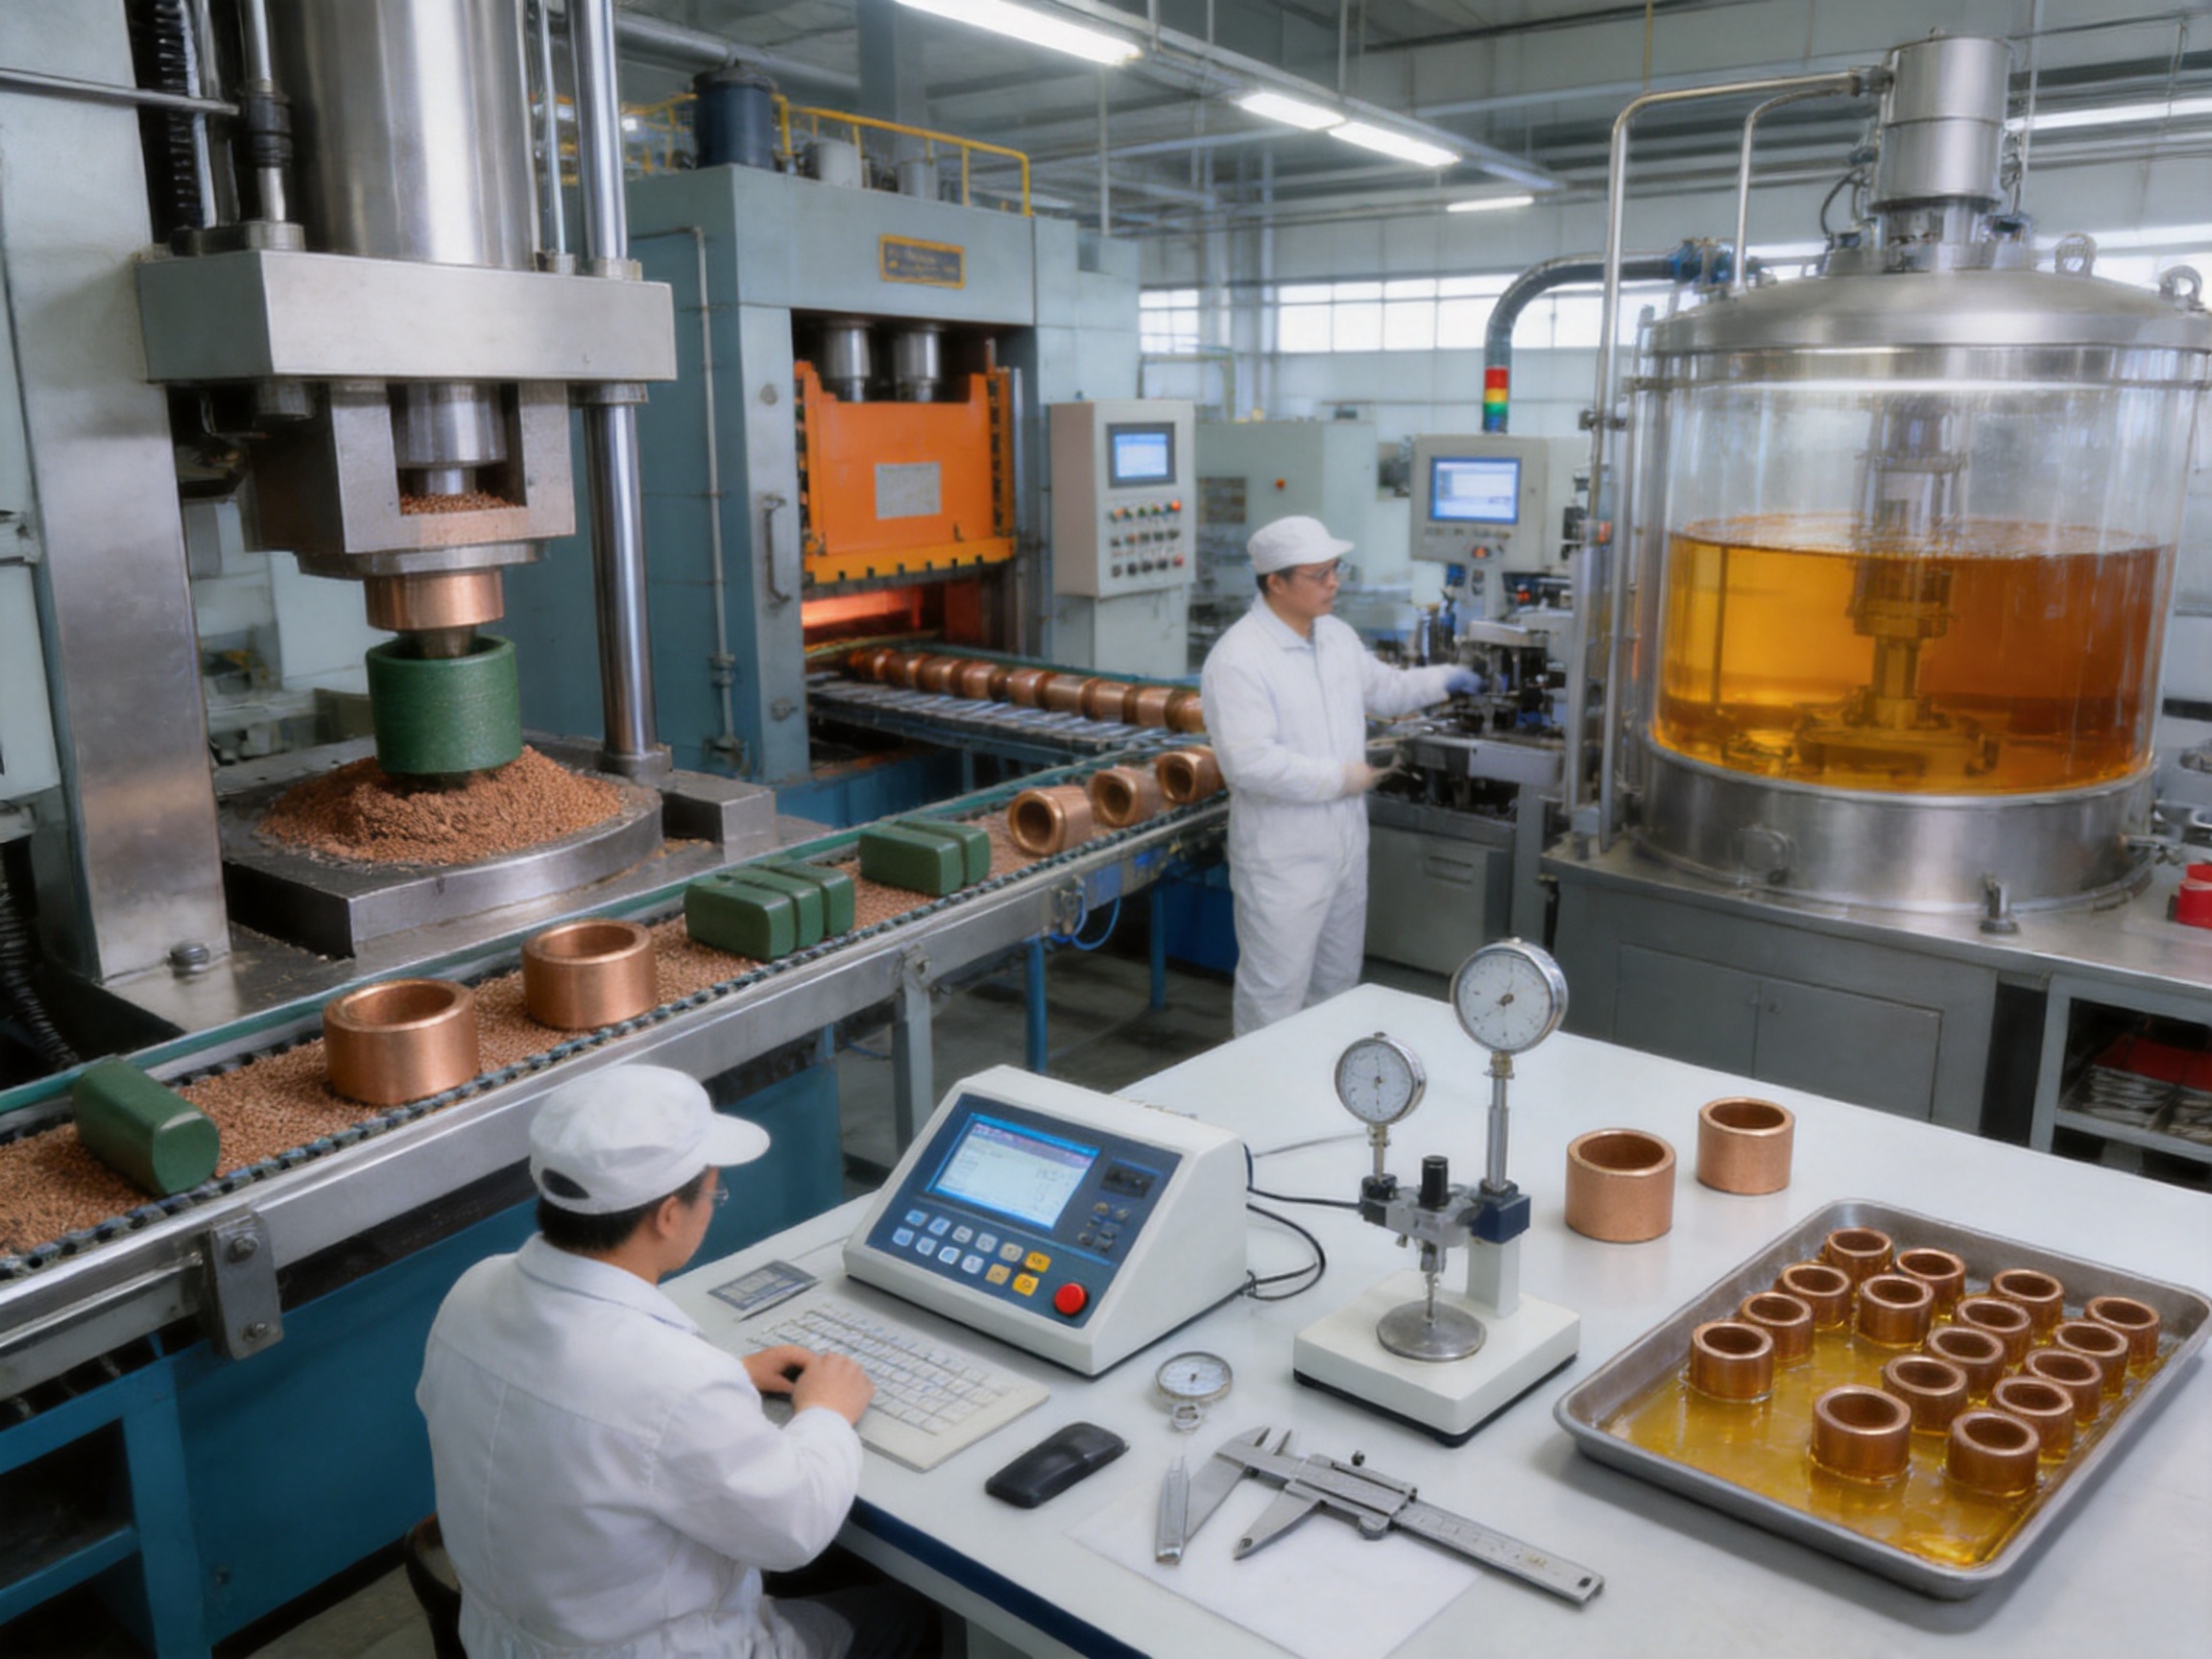
During compaction, measured powder is filled into a precision tool and compressed under controlled pressure. The powder is formed into the approximate geometry of the bushing, including the inner bore and outer cylindrical surface. Tool design and filling consistency are important because uneven powder distribution can cause density gradients, distortion, or cracking.
High-efficiency presses and precision forming equipment support repeatable production for both standard and customized components. The compaction process can be adjusted according to the required geometry, density range, wall thickness, and production volume.
Compared with machining a bushing from a solid bar, compaction can produce a near-net-shape component with less material waste. It is especially advantageous for larger production quantities, where tooling investment can be balanced against reduced machining time and improved consistency.
4.3 Controlled Sintering
The compacted part is initially known as a green compact. It has sufficient shape for handling but does not yet possess the final strength required for use. The green compact is heated in a controlled sintering furnace. For the A0667 product, the stated sintering parameter is TCI 690 ± 30°C.
During sintering, particles bond at their contact points, increasing the strength of the component while maintaining the designed porous structure. Temperature, heating rate, holding time, furnace atmosphere, and cooling conditions must be controlled carefully. Inconsistent sintering may lead to variations in hardness, dimensional change, density, pore connectivity, and wear performance.
A properly controlled sintering cycle provides a stable balance between structural integrity and oil storage capacity. The objective is not to eliminate all pores. Instead, the process must create a uniform and functional porous network while providing sufficient strength for the intended mechanical load.
4.4 Sizing and Precision Calibration
After sintering, the bushing may experience small dimensional changes. Sizing uses a precision tool to calibrate the inner and outer dimensions and improve geometric consistency. This operation is important for achieving the specified fit between the bushing, shaft, and housing.
For the A0667 bushing, key dimensional tolerances are controlled within approximately ±0.02 mm, with concentricity controlled to no more than 0.05 mm. These requirements support stable shaft rotation and reduce the risk of uneven contact.
Sizing also improves surface consistency and helps correct minor deformation caused by sintering. Depending on the design, additional machining or finishing may be performed to meet special drawing requirements, improve a surface feature, or create a customized geometry.
4.5 Cleaning Before Oil Impregnation
Before oil impregnation, the workpiece must be cleaned thoroughly. Powder residue, handling contamination, and loose particles can interfere with oil penetration or remain on the external surface. Cleaning contributes to stable impregnation and helps prevent unwanted oil stains during packaging.
The external surface is checked to ensure that the finished component is clean and suitable for assembly. Proper cleaning also supports reliable inspection because contamination can obscure surface defects or affect weight measurements.
4.6 Vacuum Oil Impregnation
The cleaned bushing is immersed in 46# mechanical oil for approximately 20 minutes in a vacuum environment at about 80°C. The vacuum helps remove air from the pores so that the oil can enter more effectively. Heating lowers the oil viscosity and supports penetration into the internal pore network.
After the impregnation cycle, the part is drained and cleaned on the outside. The objective is to retain oil inside the pores while avoiding excessive surface oil that could contaminate packaging, adjacent components, or the customer’s assembly line.
Vacuum impregnation distinguishes this product from many ordinary bronze or brass bushings. A dense machined sleeve may require continuous external lubrication, whereas the porous CuSn10 bushing is designed to store and release oil as part of its operating function.
4.7 Final Inspection and Packaging
Finished products undergo dimensional inspection and relevant performance checks before shipment. Packaging must protect the bushings from dust, impact, deformation, and contamination during storage and transportation. Clean packaging is particularly important for oil-impregnated parts because uncontrolled contamination may affect installation or early operating performance.
The complete manufacturing route integrates material control, forming technology, thermal processing, dimensional calibration, lubrication treatment, and inspection. This integrated approach provides greater consistency than relying on a single machining or casting operation.
5. Quality Control and Manufacturing Strengths
Jiande Welfine Technology Co., Ltd. was established in 2001 and specializes in powder metallurgy sintering, self-lubricating bushings, and precision components. The company operates a production base covering approximately 13,039 square meters and employs more than 150 skilled personnel.
The facility includes high-efficiency presses, high-temperature sintering furnaces, precision forming machines, and inspection equipment. This combination allows the company to manage the major stages of production internally and maintain better control over quality, delivery, and customization.
Welfine follows ISO 9001:2015 and IATF 16949:2016 quality management systems. These certifications support systematic control of processes, documentation, traceability, corrective actions, and continuous improvement. IATF 16949 experience is especially relevant to customers requiring automotive-level process discipline and stable batch performance.
| Quality Control Stage | Main Control Items | Purpose |
| Raw Material Inspection | Composition, particle size, powder characteristics | Confirm stable alloy and forming behavior |
| Tooling and Compaction | Powder filling, press parameters, green-part condition | Prevent density variation and forming defects |
| Sintering | Temperature, atmosphere, heating and cooling cycle | Control strength, shrinkage, and porosity |
| Sizing | Inner diameter, outer diameter, geometry | Improve dimensional consistency |
| Oil Impregnation | Vacuum, temperature, immersion time, surface cleanliness | Achieve stable oil retention and clean surfaces |
| Final Inspection | Dimensions, weight, density, hardness, wear performance | Verify compliance with product requirements |
| Packaging | Cleanliness, protection, identification | Prevent contamination and transport damage |
First-article inspection is used to verify that the initial parts meet the drawing and process requirements before full production continues. Online dimensional monitoring during compaction, sintering, and sizing helps identify process drift early. This reduces the risk of defective parts moving to subsequent operations.
Finished product inspection includes full dimensional inspection for applicable critical dimensions. Sampling checks may also cover density, hardness, and wear resistance. The combination of process inspection and final inspection is more effective than relying only on end-of-line testing because it addresses defects at their source.
6. Advantages Over Conventional Bushing Materials
6.1 Compared with Standard Brass Bushings
Standard brass bushings can be economical and easy to machine, but dense brass typically has limited oil-retention capability. If the external lubricant supply is interrupted, friction and wear may increase rapidly. The porous CuSn10 bushing stores oil within its structure and can gradually release it during operation.
CuSn10 bronze also offers a useful balance of hardness and wear resistance. In rotating or oscillating assemblies, this can help maintain a more stable sliding interface over a longer operating period. The exact performance depends on shaft material, load, speed, temperature, and clearance, but the material is generally better suited to self-lubricating applications than ordinary dense brass.
6.2 Compared with Fully Machined Solid Bronze
Fully machined solid bronze bushings can provide high mechanical strength and good wear resistance. However, they normally require external lubrication unless a separate solid lubricant or surface treatment is applied. Machining from bar stock can also generate a significant amount of material waste and require multiple cutting operations.
Powder metallurgy offers near-net-shape production and controlled porosity. This reduces material waste and can simplify production for repeat parts. It also enables the oil-impregnated structure that gives the bushing its self-lubricating function.
6.3 Compared with Cast Bronze Bushings
Cast bronze bushings can be suitable for large components and heavy-duty systems, but casting quality may be affected by shrinkage, segregation, inclusions, and other process variables. Additional machining is often required to achieve accurate dimensions and surface quality.
Powder metallurgy provides repeatable compaction and sintering conditions for smaller precision components. The process supports controlled density and dimensional consistency across high-volume production. It can also reduce secondary machining requirements and improve material utilization.
6.4 Compared with Polymer Bushings
Polymer bushings can provide low friction and corrosion resistance in selected environments, but their load capacity, thermal stability, and dimensional behavior may be limited by temperature and mechanical stress. CuSn10 bronze has a metallic structure that is better suited to many applications involving load, heat transfer, and repeated mechanical contact.
Material selection should always be based on actual operating conditions. Polymer, ceramic, steel-backed, or composite bushings may be more appropriate in certain environments. However, for applications requiring a combination of metallic strength, oil retention, dimensional accuracy, and self-lubrication, CuSn10 powder metallurgy bronze is a strong option.
7. Performance Benefits in Industrial Equipment
The product’s primary advantage is its ability to combine several desirable properties in one compact component. It provides a wear-resistant copper-based matrix, controlled porosity, retained lubricant, precision geometry, and scalable production.
Low friction helps reduce the energy required for movement and can support smoother operation. Reduced direct contact between the shaft and bushing also helps limit scoring and adhesive wear. Good thermal conductivity assists in moving heat away from the sliding area, while the bronze structure provides resistance to many common mechanical environments.
The bushing can also reduce maintenance requirements. If the product is correctly selected and installed, the internal oil reserve can support extended operation without frequent manual lubrication. This is valuable for machinery with numerous bushings, difficult-to-access components, or long service intervals.
Dimensional accuracy is equally important. A bushing with excessive clearance may cause vibration, noise, impact loading, and unstable motion. A bushing with insufficient clearance may experience binding, overheating, or difficult assembly. Controlled sizing and concentricity help the component achieve the intended fit.
8. Application Areas
8.1 Automotive Components
Automotive assemblies use bushings in mechanisms involving rotation, pivoting, guidance, and vibration control. The CuSn10 bushing can be considered for selected engine, chassis, transmission, actuator, and accessory applications where oil retention and wear resistance are required.
Automotive environments may include temperature changes, vibration, dust, oil exposure, and repeated start-stop cycles. The bushing design must therefore be matched to the specific component, load profile, speed, and temperature range. When these conditions are within the material’s capability, the oil-impregnated structure can support stable operation and reduced maintenance.
8.2 Precision Machine Tools
Machine tools require accurate movement and stable alignment. Bushings may be used to guide shafts, support rotating members, or reduce friction in auxiliary mechanisms. The specified concentricity and dimensional control of the A0667 product support applications where precise fit and repeatable movement are important.
Clean assembly, correct clearance, and protection from abrasive contamination are essential for machine tool applications. Even a high-quality bushing can experience premature wear if chips, dust, or abrasive particles enter the sliding interface.
8.3 Hydraulic Pumps and Valve Assemblies
Hydraulic systems depend on accurate movement, pressure stability, and reliable component alignment. Bushings can guide shafts, support rotating parts, and maintain the position of moving elements in pump and valve assemblies.
CuSn10 bronze offers good wear resistance and dimensional stability for many hydraulic applications. However, compatibility with hydraulic fluid, pressure, speed, and temperature should be verified before use. Where the bushing is exposed directly to a specialized fluid, the impregnation oil and material must be evaluated for compatibility.
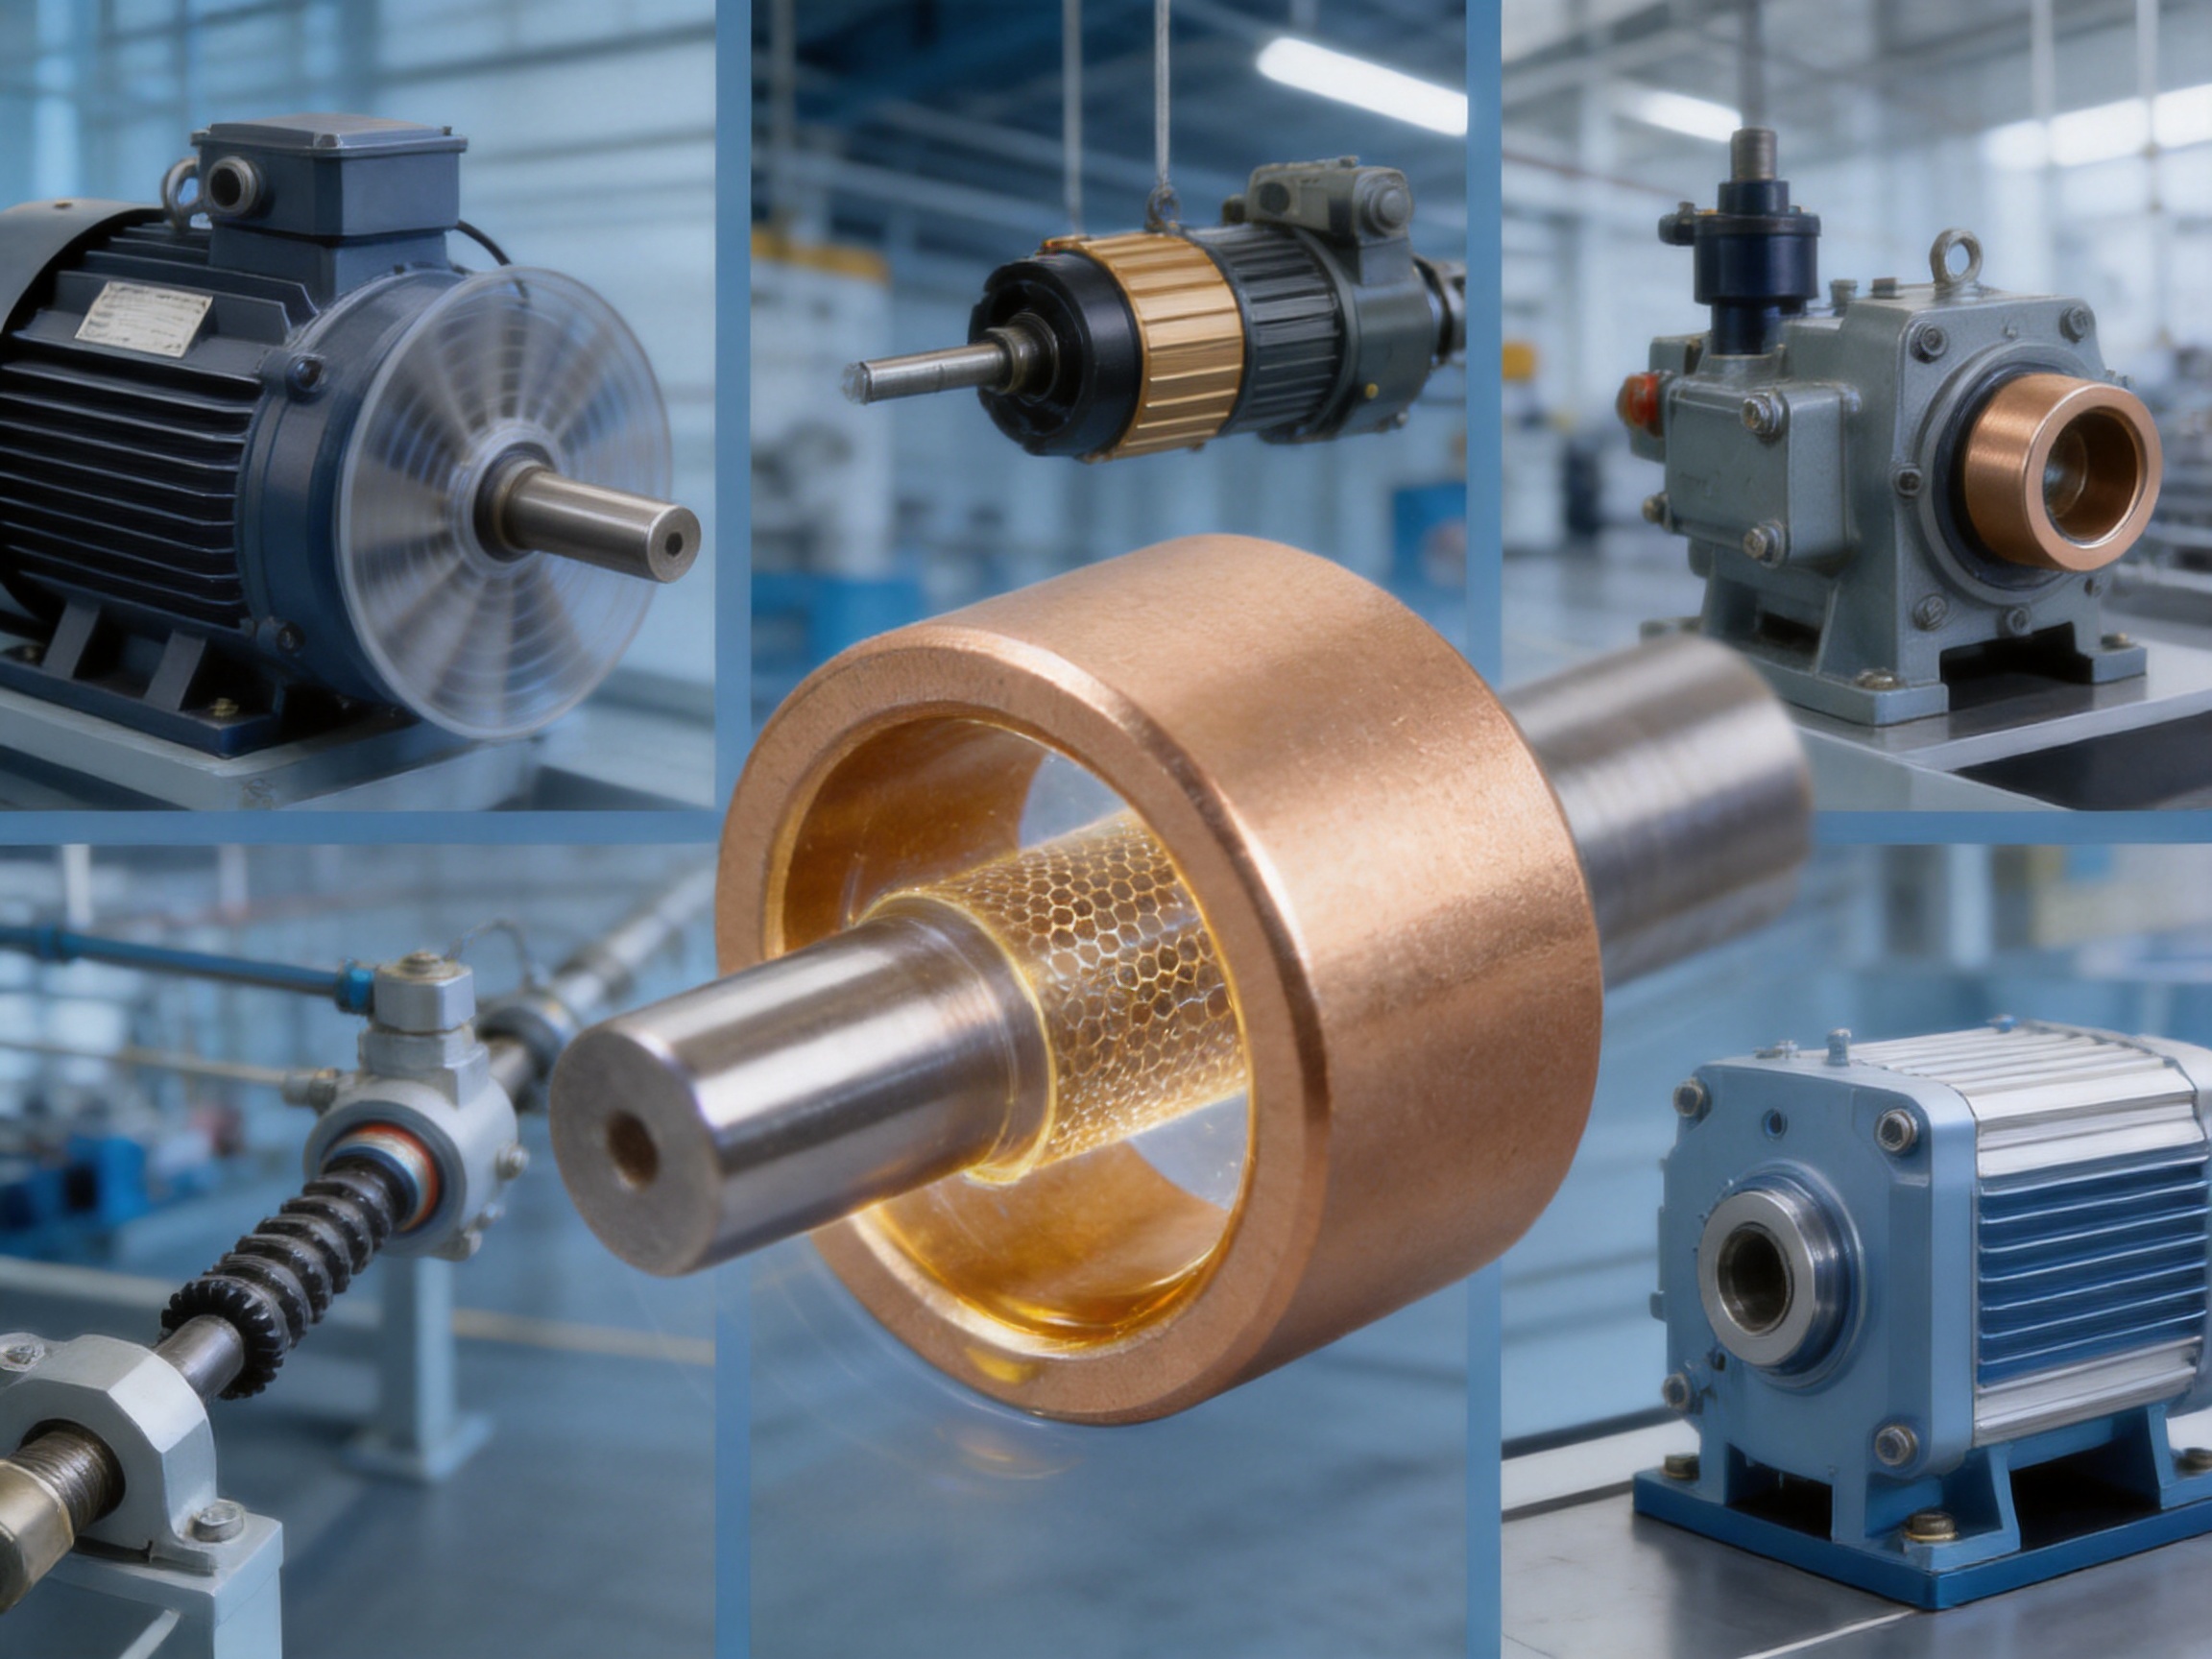
8.4 Electric Motors and Fans
Electric motors and fans often operate for long periods with continuous shaft rotation. The bushing must maintain a stable sliding surface, manage heat, and resist wear. Oil-impregnated bronze can be advantageous in applications where routine grease application is inconvenient.
Fans, blowers, and refrigeration equipment may contain rotating assemblies that require compact and quiet support components. A properly fitted CuSn10 bushing can help reduce friction and support long-term operation. Speed limits and temperature conditions should be confirmed for each design.
8.5 Refrigeration and Household Appliances
Household appliance transmission structures often require small, economical, and reliable bushings. Powder metallurgy is well suited to the production of repeat components with controlled dimensions and consistent performance.
The low-maintenance characteristics of oil-impregnated bushings can be beneficial in appliances that are not designed for regular service lubrication. Application engineers should consider noise requirements, operating cycle, load, temperature, and possible contact with cleaning agents or moisture.
8.6 Agricultural Machinery
Agricultural machinery may operate in dusty, humid, and contaminated environments. It can also experience frequent starts, stops, impacts, and load changes. The CuSn10 bushing’s oil-retaining structure and wear resistance can support many pivoting and transmission applications.
Contamination control remains important. Seals, protective covers, correct installation, and periodic inspection can help prevent abrasive particles from entering the bearing interface. The bushing should be selected according to the actual load and environmental conditions rather than relying only on nominal dimensions.
8.7 Automation and Construction Machinery
Automation systems require predictable movement and high dimensional repeatability. Bushings may be used in linear guides, linkages, indexing mechanisms, and motion assemblies. Powder metallurgy production supports consistent batches for equipment manufacturers producing multiple machines.
Construction machinery places greater demands on bushings because of high impact, vibration, and load. CuSn10 powder metallurgy bushings may be suitable for selected medium-load joints and guided components, while extremely severe articulation points may require a different bronze grade, solid lubricant system, or heavy-duty composite design.
| Industry | Typical Bushing Location | Main Performance Requirement |
| Automotive | Chassis, actuators, accessories | Wear resistance and dimensional stability |
| Electric Motors | Shaft support | Low friction and long operating life |
| Hydraulic Equipment | Pump and valve guide components | Precision and load capacity |
| Machine Tools | Guide and support mechanisms | Concentricity and controlled clearance |
| Fans and Refrigerators | Rotating transmission components | Quiet operation and low maintenance |
| Agricultural Machinery | Pivot and transmission systems | Wear resistance and contamination tolerance |
| Automation Equipment | Motion assemblies | Repeatability and smooth movement |
| Construction Machinery | Selected joints and guides | Impact resistance and load support |
9. Design and Selection Considerations
Selecting a bushing requires more than matching the inner and outer diameters. Engineers should evaluate load, speed, temperature, lubrication, shaft material, surface finish, housing material, installation method, environment, and expected duty cycle.
Load affects the pressure applied to the projected bearing area. Speed influences frictional heat and the rate at which lubricant is consumed. Temperature affects oil viscosity, dimensional clearance, and the strength of the bronze matrix. A high-load, low-speed oscillating application may require a different design approach from a high-speed continuous rotation application.
Shaft hardness and surface finish also influence service life. A rough or soft shaft may damage the bushing, while a properly finished shaft can support a stable lubricating film. Alignment must be controlled because angular misalignment can concentrate pressure on one edge of the bushing.
Housing fit is equally important. An excessive interference fit can reduce the internal clearance, while an insufficient fit can allow the bushing to move in the housing. Installation tools should apply force evenly and should not damage the bore or chamfer.
Environmental factors include dust, moisture, chemicals, vibration, shock, and exposure to external oils or fluids. In contaminated environments, seals and protective structures may be needed. In high-temperature applications, the retained oil and material properties must be reviewed carefully.
10. Custom Manufacturing and OEM Support
Different machines require different bushing dimensions, shapes, materials, oil types, clearances, and performance targets. Welfine provides OEM and ODM services based on customer drawings, samples, and technical requirements.
Customization can include inner and outer diameter changes, length adjustments, chamfer modifications, stepped or flanged geometries, special tolerances, different copper-based materials, alternative porosity levels, and application-specific oil impregnation requirements. Small-batch prototyping and mass production are both supported.
The recommended information for a quotation includes a technical drawing or sample, material requirement, annual demand, application description, load, speed, temperature, shaft and housing specifications, lubrication conditions, inspection standards, and packaging requirements.
When drawings are not available, a physical sample can provide useful information for reverse engineering and development. The manufacturer can evaluate the sample’s dimensions, material, density, oil content, and operating requirements before proposing a production route.
For standard orders, the stated delivery period is generally 7–15 working days, while urgent orders may receive priority production support depending on tooling, material availability, and production scheduling. International delivery can be arranged through express, air freight, or sea freight channels.
11. Installation and Maintenance Recommendations
Before installation, inspect the bushing, shaft, and housing for burrs, dirt, dents, and damage. The housing bore should be clean and correctly aligned. The shaft should have a suitable surface finish and should not contain sharp edges that could scrape the bushing during assembly.
Use an appropriate press or installation tool that contacts the bushing evenly. Do not apply installation force through a thin wall or use impact methods that may deform the component. The chamfer should face the entry direction when applicable.
After installation, confirm that the shaft rotates or moves smoothly. Check for abnormal resistance, noise, binding, or excessive radial play. If the bushing is installed into a housing with a significant interference fit, verify that the final inner diameter remains within the required clearance range.
Although the oil-impregnated structure reduces lubrication requirements, inspection is still recommended. Look for unusual noise, temperature rise, vibration, discoloration, scoring, or changes in operating clearance. These signs may indicate misalignment, overload, contamination, insufficient clearance, or an unsuitable operating condition.
Additional lubricant should not be introduced automatically without confirming compatibility. Excessive or incompatible lubricant may alter friction behavior, wash out the impregnated oil, attract contaminants, or affect seals and adjacent components.
12. How Product Quality Is Evaluated
A reliable CuSn10 powder metallurgy bushing should be evaluated through a combination of material, dimensional, structural, and functional criteria. No single test provides a complete picture of quality.
Material verification confirms the copper-tin composition and helps ensure that the correct powder has been used. Density measurement provides information about compaction and porosity. Weight consistency can help identify filling or dimensional variation in small components.
Dimensional inspection should cover the inner diameter, outer diameter, length, chamfer, roundness, and concentricity where relevant. These values must be checked using calibrated equipment and appropriate measurement methods.
Hardness and wear testing can provide information about the mechanical and tribological behavior of the material. Oil content and impregnation effectiveness may also be assessed when required by the application.
Visual inspection should identify cracks, chips, deformation, excessive surface oil, contamination, burrs, and other defects. For critical applications, customers may request additional documentation, batch traceability, capability studies, or special inspection plans.
13. Why Process Integration Matters
The performance of a self-lubricating bushing depends on the interaction of multiple process variables. A correct alloy with poor density control may not deliver stable results. Accurate dimensions without proper oil impregnation may produce a dry-running component. Effective impregnation without adequate strength may lead to deformation under load.
Integrated production allows the manufacturer to connect these variables. Powder characteristics influence compaction. Compaction influences green density. Green density and furnace conditions influence sintering shrinkage and porosity. Sizing affects final clearance. Cleaning and vacuum impregnation determine oil retention. Final inspection verifies whether the complete process has delivered the intended result.
This is one of the major strengths of an experienced powder metallurgy manufacturer. Rather than treating each operation as an isolated service, the company can optimize the complete manufacturing chain and make adjustments based on measured production data.
14. Sustainability and Cost Efficiency
Powder metallurgy can reduce material waste because components are formed close to their final geometry. Compared with machining a bushing from a larger solid bar, the process may require less cutting and produce fewer chips. This supports efficient use of copper-based materials, which can be relatively costly.
Mass production also benefits from repeatable tooling and automated or semi-automated pressing. Once the process has been validated, large quantities can be produced with consistent dimensions and reduced labor per part.
The self-lubricating function may provide additional lifecycle benefits. Reduced external lubrication can lower lubricant consumption, decrease service labor, and reduce equipment downtime. The actual savings depend on the application, but the potential is significant in machinery containing many bushings or components that are difficult to access.
Economic performance should be evaluated over the complete service life rather than through purchase price alone. A lower-cost bushing that requires frequent replacement or lubrication may become more expensive than a precisely manufactured oil-impregnated component with longer service intervals.
15. Future Development of Powder Metallurgy Bushings
Industrial equipment is moving toward greater automation, compact design, higher efficiency, and reduced maintenance. These trends are increasing demand for bushings that can operate reliably with minimal external lubrication and tight dimensional control.
Future development is expected to focus on improved pore structure, optimized alloy formulations, higher load capacity, better thermal performance, and more application-specific impregnation oils. Manufacturing systems are also becoming more data-driven, with enhanced monitoring of powder filling, press force, furnace conditions, sizing accuracy, and final inspection results.
Emerging applications may include electric vehicles, electric tools, intelligent manufacturing equipment, robotic mechanisms, compact actuators, renewable energy equipment, and advanced production lines. These applications require small components that offer predictable performance and long service life.
CuSn10 powder metallurgy bronze remains well positioned for this development because it combines the established advantages of copper-tin bronze with the controlled porosity and efficient production capabilities of powder metallurgy.
16. Frequently Asked Questions
Can the CuSn10 powder metallurgy bronze bushing operate without regular manual lubrication?
Under suitable operating conditions, the oil stored in the porous structure can provide continuous lubrication and significantly reduce the need for manual lubrication. However, the bushing is not maintenance-free in every application. Periodic inspection is recommended, especially under high loads, elevated temperatures, contamination, or continuous operation.
Is CuSn10 suitable for high-speed rotating equipment?
CuSn10 bushings can be used in many medium- and high-speed applications, provided that the load, speed, clearance, temperature, shaft finish, and lubrication conditions remain within the design limits. The specific operating envelope should be confirmed through application analysis or testing.
What is the main difference between a powder metallurgy bronze bushing and a cast bronze bushing?
A powder metallurgy bushing has a controlled porous structure that can retain lubricating oil. It also offers strong dimensional consistency and efficient mass production. A cast bronze bushing is generally denser and may provide high mechanical strength, but it normally requires external lubrication unless it includes a special lubricant system.
Why is vacuum used during oil impregnation?
Vacuum removes air from the internal pores of the sintered material. When the bushing is immersed in heated oil, the reduced internal pressure helps the oil penetrate the pore network more completely. After the vacuum is released, the oil remains stored inside the component.
What does the 5.7–5.8 g/cm³ density specification indicate?
The density range reflects the balance between the metallic structure and the designed pore volume. It is an important process-control value because density influences mechanical strength, oil retention, dimensional stability, and wear behavior.
What is the purpose of the 0.4 × 45° chamfer?
The chamfer guides the bushing into the housing during installation, reduces the risk of edge interference, and removes a sharp edge that could damage the mating component or complicate assembly.
Can the bushing be customized according to a drawing?
Yes. Custom dimensions, materials, chamfers, tolerances, oil impregnation requirements, and packaging conditions can be developed according to customer drawings, samples, or technical specifications. OEM and ODM services are available for prototypes, small batches, and mass production.
What information is needed to select the correct bushing?
Important information includes shaft diameter, housing diameter, bushing length, radial load, rotational or oscillating speed, operating temperature, duty cycle, shaft material and finish, environmental conditions, installation method, and required service life.
How can premature bushing wear be prevented?
Use the correct clearance, maintain proper shaft alignment, keep the assembly clean, avoid excessive loads, protect the component from abrasive contamination, and ensure that the shaft surface finish is appropriate. Correct installation is also essential because deformation or misalignment can rapidly increase wear.
Does oil impregnation leave the outside of the bushing oily?
The impregnation process is followed by draining and surface cleaning. The purpose is to retain oil within the pores while minimizing surface oil, allowing the component to be packaged and handled more cleanly.
What quality certifications support production capability?
Jiande Welfine Technology Co., Ltd. operates under ISO 9001:2015 and IATF 16949:2016 quality management systems. These systems support documented process control, traceability, inspection, corrective action, and continuous improvement.
Are these bushings appropriate for hydraulic systems?
They can be suitable for selected hydraulic pump, valve, and guide applications. Fluid compatibility, pressure, speed, temperature, and dimensional clearance must be evaluated before approval. The impregnation oil and hydraulic medium should also be checked for compatibility.
What delivery support is available for customized products?
Quotation is available based on drawings or samples, and standard orders are generally delivered within 7–15 working days depending on specifications and production scheduling. International express, air freight, and sea freight options can be arranged.
17. Conclusion
The CuSn10 powder metallurgy bronze bushing provides a practical solution for machinery that requires wear resistance, dimensional accuracy, reliable oil retention, and reduced lubrication maintenance. Its copper-tin bronze matrix supports mechanical durability and heat transfer, while the controlled porous structure stores and releases oil during operation.
The A0667 specification demonstrates the product’s precision-oriented design, including controlled density, weight, concentricity, chamfer geometry, and dimensional tolerance. The integrated manufacturing route of compaction, sintering, sizing, cleaning, vacuum oil impregnation, inspection, and packaging ensures that each performance characteristic is supported by a defined process.
Compared with conventional brass, fully machined bronze, and ordinary cast bushings, the product offers advantages in self-lubrication, material utilization, production consistency, and maintenance reduction. Its application range includes automotive components, electric motors, fans, refrigeration equipment, hydraulic systems, precision machinery, automation equipment, agricultural machinery, and selected construction machinery.
With more than 20 years of powder metallurgy experience, a modern production base, specialized equipment, skilled personnel, and ISO 9001:2015 and IATF 16949:2016 quality systems, Jiande Welfine Technology Co., Ltd. can provide customized CuSn10 bushing solutions based on drawings, samples, and application requirements.
For equipment manufacturers seeking a reliable balance between performance, production efficiency, and lifecycle cost, the CuSn10 powder metallurgy bronze bushing is a strong candidate for precision self-lubricating applications.
References
1. Powder Metallurgy Materials and Processes, technical reference literature on powder compaction, sintering, density control, and porous metal structures.
2. Copper Development Association, technical information on copper-tin bronze alloys, wear behavior, thermal conductivity, and engineering applications.
3. International Organization for Standardization, ISO 9001:2015 Quality Management Systems: Requirements.
4. International Automotive Task Force, IATF 16949:2016 Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
5. General engineering references on oil-impregnated bearings, porous bronze bushings, lubrication mechanisms, shaft clearances, and sliding-contact design.
6. Manufacturer technical data for CuSn10 powder metallurgy bronze bushing, product code A0667, including dimensional, density, oil impregnation, and inspection requirements.
Product: Powder Metallurgy Bronze Bushing (A0667)
Related products
-
-
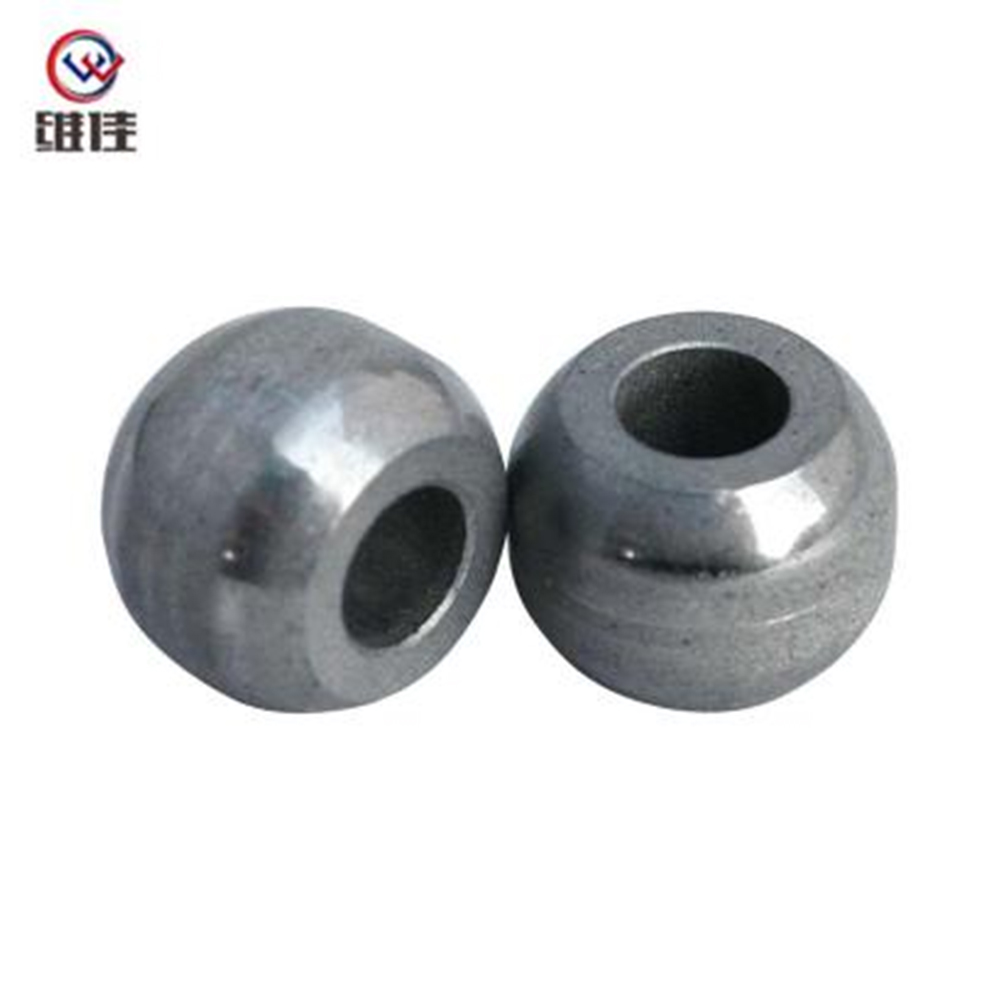
Product Description: High-precision powder metallurgy part (S14*7*10) made of iron material from Jiande Wefine, customized PM components with strict tolerance control.
See Details -
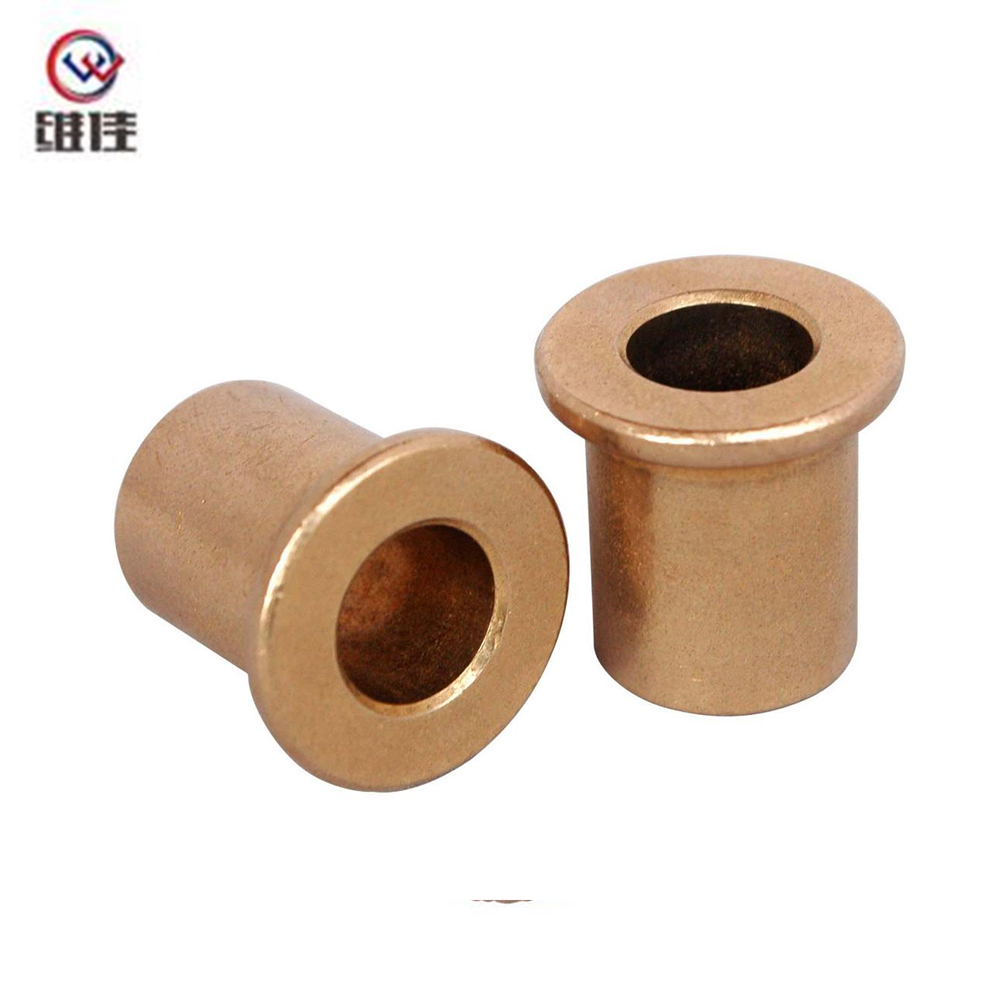
This copper-based powder metallurgy bushing is manufactured through an integrated process of compaction, sintering, sizing, and oil impregnation. It features excellent wear resistance and self-lubrica...
See Details
Copyright © Jiande Welfine Technology Co., Ltd. All Rights Reserved. Custom Self-lubricating Sintered Bushing Manufacturers
