E-mail us: [email protected]
Tel: +86-15239857375
 English
 中文简体


 Home / Author / Luo Qian — Product Sales Supervisor / CuSn10 Powder Metallurgy Bronze Bushing: High-Precision Self-Lubricating Performance for Industrial Machinery
CuSn10 Powder Metallurgy Bronze Bushing: High-Precision Self-Lubricating Performance for Industrial Machinery
 2026.11.05
 Luo Qian — Product Sales Supervisor
Content
- 1 1. Product Overview
- 2 2. Why CuSn10 Bronze Is Suitable for Bushings
- 3 3. How the Self-Lubricating Structure Works
- 4 4. Manufacturing Process from Powder to Finished Bushing
- 5 5. Quality Control and Inspection Strengths
- 6 6. Advantages over Conventional Machined or Cast Bushings
- 7 7. Application Areas
- 8 8. Installation and Operating Considerations
- 9 9. Customization and OEM/ODM Capabilities
- 10 10. Manufacturing Infrastructure and Company Strengths
- 11 11. How to Select the Correct CuSn10 Bushing
- 12 12. Frequently Asked Questions
- 12.1 What is a CuSn10 powder metallurgy bronze bushing?
- 12.2 What does the CuSn10 designation mean?
- 12.3 Can the bushing operate without regular lubrication?
- 12.4 Is this bushing suitable for high-speed equipment?
- 12.5 How does it differ from a cast bronze bushing?
- 12.6 How does it differ from a machined solid bronze bushing?
- 12.7 What is the purpose of the 0.4 × 45-degree chamfer?
- 12.8 What does the 0.05 mm concentricity requirement indicate?
- 12.9 Can the product be customized?
- 12.10 What information should be provided for a quotation?
- 12.11 How long is the usual delivery time?
- 12.12 What after-sales support is available?
- 13 13. Conclusion
- 14 References
- 15 Product: Powder Metallurgy Bronze Bushing (A0667)
Modern machinery increasingly depends on compact, reliable, and maintenance-efficient bearing components. Bushings may be small compared with the equipment in which they are installed, but their influence on operating stability, service life, noise, energy consumption, and maintenance cost is substantial. A properly selected bushing must support moving shafts, control friction, tolerate load and vibration, maintain dimensional accuracy, and continue operating under conditions where regular lubrication may be difficult.
The CuSn10 powder metallurgy bronze bushing is designed to address these requirements through a combination of copper-based alloy performance, controlled porosity, precision forming, sintering, sizing, and oil impregnation. Manufactured from CuSn10 bronze powder, the bushing provides a wear-resistant matrix with pores capable of retaining and releasing lubricating oil during operation. This structure helps create a self-lubricating bearing surface that can reduce friction and maintenance requirements in many industrial applications.
Product code A0667 represents a precision CuSn10 powder metallurgy bronze bushing with a specification of 10G7 × 13s7 × 10 mm. Its controlled dimensions, chamfered edges, defined density range, and concentricity requirement make it suitable for demanding assemblies in precision machinery, automotive components, hydraulic systems, fans, refrigerators, and other mechanical equipment.
Beyond the material itself, product quality depends on manufacturing discipline. The production route includes powder preparation, compaction, sintering, sizing, precision inspection, vacuum oil impregnation, cleaning, and packaging. Each stage affects the final bearing's density distribution, porosity, dimensional stability, mechanical strength, oil-retention capability, and service life.
This article examines the construction, performance, manufacturing process, quality controls, application advantages, customization capabilities, and selection considerations associated with CuSn10 powder metallurgy bronze bushings.
1. Product Overview
The A0667 bushing is a copper-based powder metallurgy component manufactured from CuSn10 material. CuSn10 is a tin bronze containing approximately 10 percent tin, with the balance primarily copper. The alloy is valued for its combination of wear resistance, load-carrying capability, corrosion resistance, thermal conductivity, and compatibility with lubricated sliding applications.
Unlike a fully dense machined sleeve, a sintered bronze bushing contains a carefully controlled network of interconnected pores. These pores are filled with lubricating oil during the impregnation process. When the bushing operates, heat and friction encourage oil to migrate toward the sliding interface. When the component cools or stops, some of the oil can return to the pore structure. This dynamic behavior supports long-term lubrication and reduces the need for frequent external oil application.
| Product Item | Specification |
| Product name | Powder Metallurgy Bronze Bushing |
| Product code | A0667 |
| Material | CuSn10 |
| Nominal specification | 10G7 × 13s7 × 10 mm |
| Chamfer | 0.4 × 45 degrees |
| Weight | 3.36–3.41 g |
| Density | 5.7–5.8 g/cm³ |
| Concentricity | Not more than 0.05 mm |
| Sintering parameter | TCI 690 ± 30 degrees Celsius |
| Impregnation medium | 46# mechanical oil |
The dimensional specification is intended for controlled assembly conditions. The G7 and s7 tolerance designations indicate that the internal and external dimensions are manufactured for a defined fit relationship. Actual operating clearance must still be evaluated according to shaft material, shaft diameter, rotational speed, load, temperature, and lubrication conditions.
2. Why CuSn10 Bronze Is Suitable for Bushings
The performance of a bushing begins with its material system. Copper-based alloys are widely used in sliding bearings because they combine good thermal conductivity with favorable friction and wear characteristics. Copper transfers heat away from the contact zone, while tin improves hardness, wear resistance, and resistance to deformation compared with many softer copper materials.
CuSn10 offers a practical balance between load capacity and sliding performance. The tin content strengthens the bronze matrix and improves resistance to adhesive wear. This is important when the bushing operates under repeated rotation, oscillation, intermittent motion, or start-stop conditions.
The alloy is also suitable for applications exposed to moderate moisture, industrial contamination, or changing environmental conditions. Although no bearing material is immune to corrosion or contamination, CuSn10 bronze generally provides better corrosion resistance than ordinary ferrous materials and can maintain stable performance in a wide range of mechanical assemblies.
Thermal conductivity is another important advantage. Friction generates heat at the shaft-bushing interface. If that heat remains concentrated, the lubricant may degrade and the clearance may change. A copper-based matrix can help distribute heat through the component and into the surrounding housing, supporting more stable operating conditions.
CuSn10 is particularly valuable when an application requires more wear resistance than standard brass can provide. Brass may perform effectively in light-duty conditions, but it may offer lower load capacity, weaker oil retention, and shorter service life in continuous sliding applications. The CuSn10 powder metallurgy structure addresses these limitations by combining a stronger bronze matrix with oil-retaining pores.
| Performance Factor | CuSn10 Powder Metallurgy Bronze | Common Brass Bushing |
| Wear resistance | High | Moderate |
| Load-carrying capability | High for suitable operating conditions | Moderate |
| Oil retention | Excellent because of controlled porosity | Low in fully dense material |
| Friction control | Supported by impregnated oil | Usually depends more heavily on external lubrication |
| Dimensional repeatability | High when pressing, sizing, and inspection are controlled | Dependent on machining quality |
| Mass-production efficiency | High for repeat components | Often requires more material removal |
3. How the Self-Lubricating Structure Works
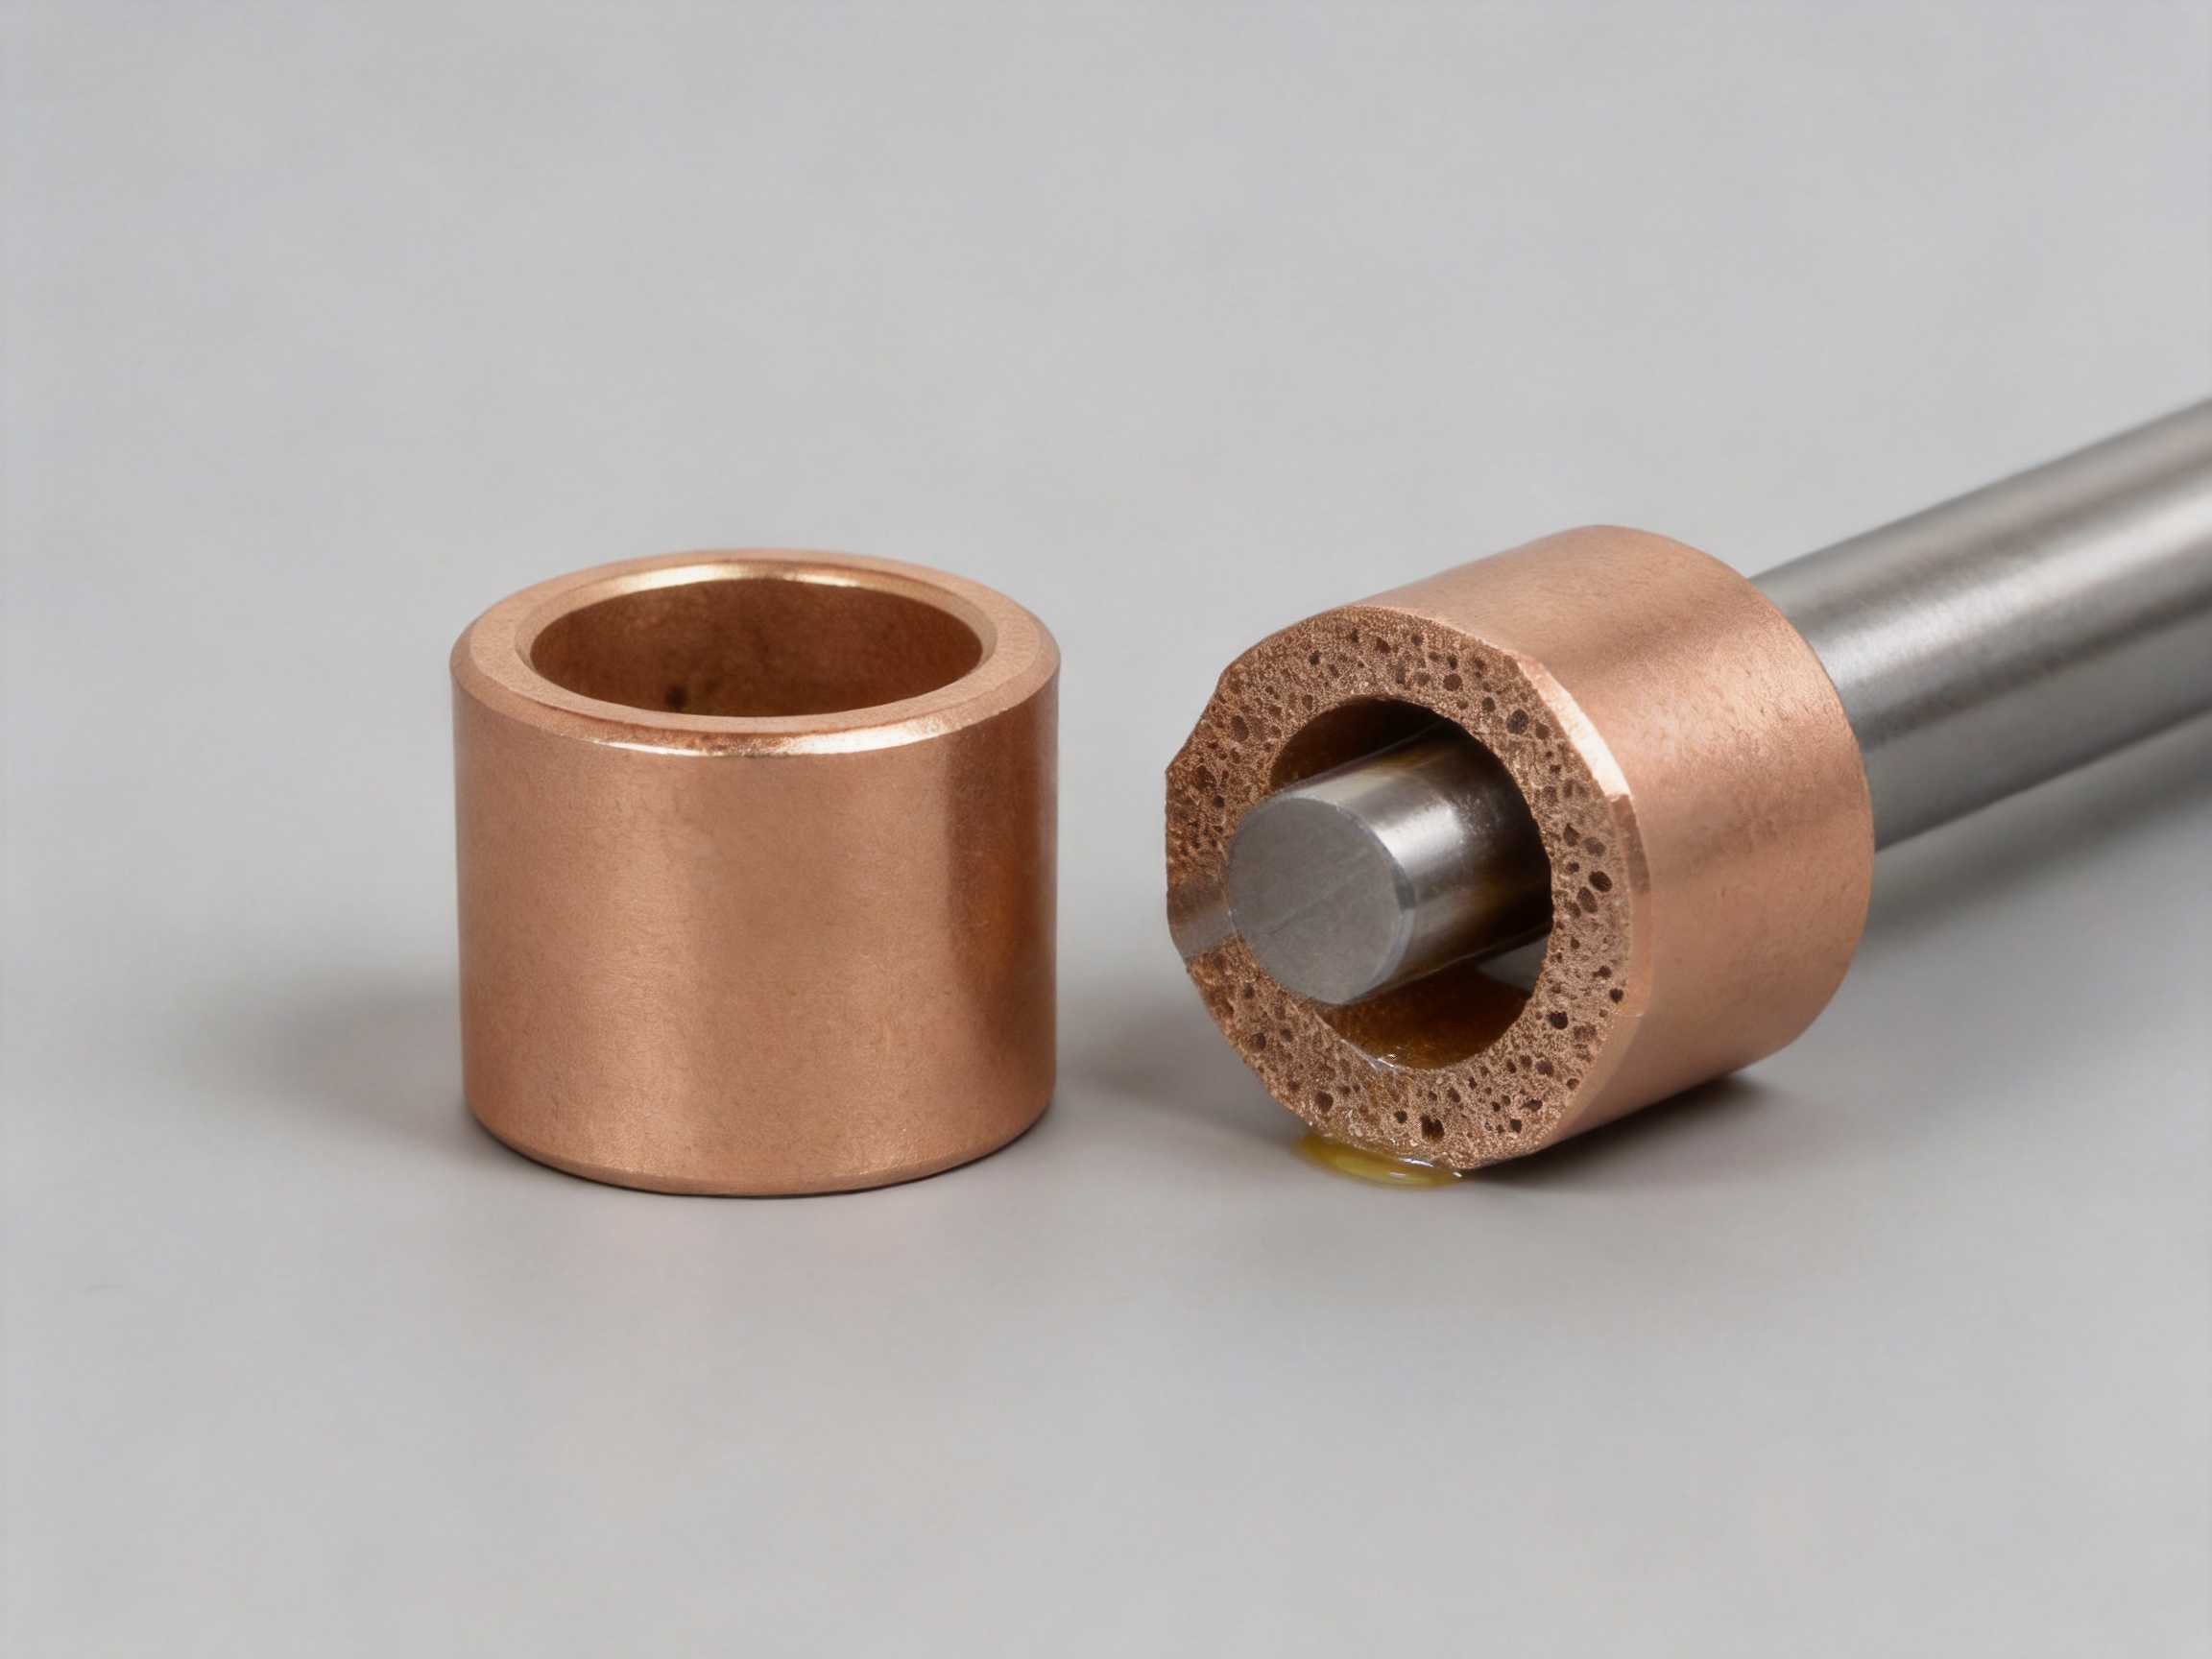
The self-lubricating function of a sintered bronze bushing comes from the relationship between its solid bronze framework and its pore network. During compaction and sintering, the powder particles bond together without eliminating all internal voids. The remaining pores are distributed throughout the bushing and are controlled to provide a balance between strength and oil capacity.
After sintering and sizing, the component is placed in a vacuum environment and immersed in 46# mechanical oil. In the supplied production process, oil impregnation is performed for approximately 20 minutes in an environment maintained at about 80 degrees Celsius. Vacuum conditions help remove air from the internal pores. When the vacuum is released while the bushing remains immersed, oil is drawn into the available pore volume.
This process is more effective than simply applying oil to the surface. Surface-applied lubricant can quickly drain away, evaporate, or be displaced during operation. Impregnated oil is stored within the bushing itself and can gradually feed the sliding interface. The result is a bearing component that can operate with reduced dependence on continuous external lubrication.
Self-lubrication does not mean that the bushing is completely maintenance-free under every condition. Excessive load, high temperature, contamination, incorrect shaft clearance, inadequate alignment, or operation outside the recommended speed range can still cause premature wear. Periodic inspection remains advisable, especially in safety-critical equipment or applications involving severe duty cycles.
The pore structure must be carefully controlled. If porosity is too low, the bushing may not retain enough oil to support self-lubrication. If porosity is too high, the component may lose mechanical strength, dimensional stability, or resistance to impact. A capable powder metallurgy manufacturer therefore manages powder characteristics, compaction pressure, sintering conditions, and density distribution as an integrated system.
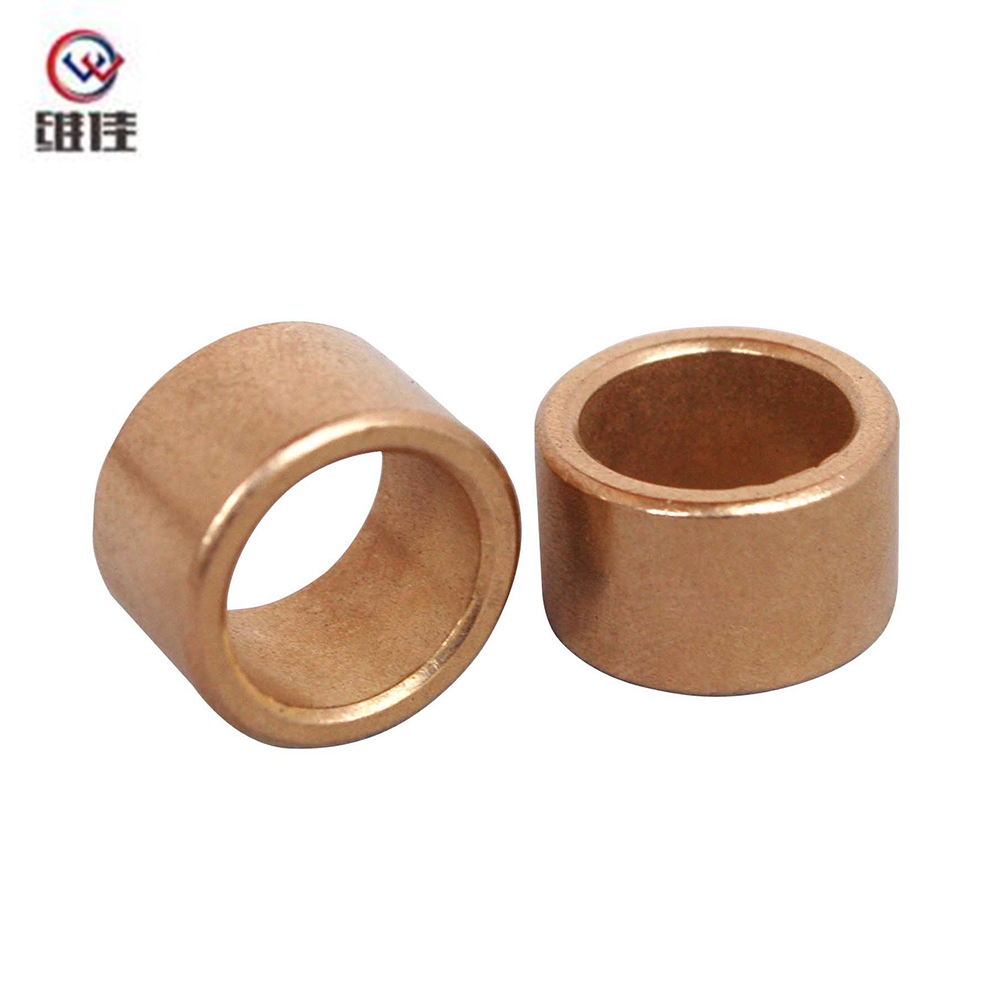
Powder Metallurgy Bronze Bushing (A0667)
4. Manufacturing Process from Powder to Finished Bushing
4.1 Raw Material Preparation
Production begins with the preparation and inspection of CuSn10 bronze powder. Powder composition and particle size influence flowability, filling behavior, compact density, sintering response, surface quality, and final mechanical performance.
Each batch of copper-based powder should be checked to confirm that its composition and particle-size distribution meet the applicable material and process requirements. The supplied quality system identifies raw material composition and particle-size testing as important controls and references compliance with the SNF01-9010-1 standard.
Consistent powder preparation is essential because variations at this stage can create density differences between production batches. In a bushing, uneven density may lead to local differences in strength, pore size, oil retention, dimensional change, and wear resistance. Stable raw material control creates a reliable foundation for subsequent forming and sintering operations.
4.2 Compaction and Forming
During compaction, the bronze powder is filled into a precision mold and compressed under controlled pressure. The mold defines the basic geometry of the bushing, including its outer diameter, inner diameter, length, and other design features that can be formed directly.
Powder compaction offers a significant advantage for repeat production. It can produce large quantities of components with consistent geometry while minimizing material waste. Unlike machining from a solid bar, compaction forms the component close to its final shape and avoids removing large volumes of material.
Uniform filling and controlled pressing are important. If the powder is not distributed evenly, the compact may contain density gradients. These gradients can lead to distortion during sintering or inconsistent performance in service. Modern presses, forming tools, and process monitoring help manufacturers maintain repeatable compaction conditions.
4.3 Sintering
The compacted part is transferred to a controlled-atmosphere sintering furnace. The supplied product information lists a sintering parameter of TCI 690 ± 30 degrees Celsius. During sintering, powder particles bond together through solid-state diffusion, increasing the strength and integrity of the component while preserving the designed porous structure.
Temperature, heating rate, holding time, furnace atmosphere, and cooling conditions all affect the final result. Excessive sintering can close too many pores or cause dimensional changes, while insufficient sintering may produce inadequate strength and weak particle bonding. Process engineers therefore establish a controlled thermal cycle for the selected powder formulation and component geometry.
Controlled-atmosphere sintering also helps protect the copper-based material from undesirable oxidation. Stable furnace conditions support consistent color, surface quality, density, strength, and dimensional behavior. For high-volume production, repeatability from batch to batch is as important as the performance of an individual part.
4.4 Sizing and Precision Calibration
After sintering, the bushing may undergo sizing. Sizing applies controlled pressure through a dedicated tool to improve dimensional accuracy, roundness, straightness, and surface condition. This step is especially important when the component must meet a defined shaft or housing fit.
The A0667 design specifies a concentricity requirement of no more than 0.05 mm. Maintaining concentricity helps prevent uneven contact between the shaft and bushing. Excessive eccentricity can create localized loading, irregular oil-film formation, vibration, and accelerated wear.
Key dimensions are controlled within tight tolerances, with the supplied product information identifying control within ±0.02 mm for important dimensions. The exact tolerance achievable depends on the geometry, tooling, material, production volume, and inspection method, but precision sizing is an important advantage over loosely controlled sintered components.
4.5 Precision Machining and Edge Treatment
Some bushing designs require secondary machining to achieve specific dimensional or surface requirements. Precision machining may be applied to the inner diameter, outer diameter, end faces, grooves, oil holes, or other functional features.
The A0667 bushing includes a 0.4 × 45-degree chamfer. A chamfer reduces the risk of sharp-edge interference during assembly and helps guide the bushing into its housing. It can also reduce the possibility of scraping or damaging the shaft during insertion, provided that the installation method and alignment are appropriate.
Machining operations must be compatible with the porous structure. Excessive cutting or poor tool condition can create burrs, smear the surface, or remove material unevenly. Appropriate tooling, controlled feeds, and post-machining cleaning help preserve the functional quality of the bushing.
4.6 Vacuum Oil Impregnation
Oil impregnation is a defining stage in the production of self-lubricating bronze bushings. Before impregnation, the workpiece is cleaned to remove loose particles and processing residue. The component is then immersed in 46# mechanical oil in an approximately 80-degree Celsius vacuum environment for about 20 minutes.
Heating lowers the viscosity of the oil and improves its ability to enter the fine pore network. Vacuum treatment removes trapped air from the pores. When the pressure condition changes, the oil can penetrate into the internal structure more effectively than under atmospheric immersion alone.
After impregnation, excess oil is removed from the surface. This is important for assembly cleanliness, packaging quality, and reliable dimensional measurement. The finished bushing should contain oil within its pores without presenting unacceptable oil stains or contamination on its external surfaces.
4.7 Cleaning and Packaging
Clean packaging protects the component from dust, moisture, foreign particles, and handling damage. Packaging procedures should be selected according to the product's size, oil condition, shipment distance, and customer requirements.
For international supply, the manufacturer supports express delivery through services such as DHL and FedEx, as well as sea and air freight. Correct packaging helps prevent deformation, surface contamination, and mixing of different specifications during transportation.
5. Quality Control and Inspection Strengths
The reliability of a powder metallurgy bushing depends on more than the nominal alloy designation. Effective quality control must cover raw materials, tooling, forming, thermal processing, sizing, impregnation, final dimensions, and functional characteristics.
First-article inspection is used to verify that the initial production parts conform to the drawing and process requirements. This inspection may include dimensional measurement, weight, appearance, density, concentricity, chamfer condition, and other customer-defined characteristics.
Online dimensional monitoring during compaction, sintering, and sizing helps prevent process drift. If a dimension begins moving toward an unacceptable limit, corrective action can be taken before a large quantity of nonconforming product is produced.
Finished product inspection includes full dimensional inspection according to the supplied quality plan. Sampling tests may cover density, hardness, wear resistance, and other performance indicators. The combination of 100 percent dimensional inspection and sampling-based material or performance testing provides a practical balance between production efficiency and quality assurance.
| Quality Stage | Typical Control Activity | Purpose |
| Raw material inspection | Composition and particle-size testing | Confirm consistent powder behavior and material chemistry |
| Tooling and forming control | Die condition, filling, compaction parameters | Maintain geometry and density uniformity |
| Sintering control | Temperature, atmosphere, cycle, and furnace condition | Develop strength while preserving functional porosity |
| First-article inspection | Complete review of initial parts | Verify drawing and process compliance |
| Online monitoring | Dimensional checks during production | Detect process drift at an early stage |
| Final inspection | Dimensions, appearance, weight, and selected properties | Prevent defective parts from reaching the customer |
| Oil impregnation inspection | Surface cleanliness and oil-retention process review | Support consistent self-lubricating performance |
Jiande Welfine Technology Co., Ltd. operates a quality management system supported by ISO 9001:2015 and IATF 16949:2016 certifications. These certifications reflect a structured approach to process management, traceability, corrective action, customer requirements, and continual improvement. Certification alone does not replace product-specific testing, but it provides an important framework for stable manufacturing.
6. Advantages over Conventional Machined or Cast Bushings
6.1 Improved Material Utilization
Powder metallurgy produces components close to their final shape. This reduces the amount of material removed compared with machining a bushing from a solid copper or bronze bar. Lower material waste can improve production efficiency and support more competitive pricing, particularly for repeat orders.
6.2 Consistent Mass Production
Once the tooling and process parameters have been validated, powder compaction can produce large quantities of repeat components with consistent geometry. This is valuable for automotive, appliance, motor, and industrial equipment manufacturers that require stable supply across multiple production batches.
6.3 Integrated Oil Retention
A cast or fully machined bronze bushing may require an external lubrication system, periodic grease application, or oil grooves to maintain a lubricating film. A sintered bronze bushing can store lubricant within its internal pores, reducing the dependence on frequent manual lubrication.
6.4 Dimensional Efficiency
Precision sizing and controlled secondary machining allow the bushing to meet defined assembly dimensions without extensive post-processing. The A0667 component is manufactured with controlled key dimensions and a concentricity requirement of not more than 0.05 mm.
6.5 Balanced Performance
Compared with some polymer bushings, CuSn10 bronze offers higher thermal conductivity and better resistance to certain mechanical loads. Compared with ordinary brass, it can provide improved wear resistance and load capacity. Compared with some fully dense bronze designs, its oil-retaining porosity adds a self-lubricating function.
These advantages do not make powder metallurgy bushings universally superior for every application. Polymer, composite, steel-backed, graphite-plugged, or fully dense bronze bearings may be preferable in particular temperature, chemical, load, or speed conditions. The correct selection should be based on the complete operating profile rather than material name alone.
7. Application Areas
7.1 Automotive Engine and Chassis Components
Automotive mechanisms contain numerous pivot points, linkages, actuators, transmission components, and support structures that require controlled sliding motion. A compact self-lubricating bronze bushing can reduce friction and maintenance in suitable non-critical assemblies.
In chassis-related mechanisms, bushings may experience vibration, intermittent movement, impact, and contamination. The CuSn10 bronze matrix provides wear resistance, while the impregnated oil supports low-friction movement during repeated cycles. Final suitability must be confirmed through application testing, especially where safety, extreme loads, or severe contamination are involved.
7.2 Electric Motors and Gearboxes
Electric motors require stable support for rotating shafts and moving components. A bushing with good dimensional accuracy and thermal conductivity can help maintain reliable shaft guidance. The self-lubricating structure is particularly useful where adding lubricant after assembly is inconvenient.
In gearboxes and transmission structures, the bushing may operate under combined radial load, oscillation, and occasional shock. Correct shaft hardness, surface finish, alignment, and clearance are essential to obtain the expected service life.
7.3 Fans and Refrigerators
Fans and refrigeration appliances often contain compact rotating or oscillating mechanisms that must operate quietly and efficiently. The A0667 product information identifies applications in fans and refrigerators. Its controlled dimensions and oil-impregnated structure can support low-friction operation in appropriate appliance assemblies.
Appliance manufacturers also benefit from the repeatability of powder metallurgy production. Stable component dimensions help simplify automated assembly and reduce adjustment requirements on the production line.
7.4 Hydraulic Pumps and Valve Assemblies
Hydraulic systems require accurate guidance and reliable movement under pressure, vibration, and repeated duty cycles. Powder metallurgy bronze bushings can be used in selected pump, valve, guide, and linkage assemblies where the load, pressure, speed, fluid compatibility, and temperature are within the design range.
Because hydraulic equipment can be sensitive to contamination, the cleanliness of the finished bushing and compatibility between the impregnated oil and the hydraulic medium must be evaluated. Where direct contact with hydraulic fluid is expected, technical validation should be completed before volume production.
7.5 Precision Machine Tools
Machine tools require stable positioning, controlled movement, and repeatable dimensional performance. A bushing with low friction and controlled concentricity can support guide mechanisms, adjustment systems, and auxiliary movement assemblies.
The 0.4 × 45-degree chamfer specified for the A0667 bushing can assist insertion into a prepared housing. However, assembly forces should be applied evenly and through suitable tooling to avoid distortion of the porous sleeve.
7.6 Agricultural Machinery
Agricultural equipment frequently operates in dusty, humid, and highly variable environments. Components may experience repeated start-stop motion and extended intervals between scheduled maintenance. The oil-retaining structure of a sintered bronze bushing can help maintain lubrication over extended operating periods.
Sealing, protective design, correct installation, and periodic inspection remain important because abrasive particles can accelerate wear in any sliding bearing. The bushing should be selected with consideration for load, speed, exposure, and cleaning conditions.
7.7 Automation and Industrial Equipment
Automated equipment often combines high cycle counts with strict requirements for repeatability. Bushings used in motion assemblies, linkages, indexing mechanisms, and compact actuators must maintain accurate alignment over many cycles.
Powder metallurgy is well suited to these applications because it supports repeat production of small precision parts. The manufacturer can also develop customized dimensions, materials, and features according to drawings or samples, allowing the bushing to be integrated into a specific machine design.
8. Installation and Operating Considerations
Even a high-quality bushing can fail prematurely if it is installed incorrectly. The housing bore should be clean, accurately prepared, and free from burrs. The shaft should have a suitable diameter, surface finish, hardness, and straightness. Misalignment can create edge loading and uneven wear.
Installation force should be applied through a mandrel or tool that contacts the appropriate surface. Hammering directly on the bushing can deform the sleeve, damage the edge, or alter the internal diameter. The chamfer should be aligned with the entry side of the housing when the design requires it.
Clearance must be selected according to operating conditions. High speed and high temperature generally require more clearance because thermal expansion and lubricant behavior must be considered. Low-speed oscillating movement or heavy load may require a different clearance strategy. The recommended value should be confirmed through the equipment design or technical consultation.
During initial operation, the assembly should be monitored for abnormal noise, excessive temperature, vibration, shaft scoring, or oil leakage. A short running-in period may allow the sliding surfaces to establish a stable contact pattern. If the component overheats immediately, the equipment should be stopped and the cause investigated.
Contamination control is also important. Dust, metal particles, water, and chemical residues can reduce the effectiveness of the oil film and accelerate abrasive or corrosive wear. Protective seals, clean assembly procedures, and suitable storage conditions help preserve bushing performance.
9. Customization and OEM/ODM Capabilities
Many industrial bushings are not standard catalog components. They may require special diameters, lengths, tolerances, grooves, oil holes, flanges, steps, slots, or material grades. Jiande Welfine Technology Co., Ltd. provides customized powder metallurgy structural parts and bushing solutions based on customer drawings, samples, and technical requirements.
Customization begins with a review of the application. Important information includes the bushing dimensions, shaft material, housing material, radial and axial loads, rotational or oscillating speed, operating temperature, lubrication requirements, environmental exposure, expected life, assembly method, and annual quantity.
The manufacturer can support both small-batch prototyping and mass production. Prototype work allows the design, material, fit, and process to be evaluated before committing to production tooling. Once the design is approved, dedicated tooling and controlled production parameters can provide stable output for larger orders.
Material selection can also be adapted to the application. While CuSn10 is suitable for many general-purpose self-lubricating bronze bushings, other copper-based or iron-based powder metallurgy materials may be considered where the load, cost, magnetic properties, or operating environment differs.
Customers can provide drawings or physical samples for quotation and engineering review. The stated service process supports a precise quotation within 24 hours after receipt of the necessary technical information. Standard orders are described as having a typical delivery period of 7–15 working days, while urgent orders may receive priority production subject to capacity and material availability.
10. Manufacturing Infrastructure and Company Strengths
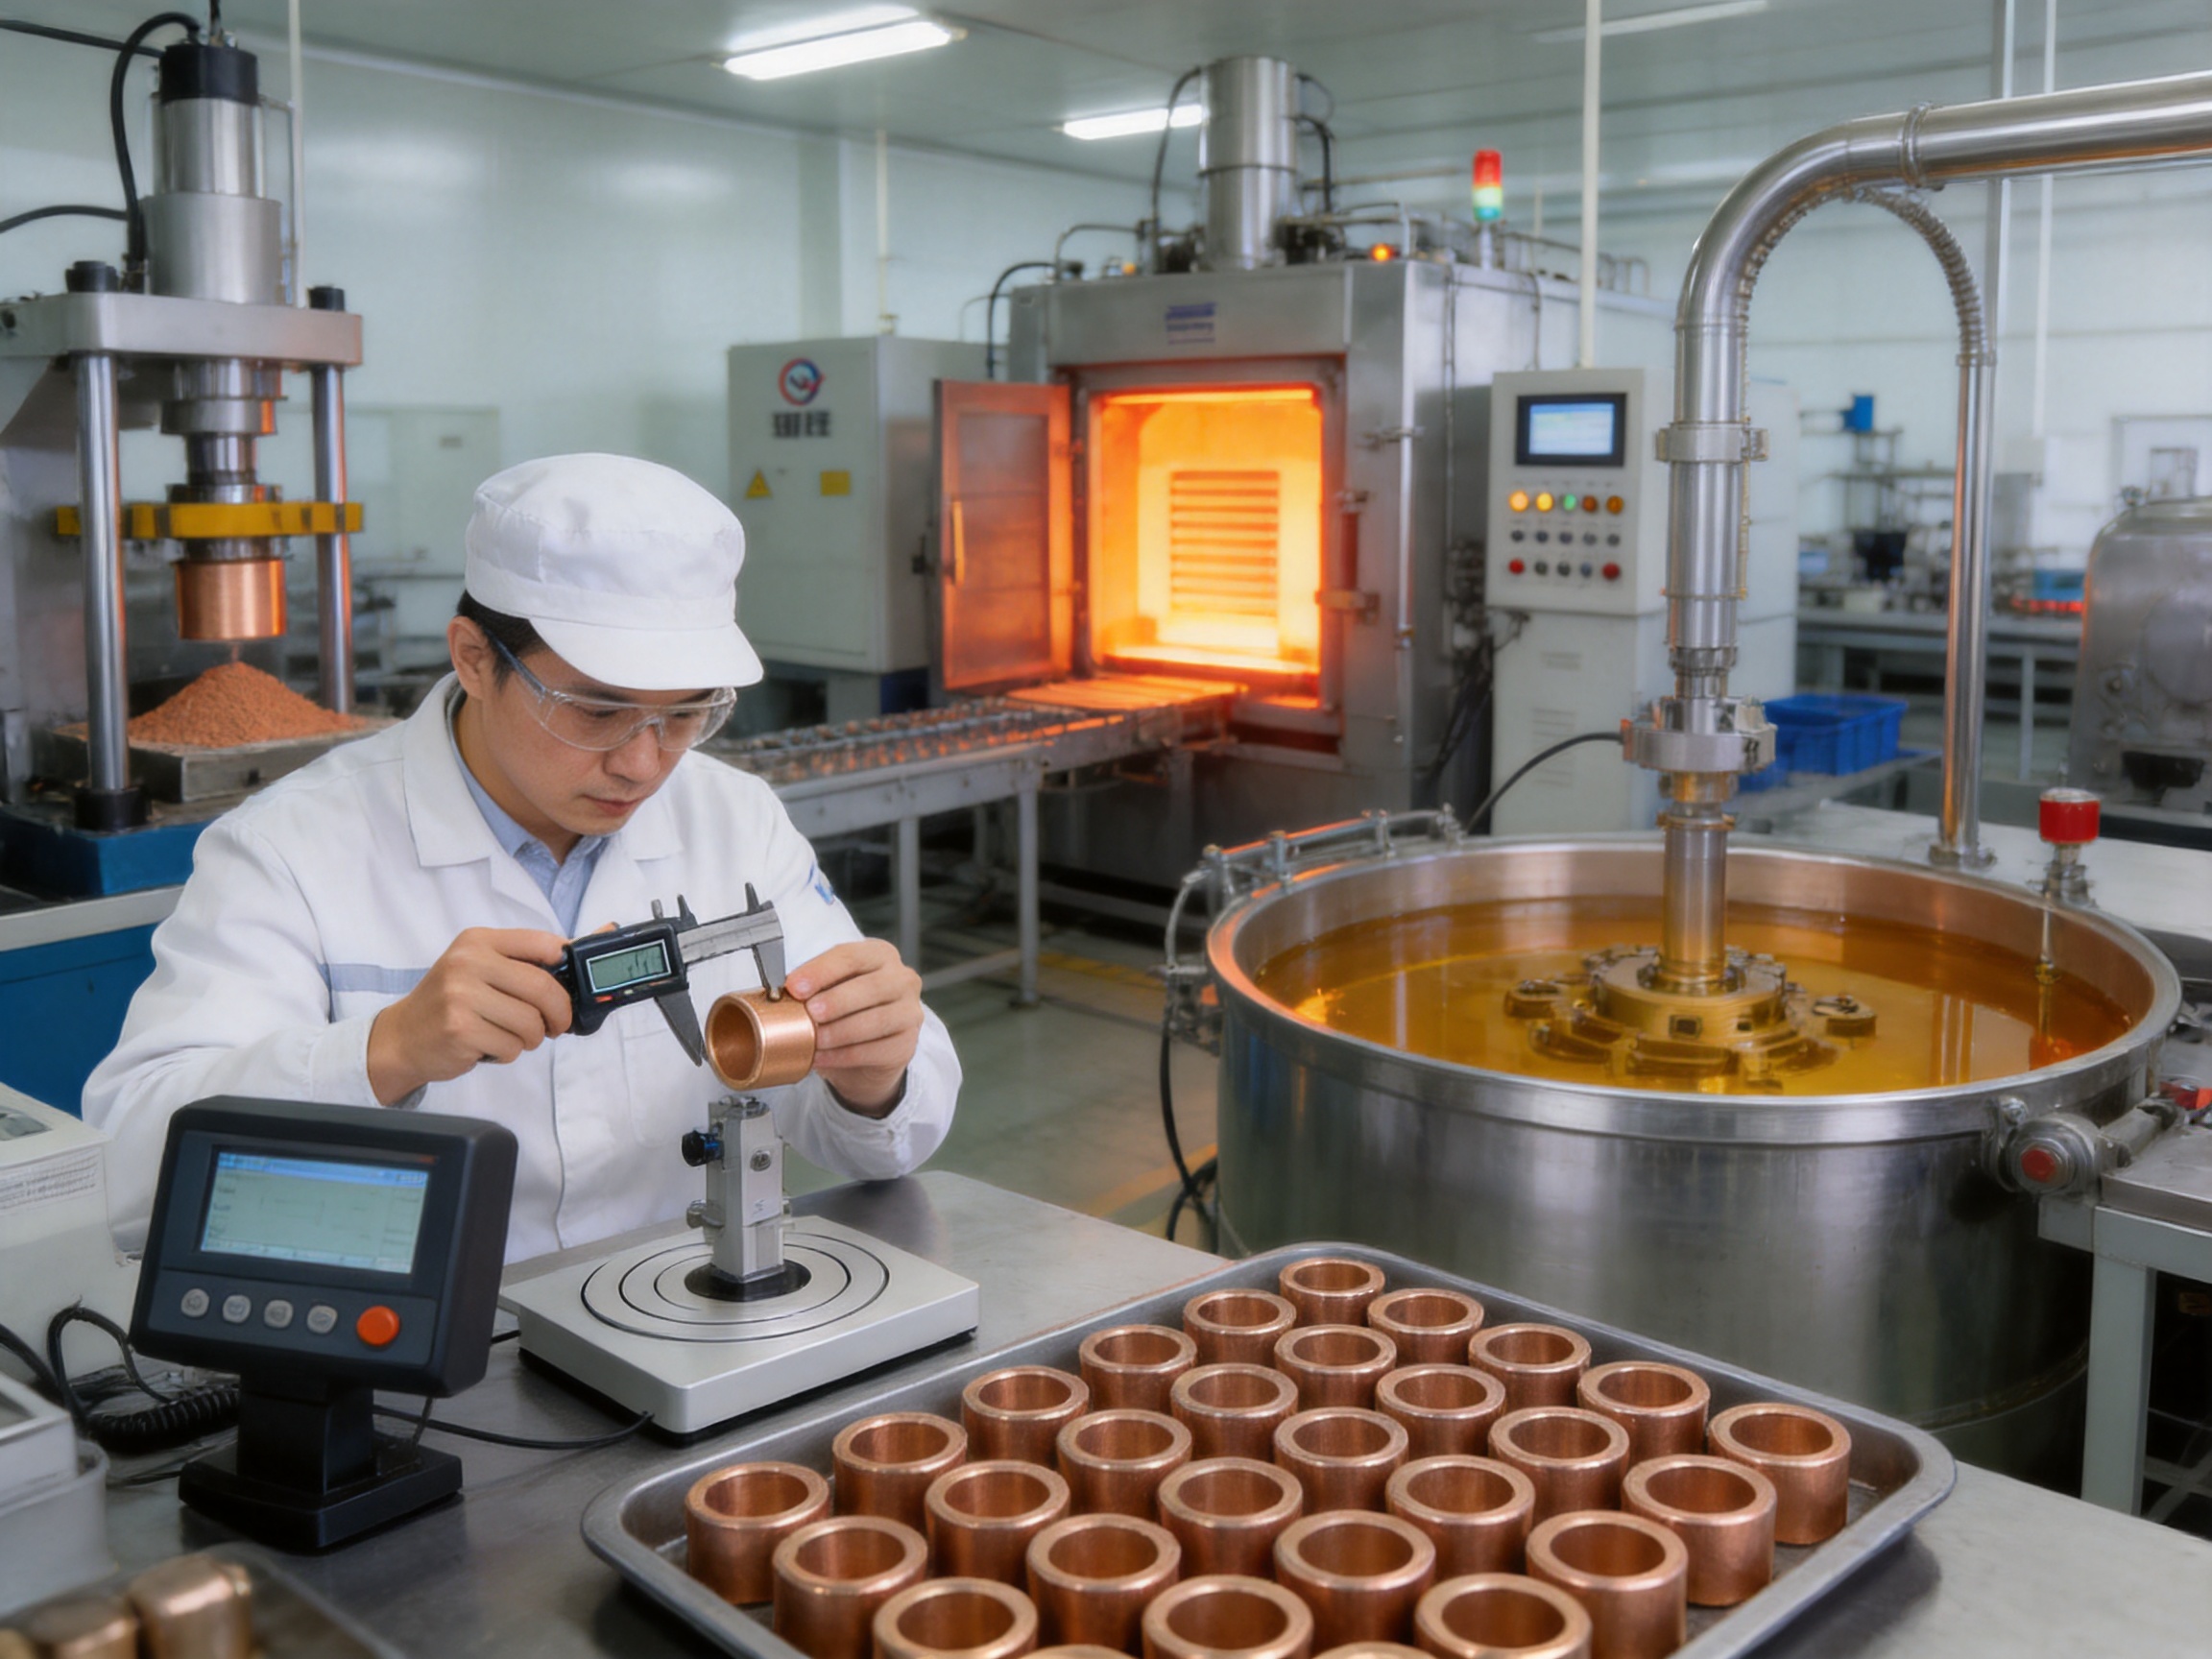
Jiande Welfine Technology Co., Ltd. was established in 2001 and specializes in powder metallurgy sintering, self-lubricating bushings, and precision components. The company integrates research and development, production, inspection, and sales, enabling it to support customers from initial design review through repeat manufacturing.
The company operates a production base covering approximately 13,039 square meters and employs more than 150 skilled personnel. Its equipment includes high-efficiency presses, high-temperature sintering furnaces, precision forming machines, and testing equipment. This infrastructure supports the complete process chain required for sintered components.
More than two decades of industry experience provide practical knowledge in powder formulation, tooling, density control, sintering, sizing, oil impregnation, and precision inspection. This experience is particularly important for components in which the balance between strength and porosity must be carefully managed.
The company's ISO 9001:2015 and IATF 16949:2016 certifications support a systematic approach to quality management and automotive-related production requirements. Its OEM and ODM capabilities allow customers to obtain customized components rather than adapting their assemblies to a limited standard product range.
Technical communication is another important strength. A bushing should not be selected by dimensions alone. The manufacturer can review drawings, samples, and operating conditions to help determine whether CuSn10 powder metallurgy bronze is suitable and whether modifications are needed for fit, lubrication, or production efficiency.
11. How to Select the Correct CuSn10 Bushing
Selection should begin with the complete duty cycle. Identify whether the motion is continuous rotation, oscillation, reciprocation, or intermittent movement. Determine the radial load, axial load, peak load, speed, acceleration, start-stop frequency, and expected operating hours.
Temperature is equally important. The bushing, shaft, housing, and impregnated oil must remain compatible at the lowest and highest operating temperatures. Heat generated by friction and nearby components should be included in the assessment.
Next, evaluate the shaft and housing. Shaft diameter, hardness, surface finish, roundness, straightness, and material all affect wear. The housing must provide adequate support without distorting the bushing during installation. Alignment should be checked where multiple bushings support the same shaft.
Environmental conditions should also be documented. Dust, water, humidity, chemicals, cleaning agents, salt spray, and outdoor exposure can influence the choice of material and sealing arrangement. If the bushing will contact hydraulic fluid, fuel, refrigerant, or another process liquid, compatibility testing may be required.
Finally, consider production requirements. Annual volume, allowable variation, packaging, inspection reports, traceability, delivery schedule, and future design changes should be discussed before tooling is finalized.
| Selection Factor | Questions to Confirm |
| Motion | Is the movement rotational, oscillating, reciprocating, or intermittent? |
| Load | What are the continuous, peak, impact, radial, and axial loads? |
| Speed | What are the average, maximum, and start-stop speeds? |
| Temperature | What temperature range will the bushing experience? |
| Fit | What are the shaft, housing, clearance, and tolerance requirements? |
| Environment | Will the component encounter dust, water, chemicals, or corrosive conditions? |
| Lubrication | Is impregnated oil sufficient, or is supplemental lubrication needed? |
| Production | What are the annual quantity, inspection, packaging, and delivery requirements? |
12. Frequently Asked Questions
What is a CuSn10 powder metallurgy bronze bushing?
It is a porous bronze sleeve manufactured from CuSn10 powder through compaction, sintering, sizing, and related precision processes. The pores are impregnated with mechanical oil so the bushing can release lubricant during operation and support self-lubricating sliding contact.
What does the CuSn10 designation mean?
CuSn10 identifies a copper-tin bronze material containing approximately 10 percent tin. The tin improves hardness, wear resistance, and load performance compared with many softer copper materials.
Can the bushing operate without regular lubrication?
Under suitable operating conditions, the oil-retaining pore structure can significantly reduce the need for external lubrication. It should not be interpreted as unlimited maintenance-free operation. Load, speed, temperature, contamination, clearance, alignment, and duty cycle all affect performance. Periodic inspection remains recommended.
Is this bushing suitable for high-speed equipment?
It can be suitable for many medium- and high-speed applications when the load, clearance, temperature, shaft condition, and oil characteristics are appropriate. The permissible operating range should be confirmed for the specific equipment rather than assumed from the material designation alone.
How does it differ from a cast bronze bushing?
A powder metallurgy bushing contains a controlled porous structure that can retain impregnated oil. It also offers efficient near-net-shape production, good dimensional repeatability, and reduced material waste. Cast bronze may be preferable for certain very high-load, large-size, or specialized applications, so the best choice depends on the operating conditions.
How does it differ from a machined solid bronze bushing?
A machined solid bronze bushing is generally dense and may require external grooves or a separate lubrication system. A sintered bushing stores oil internally and can be produced efficiently in repeat quantities. Machined solid bronze may still be selected where maximum density, special geometry, or unusually severe loading is required.
What is the purpose of the 0.4 × 45-degree chamfer?
The chamfer helps guide the bushing during assembly and reduces the risk of sharp-edge interference. It can also reduce the possibility of damaging the housing or shaft during insertion when the parts are correctly aligned.
What does the 0.05 mm concentricity requirement indicate?
It indicates that the relevant cylindrical features are controlled so their axes remain within a maximum specified deviation of 0.05 mm. Good concentricity supports more uniform shaft contact and helps reduce localized loading and vibration.
Can the product be customized?
Yes. Custom dimensions, materials, tolerances, features, and production quantities can be evaluated based on customer drawings, samples, or technical requirements. The manufacturer supports prototype development and mass production for customized powder metallurgy components.
What information should be provided for a quotation?
Customers should provide a drawing or sample, material requirement, annual quantity, tolerances, surface or dimensional requirements, application description, load, speed, temperature, lubrication conditions, and delivery expectations. Complete information allows the manufacturer to recommend a suitable process and prepare a more accurate quotation.
How long is the usual delivery time?
Standard orders are described as having a typical lead time of 7–15 working days. Actual delivery depends on tooling, material availability, order quantity, inspection requirements, and production schedule. Urgent orders may be considered for priority production.
What after-sales support is available?
Technical installation guidance is available, and products with mismatched dimensions or materials are subject to replacement according to the supplier's after-sales policy. Customers should provide inspection data, photographs, application details, and other relevant information when reporting a quality issue.
13. Conclusion
The CuSn10 powder metallurgy bronze bushing combines the wear resistance and thermal properties of tin bronze with the oil-retaining capability of a controlled porous structure. This combination makes it a practical solution for many sliding and guiding applications where low maintenance, dimensional consistency, and long operating life are important.
The A0667 bushing demonstrates the value of an integrated manufacturing process. CuSn10 powder is inspected before use, compacted into a controlled form, sintered at a defined temperature range, sized for dimensional accuracy, machined where necessary, inspected for concentricity and critical dimensions, and vacuum-impregnated with 46# mechanical oil. Cleaning and packaging complete the process and help preserve the component's condition through delivery.
Compared with ordinary brass, the product offers a stronger combination of wear resistance, load capacity, and oil retention. Compared with conventional machined bushings, powder metallurgy can reduce material waste and support efficient mass production. Compared with non-impregnated sleeves, the internal oil supply can reduce dependence on frequent external lubrication.
Its final performance still depends on correct application engineering. Shaft and housing conditions, operating clearance, load, speed, temperature, contamination, alignment, and installation quality must be evaluated before production approval. With appropriate selection and process control, the CuSn10 powder metallurgy bronze bushing can support reliable operation in automotive systems, electric motors, hydraulic equipment, appliances, agricultural machinery, automation equipment, precision machinery, and other industrial assemblies.
Through long-term experience in powder metallurgy, modern production equipment, structured quality management, and OEM/ODM engineering support, Jiande Welfine Technology Co., Ltd. provides a complete route from customized design to stable volume production. This combination of material expertise, process control, precision inspection, and customer support makes the product suitable for manufacturers seeking dependable self-lubricating bronze bushings and precision sintered components.
References
1. Powder Metallurgy Association, Powder Metallurgy Materials and Processing Principles.
2. ISO 9001:2015, Quality Management Systems—Requirements.
3. IATF 16949:2016, Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
4. ASM International, ASM Handbook: Powder Metallurgy.
5. ASM International, ASM Handbook: Properties and Selection of Nonferrous Alloys and Special-Purpose Materials.
6. Standard technical practices for porous sintered bronze bearings and oil-impregnated bushings.
7. Product technical information for CuSn10 Powder Metallurgy Bronze Bushing, Product Code A0667.
8. Manufacturer process information covering compaction, sintering, sizing, vacuum oil impregnation, inspection, packaging, and customized powder metallurgy production.
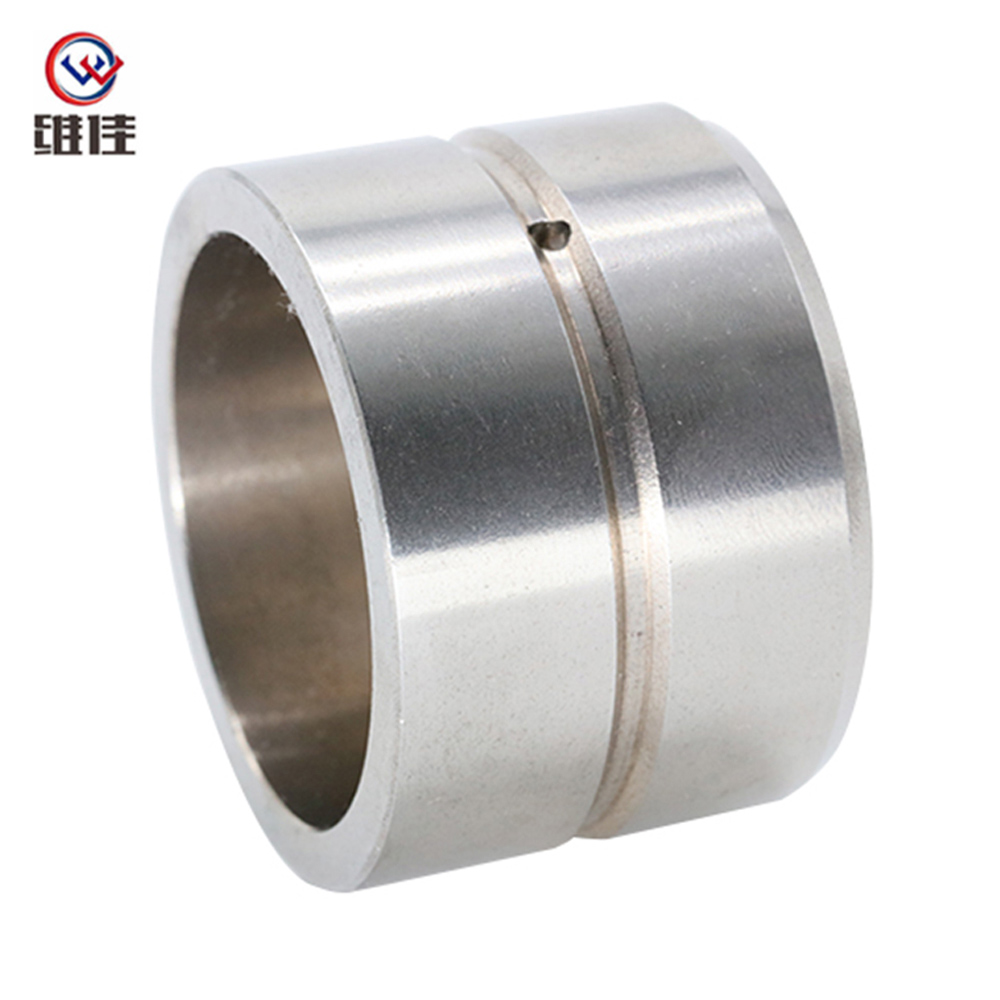
Product: Powder Metallurgy Bronze Bushing (A0667)
Related products
-
-
Product Description: High-precision powder metallurgy part (S14*7*10) made of iron material from Jiande Wefine, customized PM components with strict tolerance control.
See Details -
This copper-based powder metallurgy bushing is manufactured through an integrated process of compaction, sintering, sizing, and oil impregnation. It features excellent wear resistance and self-lubrica...
See Details
Copyright © Jiande Welfine Technology Co., Ltd. All Rights Reserved. Privacy Custom Self-lubricating Sintered Bushing Manufacturers
