E-mail us: [email protected]
Tel: +86-15239857375
 English
 中文简体


 Home / Author / Shen Yiruo — Senior After-Sales Service Manager / CuSn10 Powder Metallurgy Bronze Bushing: High-Performance Self-Lubricating Solution for Precision Machinery
CuSn10 Powder Metallurgy Bronze Bushing: High-Performance Self-Lubricating Solution for Precision Machinery
 2026.10.08
 Shen Yiruo — Senior After-Sales Service Manager
Content
- 1 1. Product Overview
- 2 2. Why CuSn10 Is Suitable for Powder Metallurgy Bushings
- 3 3. Advantages Over Conventional Bushing Materials
- 4 4. Precision Design of the A0667 Bushing
- 5 5. Integrated Manufacturing Process
- 6 6. Vacuum Oil Impregnation
- 7 7. Quality Control and Manufacturing Strengths
- 8 8. Applications of CuSn10 Powder Metallurgy Bushings
- 9 9. Comparison with Other Sintered and Self-Lubricating Bearings
- 10 10. Installation and Service Recommendations
- 11 11. Custom Manufacturing Capabilities
- 12 12. Ordering, Delivery, and Technical Support
- 13 13. Why This Product Is a Competitive Choice
- 14 14. Future Development of Powder Metallurgy Bronze Bushings
- 15 15. Frequently Asked Questions
- 15.1 Can the CuSn10 powder metallurgy bushing operate without regular lubrication?
- 15.2 What is the main advantage of CuSn10 over standard brass?
- 15.3 How does vacuum oil impregnation improve performance?
- 15.4 What does the density range of 5.7–5.8 g/cm³ indicate?
- 15.5 Why is concentricity important for a bushing?
- 15.6 What is the purpose of the 0.4 × 45° chamfer?
- 15.7 Is this bushing suitable for high-speed equipment?
- 15.8 Can the product be customized?
- 15.9 What information should be provided when requesting a quotation?
- 15.10 How should the bushing be installed?
- 15.11 What quality certifications support production capability?
- 15.12 What industries commonly use this type of bushing?
- 16 Conclusion
- 17 References
- 18 Product: Powder Metallurgy Bronze Bushing (A0667)
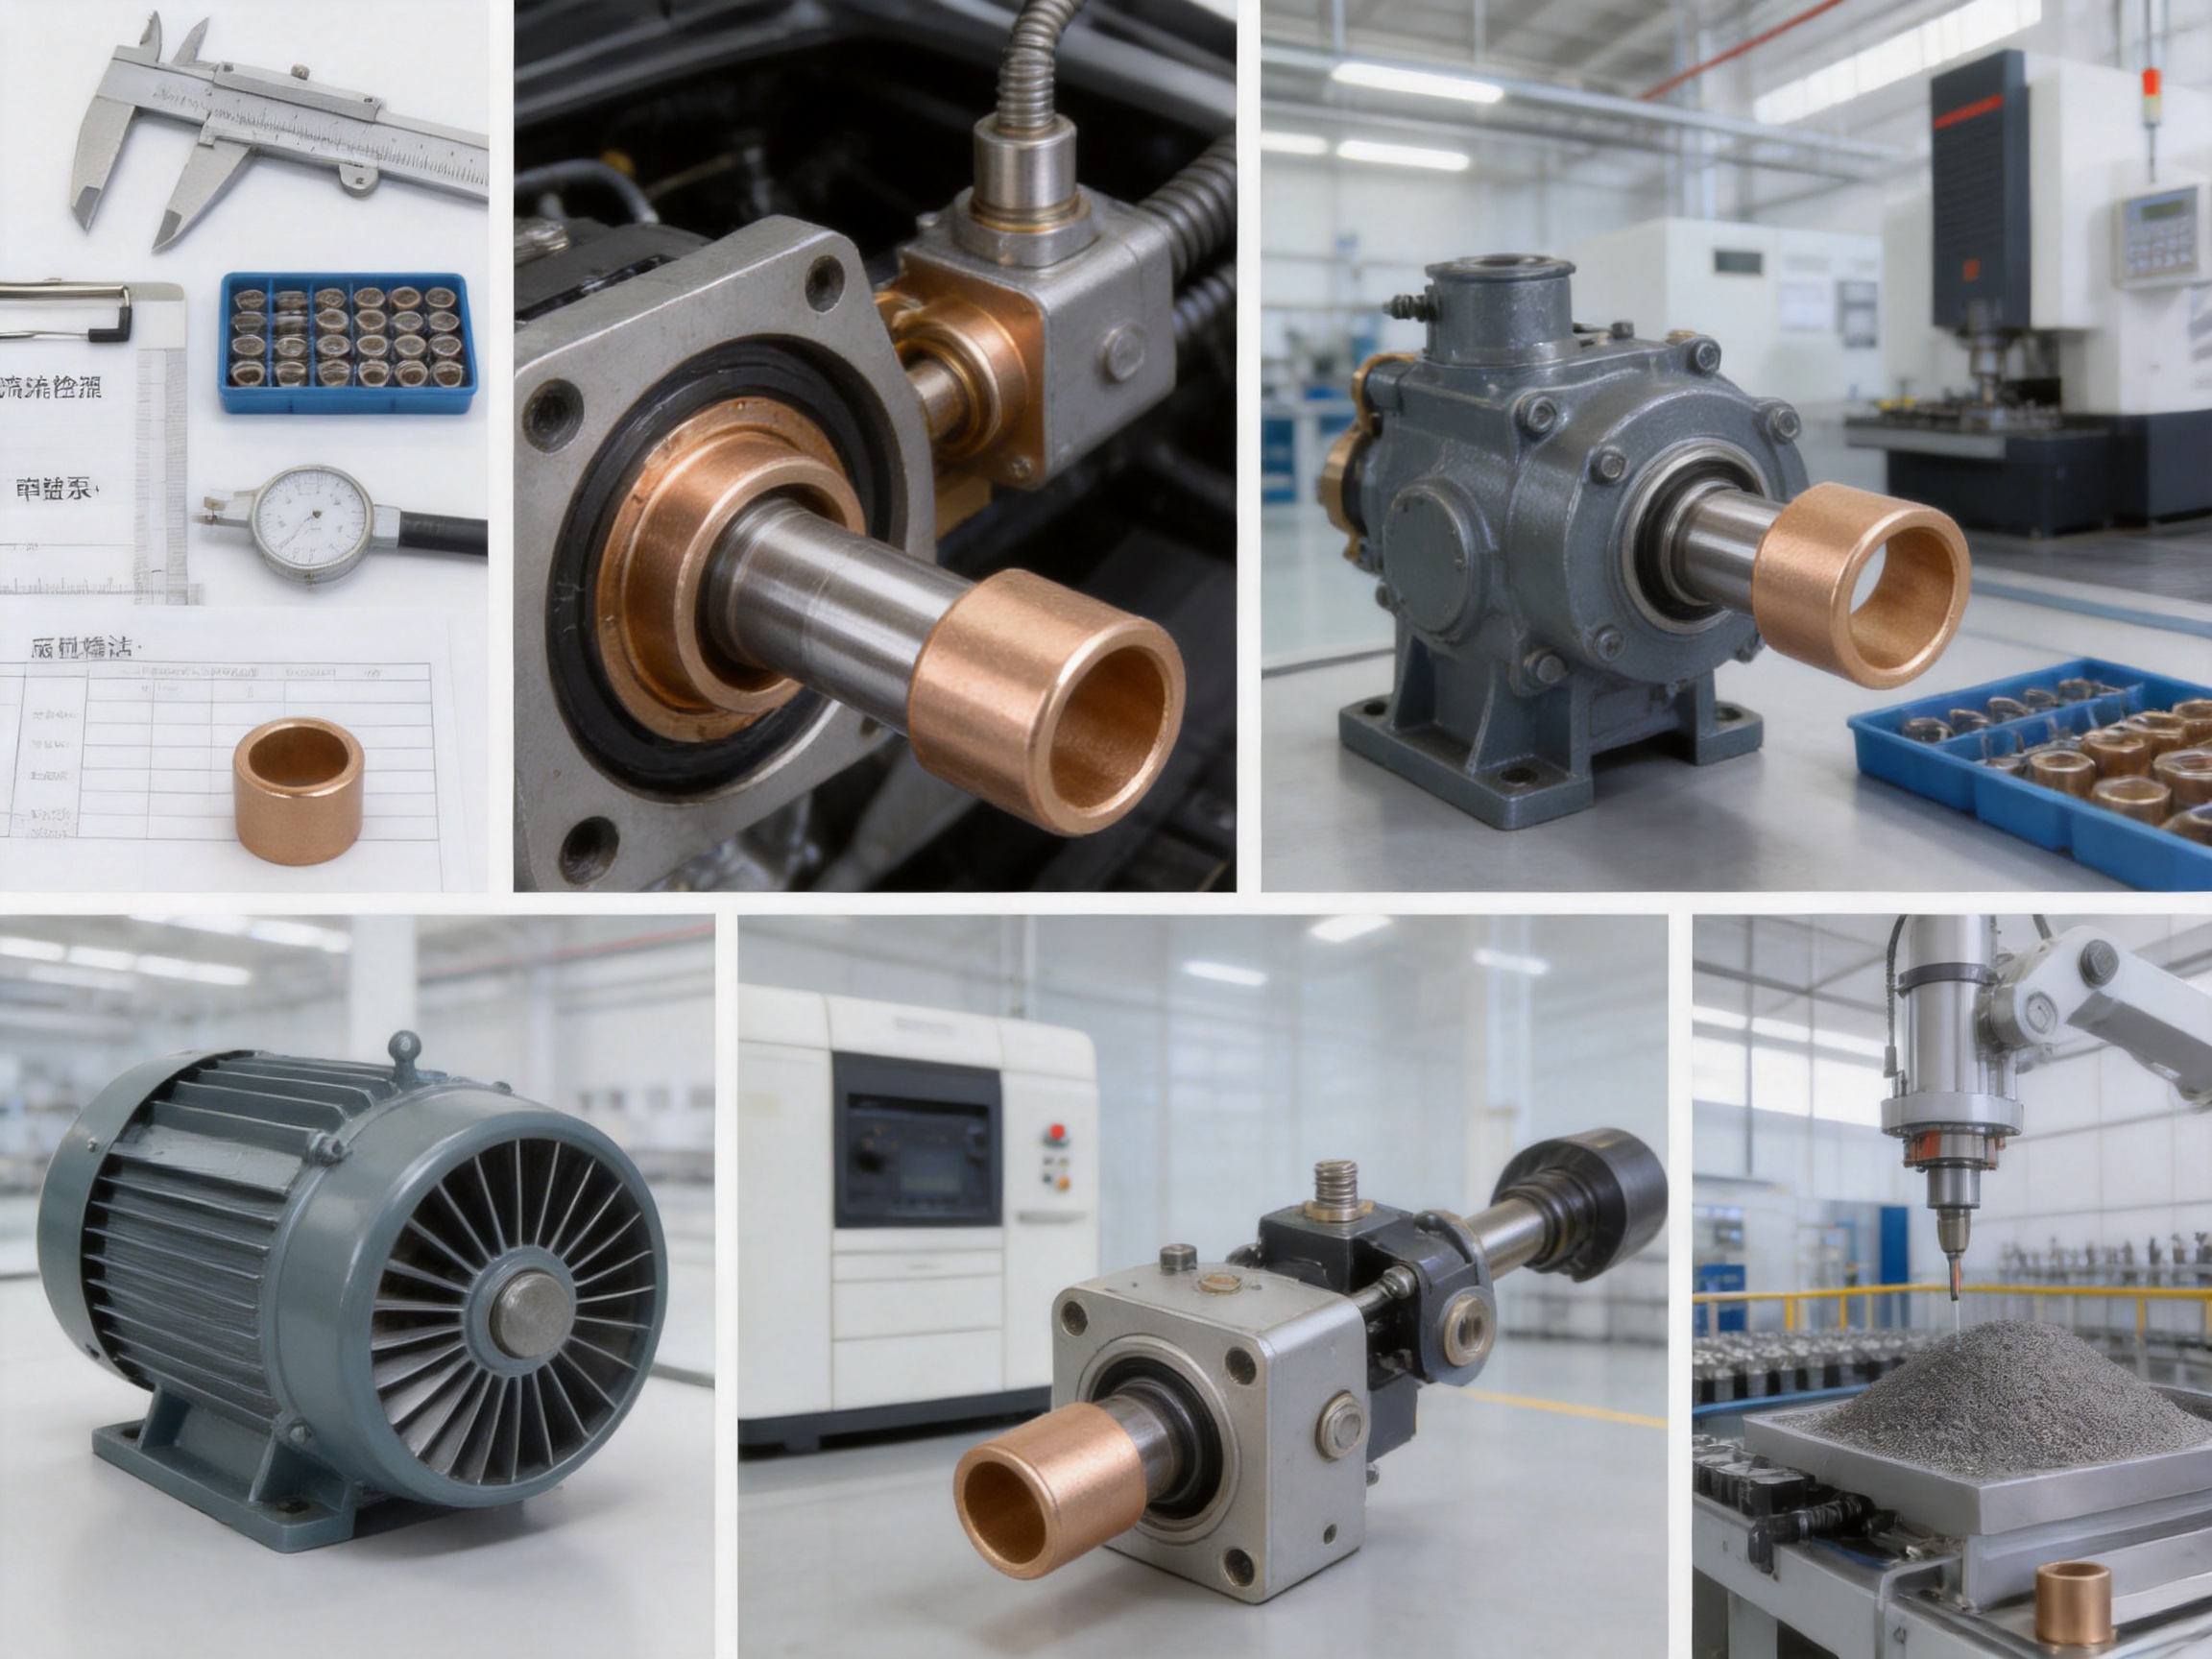
CuSn10 powder metallurgy bronze bushings are designed for machinery that requires reliable shaft support, controlled friction, long service life, and reduced lubrication maintenance. Manufactured from a copper-tin alloy containing approximately 10% tin, these bushings combine the inherent wear resistance of bronze with the oil-retaining capability of a carefully controlled porous structure.
The Powder Metallurgy Bronze Bushing A0667 is a representative precision component developed for demanding mechanical assemblies. It is produced through compaction, sintering, sizing, precision control, and vacuum oil impregnation. This integrated process allows the manufacturer to control material composition, density, dimensional accuracy, concentricity, and lubrication performance throughout production.
With a CuSn10 material specification, a nominal size of 10G7 × 13s7 × 10 mm, a concentricity of no more than 0.05 mm, and a controlled density range of 5.7–5.8 g/cm³, the bushing is suitable for compact assemblies in automotive components, precision machinery, hydraulic systems, fans, refrigerators, household appliances, and other equipment requiring stable sliding performance.
Unlike ordinary solid bronze bushings that normally require a continuous external supply of grease or oil, an oil-impregnated powder metallurgy bushing stores lubricant inside its interconnected pores. During operation, frictional heat and movement encourage oil to migrate toward the sliding interface. When the equipment stops, part of the oil can return to the porous structure through capillary action. This creates a practical self-lubricating effect that can reduce maintenance frequency.
1. Product Overview
The CuSn10 powder metallurgy bronze bushing is a cylindrical bearing component used between a shaft and a housing. Its primary function is to provide a low-friction sliding surface while supporting radial loads, guiding movement, and protecting the surrounding assembly from excessive wear.
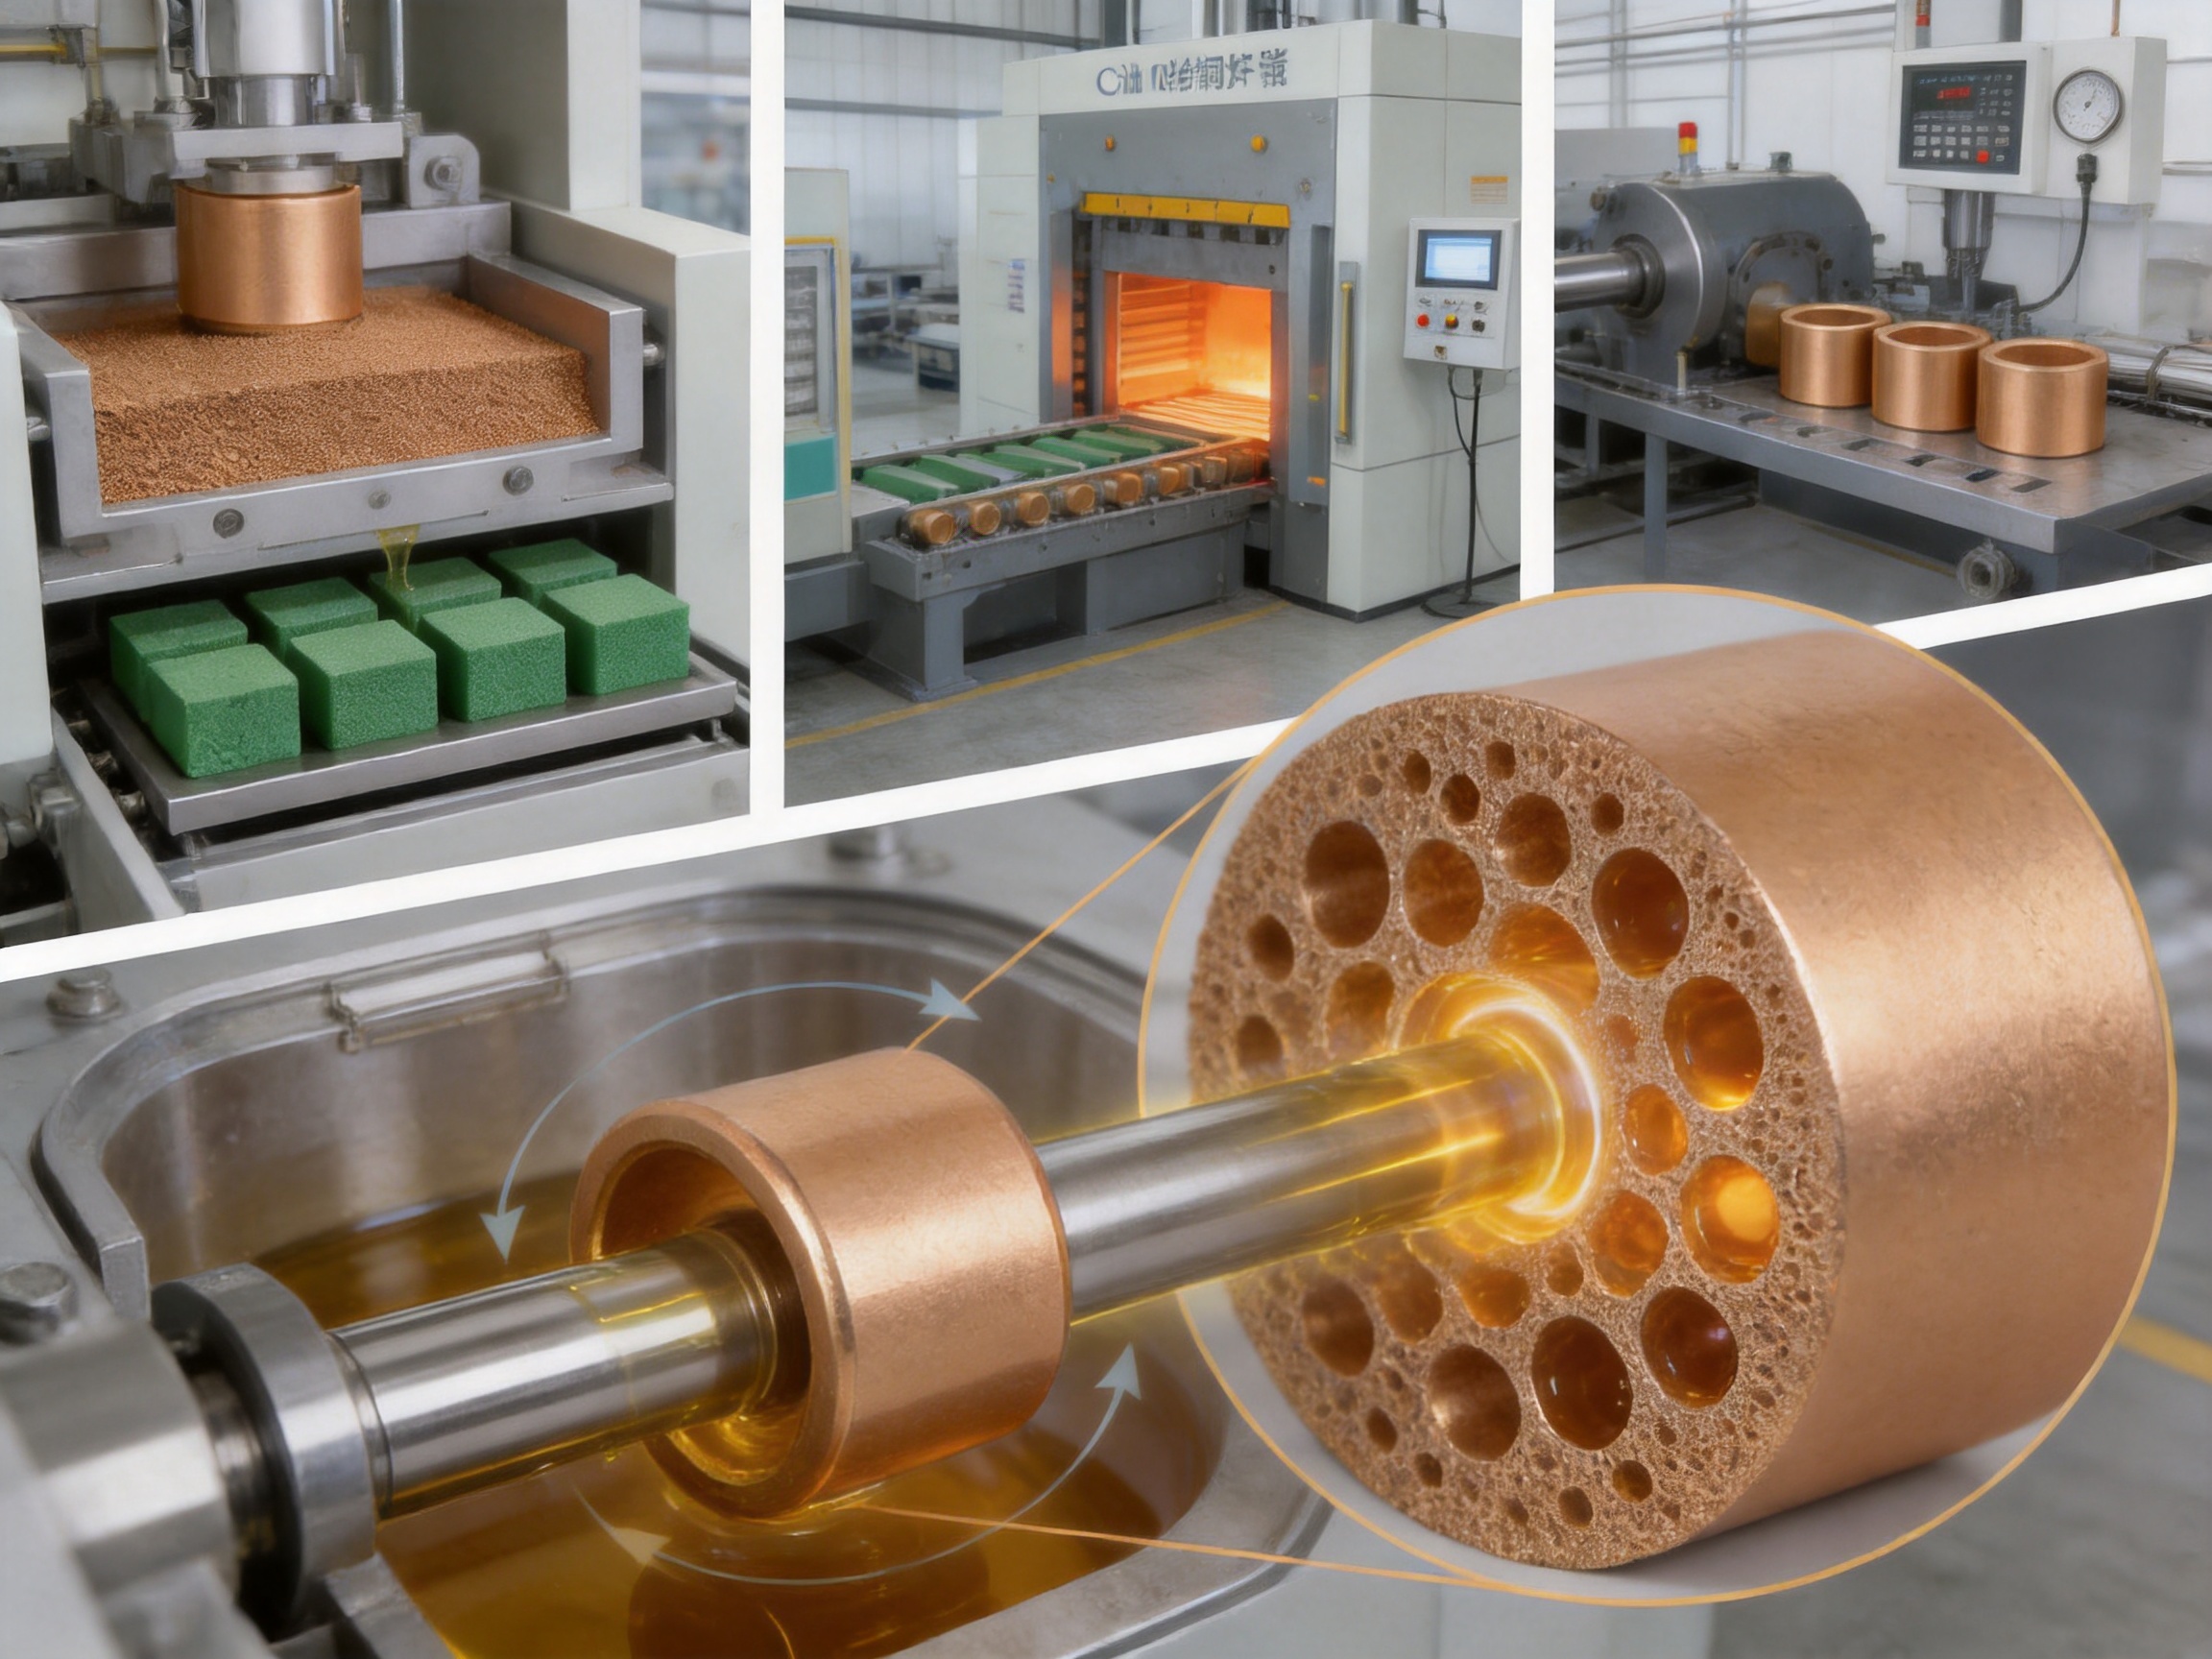
The A0667 product is manufactured using copper-based powder metallurgy technology. The raw powder is compacted under controlled pressure to form the basic geometry. The compacted part is then sintered at a controlled temperature so that the powder particles bond and the required mechanical properties are developed. Sizing and precision processing are used to achieve the specified dimensions, while vacuum oil impregnation introduces lubricating oil into the internal pores.
The final component is designed for applications where compact dimensions, stable lubrication, reliable dimensional control, and reduced servicing requirements are important. Its 0.4 × 45° chamfer helps guide assembly and reduces the possibility of interference when the bushing is inserted into a housing or combined with a shaft.
| Product Item | Specification |
| Product Name | Powder Metallurgy Bronze Bushing |
| Product Code | A0667 |
| Material | CuSn10 copper-tin bronze |
| Nominal Specification | 10G7 × 13s7 × 10 mm |
| Chamfer | 0.4 × 45° |
| Weight | 3.36–3.41 g |
| Density | 5.7–5.8 g/cm³ |
| Concentricity | ≤0.05 mm |
| Sintering Parameter | TCI 690 ± 30°C |
| Lubricating Medium | 46# mechanical oil |
| Oil Impregnation Condition | 80°C vacuum environment |
The product is also suitable for customization. Customers can provide drawings, samples, three-dimensional models, or technical requirements for the development of bushings with different outer diameters, inner diameters, lengths, chamfers, grooves, density levels, materials, and lubrication specifications.
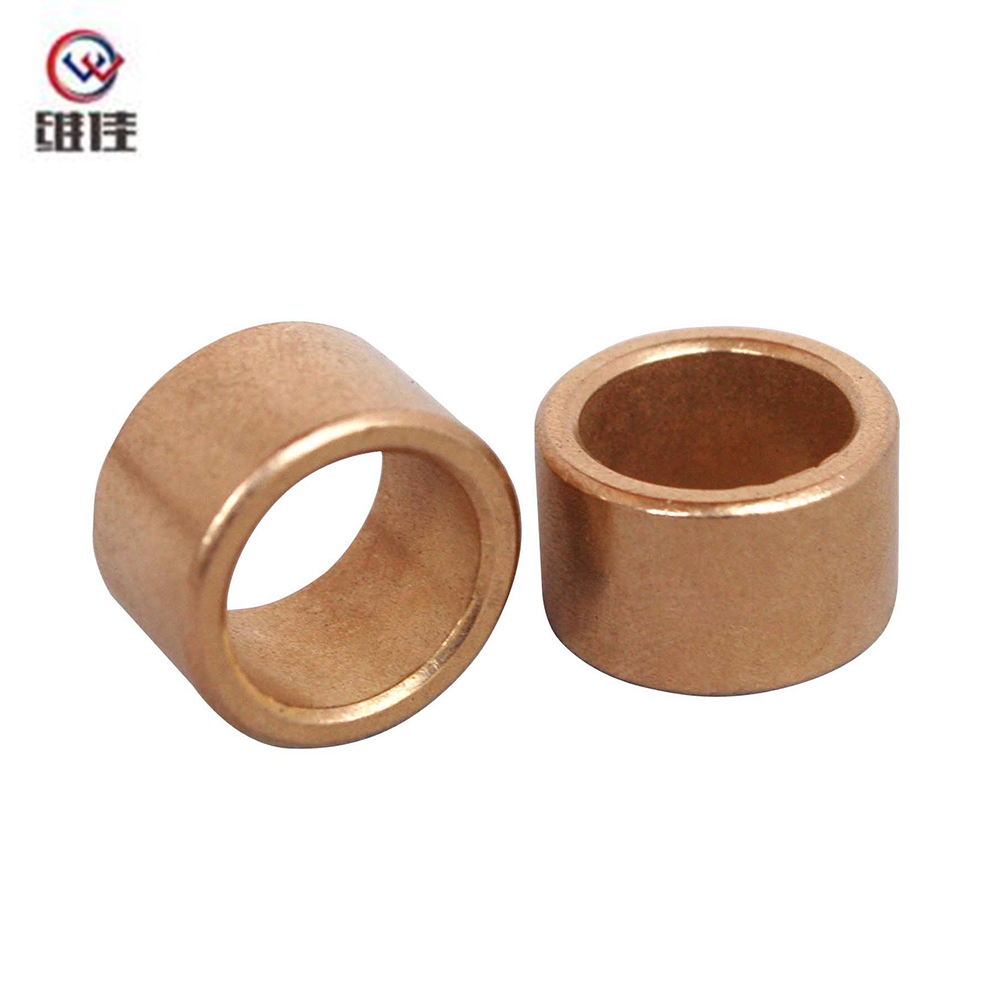
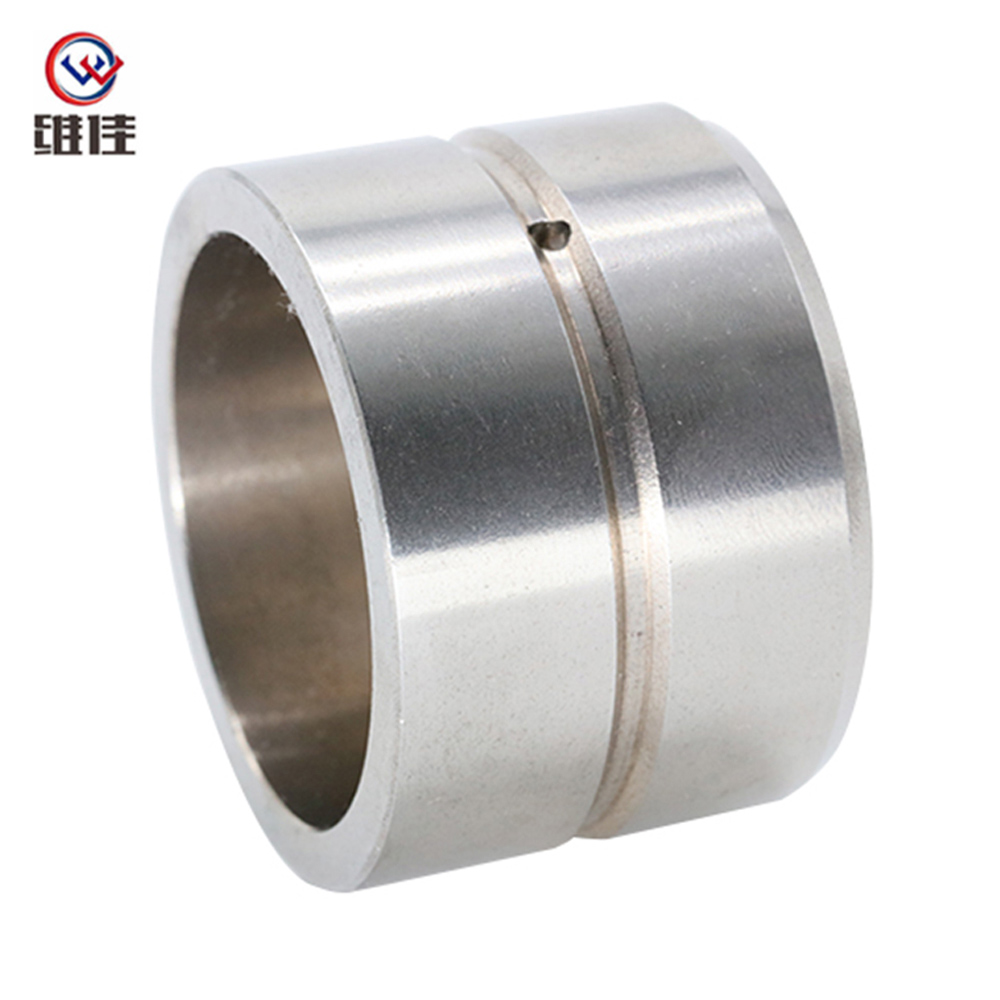
Powder Metallurgy Bronze Bushing (A0667)
2. Why CuSn10 Is Suitable for Powder Metallurgy Bushings
CuSn10 bronze is a copper-based alloy containing approximately 10% tin. The addition of tin improves the hardness, wear resistance, and load-supporting capability of the copper matrix. At the same time, the alloy retains the favorable thermal conductivity and machinability associated with copper-based materials.
When CuSn10 is processed through powder metallurgy, the final material contains a controlled network of pores. These pores are not random defects. They are deliberately established through powder selection, compaction pressure, sintering conditions, and density control. After oil impregnation, the pores act as reservoirs for lubricant.
This combination of alloy composition and porous structure provides several functional advantages:
First, the bronze matrix provides a durable sliding surface. It resists adhesive wear and can perform reliably under repeated relative movement between the bushing and shaft.
Second, the oil-retaining pores provide internal lubrication. This is particularly useful in assemblies where it is difficult to install a grease fitting or where regular manual lubrication would increase maintenance costs.
Third, the material has favorable heat transfer characteristics compared with many nonmetallic bearing materials. Heat generated at the sliding interface can be transferred through the bushing and surrounding metal structure, subject to the design and operating conditions of the complete assembly.
Fourth, the powder metallurgy process permits the manufacturer to establish a balance between strength and oil retention. Excessive porosity may reduce mechanical strength, while insufficient porosity may limit the quantity of lubricant that can be retained. Process control is therefore essential.
2.1 Wear Resistance
Wear resistance is one of the most important requirements for a bushing. During operation, the component may experience continuous rotation, oscillating movement, impact loading, vibration, or frequent starting and stopping. CuSn10 bronze is suitable for these conditions because the tin-containing matrix provides greater hardness and resistance to surface damage than many low-hardness copper materials.
The oil film formed during operation further reduces direct metal-to-metal contact. This limits adhesive wear, lowers friction, and helps prevent scoring of both the bushing and the mating shaft. The actual wear rate depends on load, speed, shaft hardness, surface roughness, alignment, temperature, contamination, and installation quality, but the material and lubrication design provide a strong foundation for long service life.
2.2 Load-Supporting Capability
A bushing must support the shaft without excessive deformation. The CuSn10 bronze matrix offers a useful balance between hardness and toughness. It can carry radial loads in many industrial assemblies while maintaining a stable sliding interface.
Powder metallurgy also helps produce a consistent microstructure. Uniformly distributed particles and controlled sintering reduce local variations that could otherwise create weak points or uneven wear. For applications involving shock loads or severe impact, the bushing design should be evaluated using the actual load spectrum and operating conditions.
2.3 Oil Retention and Self-Lubrication
The central advantage of an oil-impregnated powder metallurgy bushing is its ability to retain and release lubricant. After vacuum impregnation, the pores contain 46# mechanical oil. During operation, the oil is available near the sliding surface and can form a lubricating film.
This arrangement does not mean that the bushing is maintenance-free under every condition. High temperatures, heavy loads, high speeds, contamination, misalignment, and extended operation can consume or degrade the lubricant. Nevertheless, it can significantly reduce the need for frequent external lubrication compared with a conventional dry solid bushing.
3. Advantages Over Conventional Bushing Materials
Different bushing materials are appropriate for different applications. Solid cast bronze, brass, steel-backed composite bearings, plastic bushings, and sintered bronze bushings each have specific strengths. The CuSn10 powder metallurgy bushing is particularly competitive when the application requires integrated lubrication, repeatable dimensions, and efficient mass production.
| Performance Category | CuSn10 Powder Metallurgy Bronze | Conventional Solid Bronze | Standard Brass | General Plastic Bushing |
| Wear Resistance | Excellent | Good to excellent | Moderate | Application dependent |
| Oil Retention | Excellent after impregnation | Low unless externally lubricated | Low | Not applicable in the same way |
| Dimensional Consistency in Mass Production | Excellent | Good but machining dependent | Good but machining dependent | Good when molded correctly |
| Maintenance Requirement | Low in suitable conditions | Regular lubrication may be required | Regular lubrication may be required | Usually low |
| Material Utilization | High | Lower because of machining allowance | Lower because of machining allowance | High during molding |
| Temperature and Load Capability | Strong for many industrial applications | Strong | Moderate | Depends heavily on polymer type |
| Mass Production Efficiency | High | Moderate | Moderate | High |
Compared with traditional cast bronze bushings, the powder metallurgy version can offer more consistent dimensions, improved material utilization, and integrated oil storage. Cast bronze remains valuable for very high loads, large components, or applications requiring fully dense material. However, where reduced maintenance and stable high-volume production are priorities, oil-impregnated powder metallurgy bronze can be more efficient.
Compared with standard brass, CuSn10 generally provides better wear resistance and greater load-supporting capability. Brass may be suitable for decorative, electrical, or lower-load mechanical components, but a bronze bushing is often a more appropriate selection for repeated sliding contact.
Compared with general plastic bushings, the CuSn10 bushing offers a metallic load-bearing structure and favorable heat dissipation. Plastic materials may provide very low noise and good corrosion resistance, but their performance can change significantly with temperature, chemical exposure, moisture absorption, and load. Material selection should therefore be based on the complete operating environment.
4. Precision Design of the A0667 Bushing
Precision is essential because a bushing must fit both the housing and the shaft. If the inner diameter is too small, friction and assembly force may increase. If it is too large, clearance may become excessive and cause vibration, noise, uneven wear, or poor shaft guidance. The outer diameter must also match the housing to prevent movement or loosening during operation.
The A0667 specification of 10G7 × 13s7 × 10 mm defines a compact component with a nominal inner diameter, outer diameter, and length suitable for small precision assemblies. The product information specifies key dimension control within ±0.02 mm and concentricity of no more than 0.05 mm. These controls help maintain alignment between the inner and outer cylindrical surfaces.
The 0.4 × 45° chamfer is a small but important design detail. A chamfer reduces the risk of a sharp edge catching on the housing during pressing. It also helps protect the mating surfaces from damage and makes installation more repeatable. In automated or semi-automated assembly, a consistent chamfer can improve insertion reliability.
Weight control is another useful production indicator. The specified weight range of 3.36–3.41 g helps verify that the component has been manufactured with stable material distribution and consistent geometry. Weight alone cannot confirm performance, but it can support process monitoring when combined with dimensional, density, hardness, and functional inspections.
Density is also carefully controlled. The specified range of 5.7–5.8 g/cm³ reflects the relationship between the CuSn10 material, the designed porosity, and the required mechanical and lubrication properties. A controlled density range supports consistency from batch to batch.
5. Integrated Manufacturing Process
The performance of a powder metallurgy bushing depends on the complete manufacturing chain rather than on material selection alone. The production process for the A0667 component includes raw material inspection, powder preparation, compaction, sintering, sizing, precision machining or finishing where required, cleaning, oil impregnation, inspection, and packaging.
5.1 Raw Material Inspection
Production begins with copper-based alloy powder. Chemical composition and particle size distribution are inspected for each batch. The purpose is to ensure that the powder conforms to the required material and process specification before it enters production.
Particle size affects flowability, filling behavior, compact density, surface quality, and sintering response. Chemical composition affects hardness, wear resistance, corrosion behavior, and the final microstructure. Batch inspection reduces the risk of material variation affecting subsequent operations.
5.2 Powder Preparation and Filling
After inspection, the powder may be blended or prepared according to the required formulation. Consistent mixing helps distribute the alloy constituents uniformly. The prepared powder is then delivered into a forming die.
Accurate die filling is important for small cylindrical parts because uneven filling can produce density gradients. Density variation may lead to dimensional distortion during sintering or inconsistent mechanical properties. Proper tooling design and stable filling conditions help maintain uniformity.
5.3 Compaction
During compaction, the powder is pressed into the approximate shape of the bushing. The compaction force must be sufficient to create a stable green compact while preserving the designed porosity.
Pressing conditions are selected according to the component geometry, powder characteristics, target density, and production rate. The inner hole and outer profile are formed through precision tooling. For high-volume production, tooling condition, press repeatability, and die alignment are closely monitored.
5.4 Sintering
The compacted part is sintered in a controlled atmosphere. For the A0667 product, the listed sintering parameter is TCI 690 ± 30°C. During sintering, the powder particles bond together through diffusion and metallurgical connection. The part develops greater strength and stability while retaining the interconnected pores required for oil impregnation.
Temperature uniformity, heating rate, holding time, atmosphere, and cooling conditions all affect the result. Excessive sintering can reduce porosity and affect oil absorption. Insufficient sintering can result in low strength or poor wear resistance. Careful furnace control is therefore necessary to obtain a consistent balance between strength, density, and oil-retention capability.
5.5 Sizing and Dimensional Correction
After sintering, sizing is used to improve dimensional accuracy and geometric consistency. The part is passed through a sizing tool that applies controlled pressure to correct the inner diameter, outer diameter, roundness, and length as required.
Sizing is particularly valuable for small bushings because even a minor dimensional variation can affect assembly clearance. Stable sizing conditions help achieve the specified tolerance and concentricity without eliminating too much of the designed porosity.
5.6 Precision Machining and Finishing
Depending on the drawing and application, secondary processing may be used to produce chamfers, grooves, special profiles, or tighter dimensions. The goal is to remove only the necessary material while preserving the structural and lubrication characteristics developed during powder metallurgy processing.
For the A0667 bushing, the chamfer and key dimensions are controlled to support reliable installation and operation. Precision processing also improves the surface condition of the sliding bore, helping the bushing work effectively with the specified shaft finish and clearance.
5.7 Cleaning
Before oil impregnation, the workpiece is cleaned to remove powder residue, chips, processing contamination, and loose particles. Cleaning is important because contaminants can block pores, affect oil absorption, or enter the bearing interface during initial operation.
The cleaned component should have a suitable surface condition before entering the impregnation process. The cleaning procedure is controlled to prevent damage to the bushing and to ensure that the subsequent oil treatment is consistent.
6. Vacuum Oil Impregnation
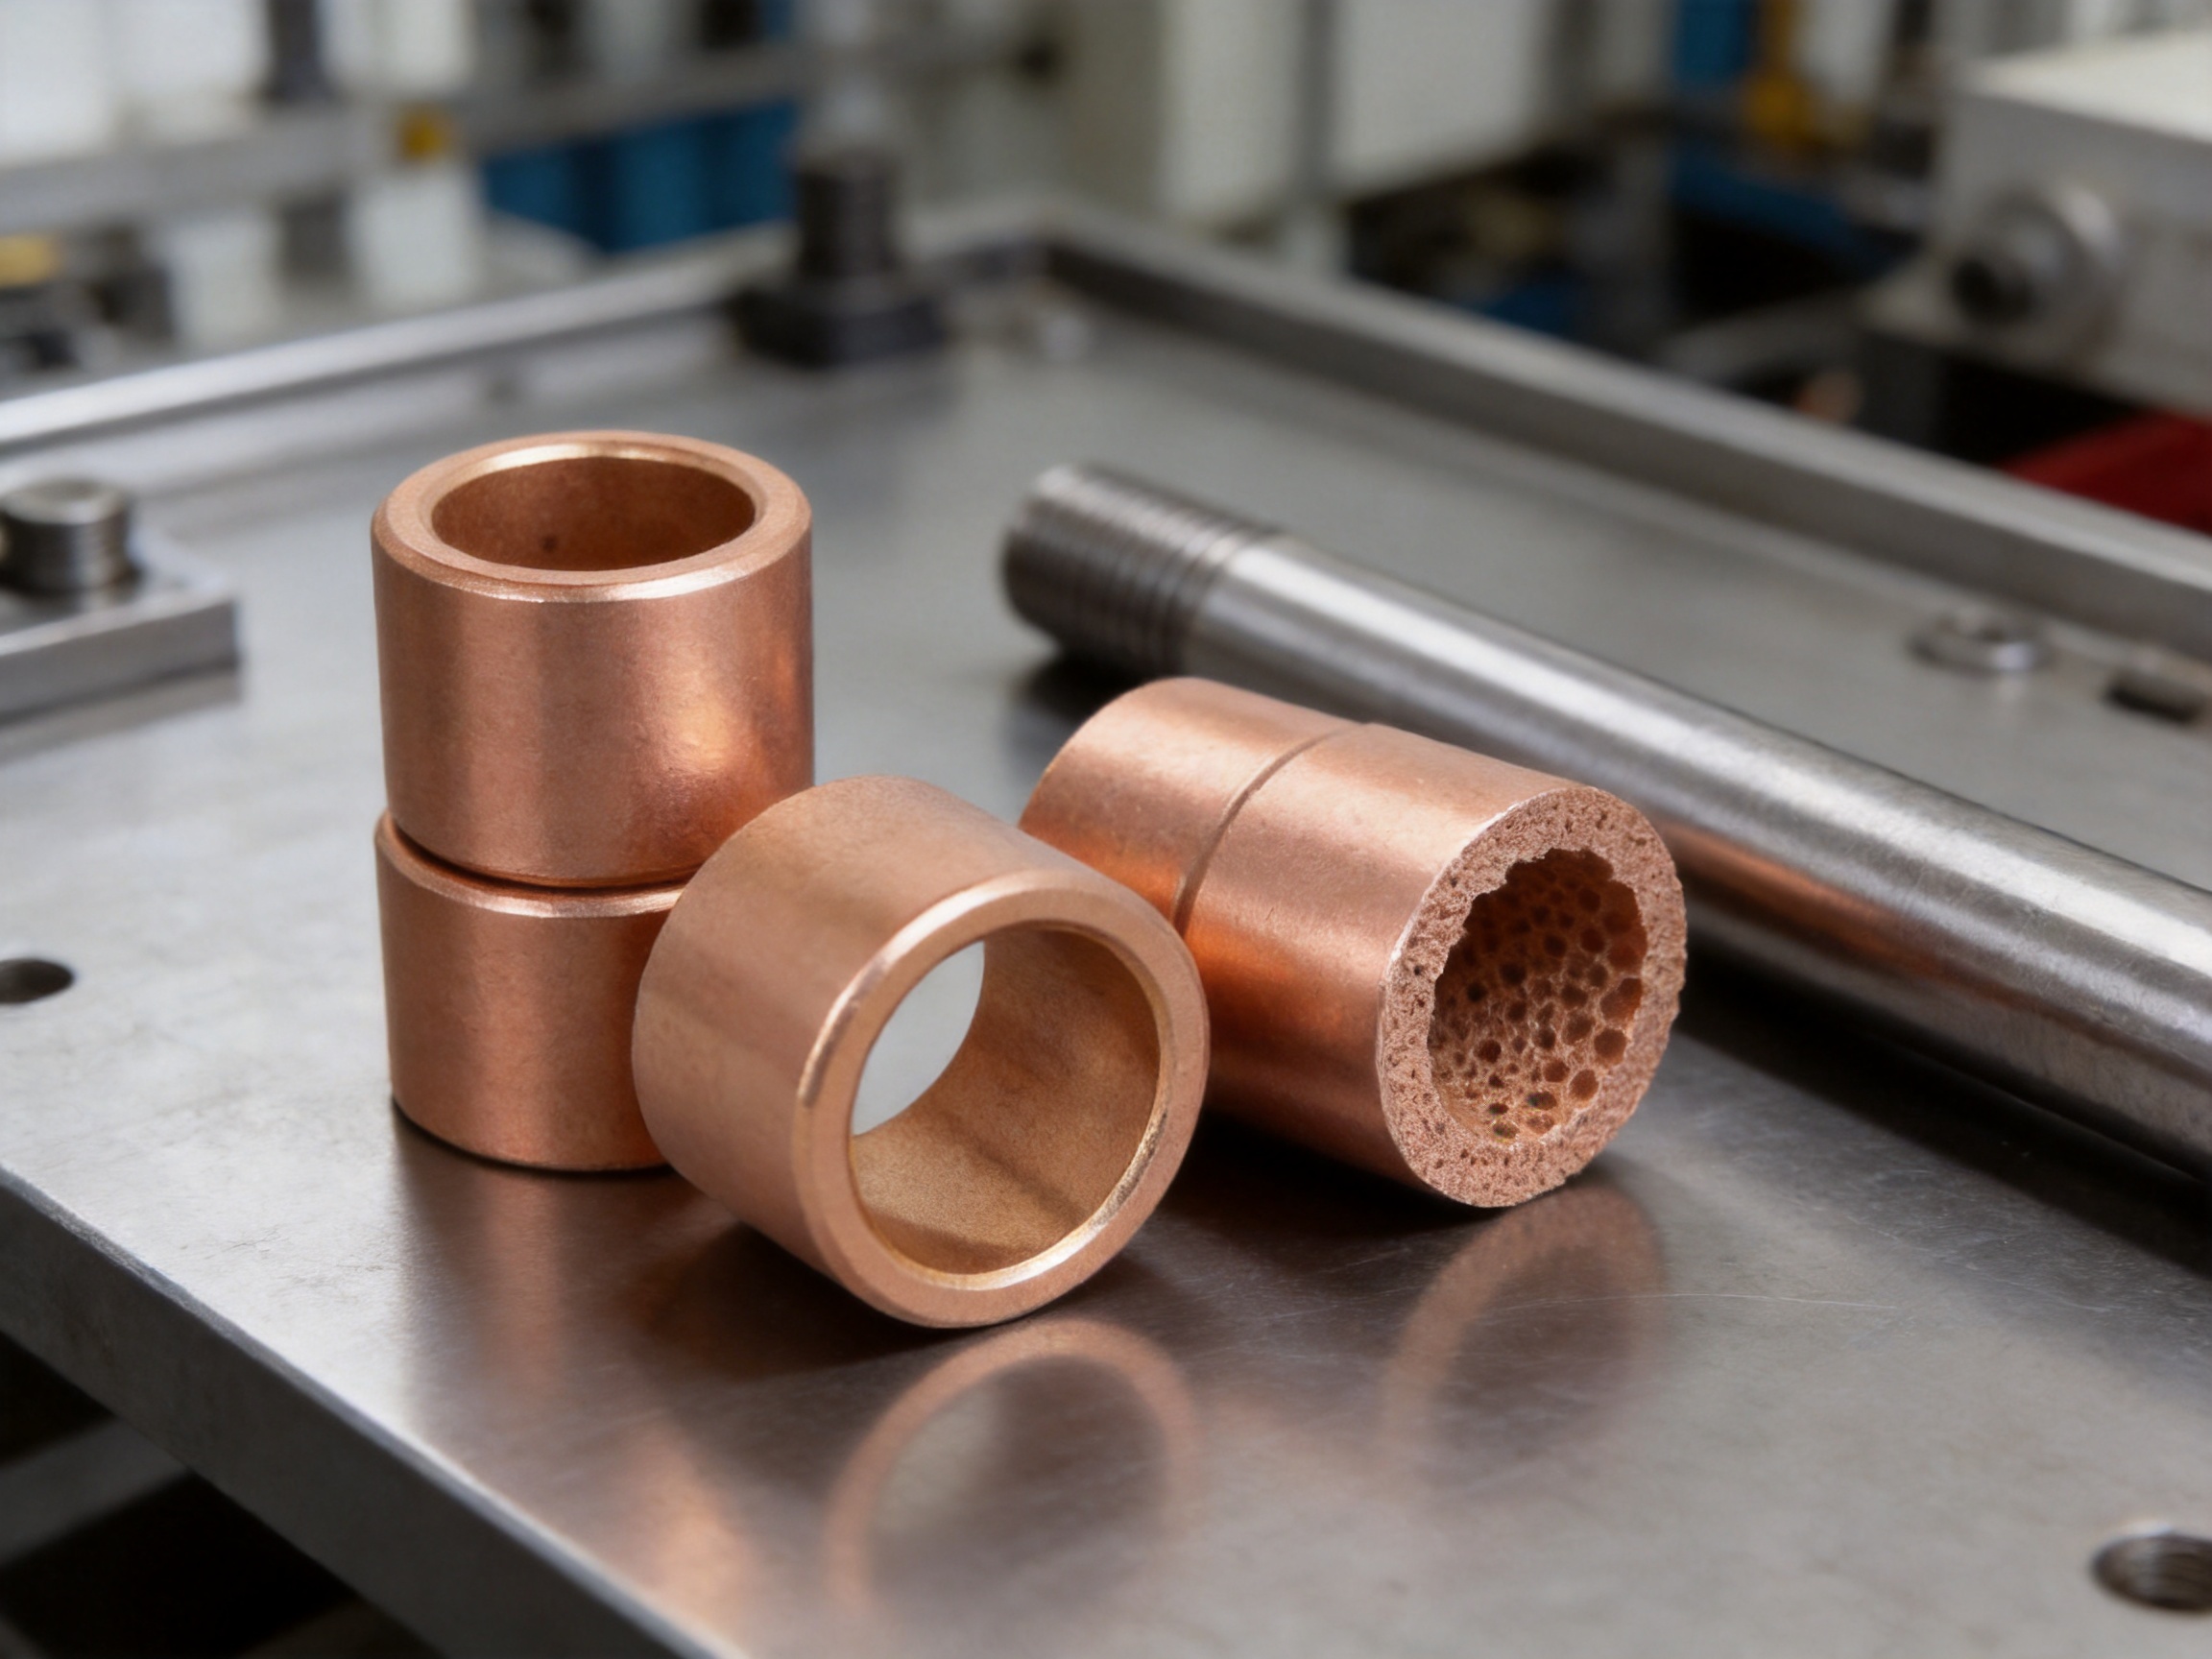
Vacuum oil impregnation is a defining step in the production of the self-lubricating bushing. The porous bushing is immersed in 46# mechanical oil in an 80°C vacuum environment. The vacuum removes air from the interconnected pores. When the vacuum is released while the component remains in oil, the oil is driven into the available pore volume.
This process is more effective than simply applying oil to the surface. Surface application may leave the internal pores largely empty, while vacuum impregnation introduces lubricant throughout the porous structure. The amount of absorbed oil depends on density, pore structure, temperature, vacuum conditions, immersion time, and the characteristics of the oil.
After impregnation, excess surface oil is removed. The product is inspected to ensure that there are no unacceptable oil stains before packing. A clean external surface is important for assembly, handling, and product appearance.
6.1 How the Self-Lubricating Mechanism Works
When the shaft rotates or oscillates inside the bushing, friction generates heat at the sliding interface. The oil within the pores becomes more mobile and gradually reaches the working surface. A thin oil film forms between the shaft and bushing, reducing direct contact and limiting friction.
When the equipment stops, the oil can redistribute within the porous structure. This replenishment effect helps the bushing remain ready for subsequent operating cycles. The result is not unlimited lubrication, but it can provide long intervals of effective operation under properly selected conditions.
The self-lubricating mechanism is especially useful in assemblies where external lubrication is difficult, such as compact mechanisms, enclosed transmission systems, small motors, household appliances, and components with limited service access.
6.2 Conditions That Affect Lubrication Performance
Operating load and speed have a direct influence on oil release. Higher pressure and sliding speed can increase temperature and lubricant consumption. Temperature also affects oil viscosity and migration behavior. Contamination can damage the oil film and accelerate wear.
Installation clearance must be correct. Excessively tight clearance can restrict oil movement and increase friction, while excessive clearance can reduce load distribution and allow vibration. Shaft surface roughness, hardness, alignment, and roundness should be compatible with the bushing.
For severe operating conditions, additional testing should be completed before mass production. Testing may include friction and wear evaluation, load-speed testing, temperature monitoring, oil-loss assessment, dimensional stability analysis, and endurance testing.
7. Quality Control and Manufacturing Strengths
Jiande Welfine Technology Co., Ltd. integrates research and development, production, precision processing, quality control, and sales. Established in 2001, the company focuses on powder metallurgy bushings, self-lubricating bearings, and precision sintered components for industrial customers.
The company operates a modern production base covering approximately 13,039 square meters. Its equipment includes high-efficiency presses, high-temperature sintering furnaces, precision forming machines, and inspection equipment. This combination supports both standard product manufacturing and customized OEM or ODM projects.
More than 20 years of experience in powder metallurgy production provide a foundation for controlling material behavior, tooling, sintering, sizing, oil impregnation, and final inspection. The company also employs more than 150 skilled personnel and supports production based on customer drawings or physical samples.
7.1 Incoming Material Control
Each batch of copper-based powder is checked for composition and particle size. This step helps verify that the material conforms to the required specification and is suitable for stable compaction and sintering.
Incoming material control is particularly important for oil-impregnated bushings because the final density and pore structure are influenced by the powder. Variations in powder characteristics can affect both mechanical strength and oil storage.
7.2 In-Process Inspection
First-article inspection is carried out during production to verify tooling, dimensions, weight, appearance, and process conditions. Online dimension monitoring is used in compaction, sintering, and sizing operations to identify deviations before they affect large quantities of parts.
Monitoring the process rather than relying only on final inspection improves production stability. It can help identify tooling wear, press variation, furnace temperature changes, sizing abnormalities, or other causes of dimensional drift.
7.3 Finished Product Inspection
Finished bushings are subject to full dimensional inspection according to the product requirements. Sampling tests may be performed for density, hardness, wear resistance, appearance, oil impregnation, and other characteristics.
For the A0667 product, important inspection points include the 10G7 × 13s7 × 10 mm dimensions, the 0.4 × 45° chamfer, the 3.36–3.41 g weight range, the 5.7–5.8 g/cm³ density range, and the maximum concentricity of 0.05 mm.
7.4 Management System Certification
The company has obtained ISO 9001:2015 and IATF 16949:2016 certifications. ISO 9001 supports systematic quality management, process control, customer requirement management, and continual improvement. IATF 16949 is especially relevant to automotive-related supply chains because it emphasizes risk control, traceability, defect prevention, and consistent production performance.
Certification does not replace product-specific testing, but it demonstrates that manufacturing activities are organized within documented quality processes. For customers purchasing customized bushings, this can provide additional confidence in production consistency and supplier management.
8. Applications of CuSn10 Powder Metallurgy Bushings
8.1 Automotive Components
Automotive equipment contains many compact sliding and pivoting assemblies. Bushings may be used in actuators, transmission-related mechanisms, chassis components, seat mechanisms, door systems, motors, pumps, and control assemblies.
The compact size and low maintenance characteristics of an oil-impregnated bronze bushing are useful where access for routine lubrication is limited. Automotive applications also benefit from repeatable dimensional control and stable mass production.
8.2 Precision Machinery
Precision machine tools and industrial mechanisms require controlled movement and accurate shaft guidance. A bushing with stable concentricity and controlled clearance can help reduce vibration and maintain predictable motion.
CuSn10 bronze is suitable for moderate loads and repeated sliding movement in compact assemblies. The correct design must account for shaft material, speed, load, operating temperature, and contamination control.
8.3 Hydraulic Pumps and Valve Groups
Hydraulic systems contain moving components that require reliable guidance under pressure and repeated cycling. Bushings may be used in pump components, valve groups, linkages, and actuator mechanisms.
Dimensional accuracy is important because excessive clearance can contribute to movement or leakage-related problems, while insufficient clearance can increase friction. The selection of a sintered bronze bushing should be based on the specific hydraulic medium, temperature, pressure, speed, and compatibility requirements.
8.4 Fans and Refrigerators
Fans and refrigeration equipment often use small rotating shafts and compact motor assemblies. In these applications, low friction, low maintenance, and stable operation are important. An oil-impregnated bushing can provide internal lubrication without requiring a complex external lubrication system.
Consistent dimensions and controlled surface quality help support quiet and stable rotation. Product selection should consider motor speed, temperature, shaft alignment, starting frequency, and expected service life.
8.5 Household Appliances
Washing machines, small motors, kitchen appliances, power mechanisms, and other household products may use bushings in transmission structures and moving parts. The high-volume nature of appliance manufacturing makes material efficiency and repeatable production especially valuable.
Powder metallurgy allows near-net-shape production with limited secondary machining. This can reduce material waste and support competitive unit costs when production volumes are high.
8.6 Agricultural and Construction Machinery
Agricultural and construction equipment often operates under vibration, dust, changing loads, and frequent start-stop cycles. CuSn10 bushings can provide a durable sliding interface for selected joints and transmission components.
Environmental contamination remains an important consideration. Seals, protective structures, shaft design, and maintenance practices should be used where necessary. In highly contaminated or shock-loaded conditions, the bushing must be validated through application-specific testing.
8.7 Automation Equipment
Automated production equipment requires repeatable motion and predictable service intervals. Bushings may be installed in guide mechanisms, linkages, linear movement assemblies, and rotating joints.
The dimensional consistency of powder metallurgy components can support standardized machine design. Customized forms, grooves, profiles, and material options can also be developed for special automation requirements.
9. Comparison with Other Sintered and Self-Lubricating Bearings
Not all sintered bushings use the same material or pore structure. Iron-based bushings may provide high strength and cost advantages, while bronze-based bushings generally offer favorable corrosion resistance, thermal conductivity, and sliding behavior. The appropriate material depends on the load, speed, environment, and lubrication requirements.
CuSn10 is particularly suitable where wear resistance, oil retention, and dimensional stability must be combined in a compact component. Compared with a basic iron-based sintered bushing, copper-tin bronze may provide more favorable corrosion resistance and heat transfer in selected environments. Compared with a fully dense machined bronze component, the porous version can reduce maintenance by storing lubricant internally.
| Selection Factor | Recommended Consideration for CuSn10 Bushing |
| Load | Verify radial and impact loads against the bushing design |
| Speed | Evaluate sliding speed and heat generation |
| Lubrication | Use the specified oil impregnation system or confirm compatibility with the application |
| Temperature | Check oil viscosity, material stability, and operating temperature range |
| Shaft Surface | Use suitable hardness, roundness, alignment, and surface roughness |
| Housing Fit | Control housing dimensions and installation method |
| Contamination | Use seals or protective features where dust, water, or particles are present |
| Maintenance | Establish inspection intervals based on actual working conditions |
10. Installation and Service Recommendations
Correct installation is essential for achieving the expected performance of an oil-impregnated bronze bushing. Before assembly, inspect the housing bore and shaft for burrs, contamination, damage, and dimensional deviations. The shaft should be correctly aligned and should not have sharp edges that could damage the internal surface.
The housing bore should provide the specified interference or fit condition. Excessive pressing force can deform the bushing or reduce the internal clearance. If a press is used, the force should be applied evenly and through a suitable installation tool. Pressing directly on an unsupported edge can distort the component.
After installation, check the shaft rotation or oscillation manually when possible. The movement should be smooth and free from abnormal binding. For automated equipment, initial running tests should monitor noise, temperature, friction, vibration, and movement accuracy.
Additional grease or oil should not be added without confirming compatibility. An incompatible lubricant may alter viscosity, damage the impregnated oil, contaminate the pores, or interfere with the intended lubrication behavior. If external lubrication is required for a special application, the lubricant type and quantity should be confirmed with the technical supplier.
Periodic inspection is recommended even though the bushing is self-lubricating. Inspection intervals should be based on load, speed, temperature, operating hours, contamination, and the consequences of failure. In demanding applications, maintenance personnel should monitor shaft play, temperature rise, noise, vibration, and visible wear.
11. Custom Manufacturing Capabilities
Industrial customers often require bushings that differ from standard catalog dimensions. Jiande Welfine Technology Co., Ltd. provides customized powder metallurgy structural parts and bushing solutions based on customer drawings, samples, or technical specifications.
Customization may include:
Inner and outer diameter changes for different shaft and housing fits.
Different lengths for compact or extended bearing support.
Chamfers, steps, grooves, flanges, lubrication channels, and other geometric features.
Alternative copper-based materials or other powder metallurgy formulations.
Modified density and porosity levels for different load and lubrication requirements.
Special oil impregnation requirements for specific operating temperatures or environments.
Small-batch prototypes for design verification.
Mass production for automotive, appliance, machinery, hydraulic, and automation customers.
The development process generally begins with a technical review of the drawing or sample. Engineers evaluate the geometry, material, tolerances, tooling requirements, production volume, lubrication method, and inspection plan. A prototype or first article can then be produced for dimensional and functional validation before full-scale production.
This approach helps customers improve manufacturability before committing to large quantities. It also allows the production process to be adjusted for special requirements such as tight concentricity, controlled weight, unusual profiles, or specific assembly conditions.
12. Ordering, Delivery, and Technical Support
Customers can provide product drawings or samples to request a quotation. According to the supplied service information, a precise quotation can normally be prepared within 24 hours after the technical requirements are received and reviewed.
Standard orders are generally delivered within 7–15 working days, while urgent orders may be supported through priority production arrangements. Actual delivery depends on product complexity, tooling requirements, order quantity, inspection requirements, and shipping method.
International logistics support includes express services such as DHL or FedEx, as well as sea and air freight. Packaging is prepared after cleaning and oil treatment to help protect the product during transportation and prevent contamination.
After-sales support includes technical installation guidance and product replacement for confirmed dimensional or material mismatches. For customized parts, customers should provide complete technical information and approval samples so that the final inspection criteria are clearly established before production.
13. Why This Product Is a Competitive Choice
The A0667 CuSn10 powder metallurgy bronze bushing combines several characteristics that are difficult to achieve through a single conventional process. Its copper-tin alloy provides a durable metallic sliding matrix. Its controlled porosity provides internal oil storage. Its sizing and inspection processes support precision installation. Its compact geometry enables use in small mechanical assemblies. Its production method supports material efficiency and repeatable high-volume manufacturing.
Compared with a basic machined bushing, the product can reduce material waste and integrate lubrication into the component. Compared with a standard non-impregnated bronze bushing, it can reduce dependence on frequent external lubrication. Compared with ordinary brass, it offers a stronger combination of wear resistance and load support for sliding applications.
The product is also supported by an established manufacturing organization with a modern production base, experienced personnel, quality certifications, advanced production equipment, and OEM and ODM capabilities. These strengths are important for customers who need more than a one-time component purchase and require stable long-term supply.
Its advantages can be summarized as follows:
Controlled CuSn10 bronze composition for wear-resistant sliding performance.
Oil-retaining porous structure for self-lubricating operation.
High material utilization and efficient powder metallurgy production.
Controlled dimensions and concentricity for precision assembly.
Vacuum oil impregnation using 46# mechanical oil at 80°C.
Suitable performance for automotive, hydraulic, appliance, machinery, fan, refrigerator, and automation applications.
Customization based on customer drawings, samples, and technical requirements.
Quality control covering raw materials, process conditions, dimensions, density, hardness, and wear performance.
Support for prototypes, small batches, mass production, international delivery, and technical installation guidance.
14. Future Development of Powder Metallurgy Bronze Bushings
Industrial equipment is moving toward higher efficiency, more compact designs, longer service intervals, and increased automation. These trends are encouraging manufacturers to use components that can operate reliably with reduced maintenance.
Self-lubricating powder metallurgy bushings are well suited to this development. Their integrated lubrication capability can simplify mechanical design and reduce the need for grease fittings, oil channels, and frequent servicing. Their near-net-shape manufacturing capability also supports cost-effective production of repeatable components.
Future development may focus on improved pore-structure control, advanced alloy formulations, optimized lubricating oils, higher precision tooling, digital process monitoring, and application-specific surface treatments. New energy vehicles, electric tools, robotics, automated production lines, and compact electromechanical systems may create additional demand for small, durable, and low-maintenance bushings.
At the same time, product selection must remain application-specific. A bushing should not be selected solely by material name or price. Engineers should evaluate the full operating envelope, including load, speed, temperature, clearance, shaft condition, contamination, duty cycle, and maintenance expectations.
15. Frequently Asked Questions
Can the CuSn10 powder metallurgy bushing operate without regular lubrication?
Under suitable operating conditions, the oil-impregnated porous structure can provide continuous or intermittent lubrication and significantly reduce the need for external lubrication. It should not be considered completely maintenance-free in every application. Periodic inspection remains recommended, especially under high load, high speed, high temperature, or contaminated conditions.
What is the main advantage of CuSn10 over standard brass?
CuSn10 generally provides better wear resistance and load-supporting capability for sliding applications. When processed through powder metallurgy and impregnated with oil, it also provides an oil-retaining structure that standard brass does not normally possess.
How does vacuum oil impregnation improve performance?
Vacuum oil impregnation removes air from the internal pores and allows 46# mechanical oil to penetrate the porous structure. During operation, the oil can migrate toward the sliding surface and help form a lubricating film. This supports lower friction and reduced wear.
What does the density range of 5.7–5.8 g/cm³ indicate?
The density range indicates that the bushing has been produced within a controlled relationship between bronze material content and porosity. Density affects strength, oil absorption, wear behavior, and dimensional stability. Maintaining a narrow range helps improve batch-to-batch consistency.
Why is concentricity important for a bushing?
Concentricity describes the alignment between the inner and outer cylindrical surfaces. Good concentricity helps maintain even wall thickness, uniform load distribution, stable shaft guidance, and predictable clearance. The A0667 product specifies concentricity of no more than 0.05 mm.
What is the purpose of the 0.4 × 45° chamfer?
The chamfer guides the bushing into the housing during assembly and reduces the risk of edge interference or damage. It is especially useful in press-fit and automated assembly operations.
Is this bushing suitable for high-speed equipment?
It can be suitable for many medium- and high-speed applications, but the actual limit depends on load, shaft diameter, clearance, temperature, oil behavior, alignment, and duty cycle. Application-specific testing is recommended before use in high-speed or critical equipment.
Can the product be customized?
Yes. Customized dimensions, profiles, materials, density levels, chamfers, grooves, and lubrication requirements can be evaluated according to customer drawings, samples, or technical specifications. Prototype production and mass production are both supported.
What information should be provided when requesting a quotation?
Useful information includes a drawing or sample, material requirement, inner and outer dimensions, length, tolerances, chamfers or grooves, operating load, speed, temperature, shaft material, housing material, lubrication conditions, annual quantity, and inspection requirements.
How should the bushing be installed?
The housing and shaft should be clean, aligned, and free from burrs. Use a suitable press or installation tool and apply force evenly. Avoid striking the bushing directly or applying force to an unsupported edge. After installation, check for smooth shaft movement and abnormal friction or binding.
What quality certifications support production capability?
The manufacturing company operates with ISO 9001:2015 and IATF 16949:2016 certifications. These systems support documented quality management, process control, defect prevention, traceability, and continuous improvement.
What industries commonly use this type of bushing?
Typical industries include automotive manufacturing, precision machinery, hydraulic equipment, fans, refrigerators, household appliances, agricultural machinery, construction machinery, electric motors, and automated production equipment.
Conclusion
The CuSn10 powder metallurgy bronze bushing is a practical solution for mechanical assemblies that require wear resistance, controlled dimensions, integrated lubrication, and reduced maintenance. The A0667 model demonstrates how copper-tin material, controlled porosity, precision forming, sintering, sizing, chamfering, and vacuum oil impregnation can be combined into a compact and reliable bearing component.
Its principal competitive advantage is the balance between a durable bronze matrix and an oil-retaining porous structure. This allows the component to support sliding movement while reducing direct metal contact and external lubrication requirements. Compared with ordinary brass, it offers improved suitability for wear-related applications. Compared with conventional solid bronze, it can provide oil storage, material efficiency, and consistent mass production.
Manufacturing quality is equally important. Raw material inspection, controlled compaction, sintering at 690 ± 30°C, sizing, dimensional monitoring, cleaning, vacuum impregnation at 80°C, and final inspection all contribute to the performance of the finished product. Supported by an experienced production team, a 13,039-square-meter facility, advanced equipment, ISO 9001:2015 and IATF 16949:2016 certifications, and OEM and ODM capabilities, Jiande Welfine Technology Co., Ltd. can provide customized solutions for a wide range of industrial requirements.
For engineers and purchasing teams, the best results will come from evaluating the bushing together with the shaft, housing, load, speed, temperature, clearance, contamination, and duty cycle. When properly specified and installed, the CuSn10 powder metallurgy bronze bushing can contribute to longer service life, lower maintenance frequency, stable mechanical performance, and more efficient equipment design.
References
1. ISO 9001:2015, Quality Management Systems — Requirements.
2. IATF 16949:2016, Quality Management System Requirements for Automotive Production and Relevant Service Parts Organizations.
3. Powder Metallurgy Materials and Processes, general technical principles for compaction, sintering, sizing, and porous component manufacture.
4. Copper and Copper Alloy Engineering Data, material characteristics of copper-tin bronze and related bearing alloys.
5. Technical information supplied for the CuSn10 Powder Metallurgy Bronze Bushing, Product Code A0667.
6. Technical information supplied for vacuum oil impregnation using 46# mechanical oil under controlled temperature and vacuum conditions.
7. General engineering guidance for plain bearings, sliding interfaces, shaft and housing fits, lubrication, installation, and maintenance.
Product: Powder Metallurgy Bronze Bushing (A0667)
Related products
-
-
Product Description: High-precision powder metallurgy part (S14*7*10) made of iron material from Jiande Wefine, customized PM components with strict tolerance control.
See Details -
This copper-based powder metallurgy bushing is manufactured through an integrated process of compaction, sintering, sizing, and oil impregnation. It features excellent wear resistance and self-lubrica...
See Details
Copyright © Jiande Welfine Technology Co., Ltd. All Rights Reserved. Privacy Custom Self-lubricating Sintered Bushing Manufacturers
